

What factors should be considered in selecting the right application method for clear and black powder coatings on metal components?
Selecting the right application method for clear or black powder coating depends on the metal substrate, component size and geometry, production volume, required appearance, and the part’s service environment. The coating process should also provide suitable surface preparation, even powder coverage, and controlled curing so the chosen finish bonds consistently without obscuring detail or causing defects.
The right application method for clear or black powder coating is determined by how the powder can be deposited, controlled and cured on the specific component. In practice, the main choice is usually between electrostatic spray and fluidised-bed application, with the decision influenced by coating thickness, part design, production handling, masking requirements, powder characteristics and the level of finish control required.
Electrostatic spray application is generally suited to components requiring controlled coverage, defined edges or a relatively consistent film build. The powder is electrically charged and attracted to an earthed metal part, allowing an operator or automated system to direct material onto the required surfaces. This method can be advantageous for components with mixed surface profiles, apertures or areas that need selective coating, although recessed sections and internal corners may require careful gun positioning because of the Faraday cage effect.
The shape of the component should therefore be assessed in three dimensions rather than by its overall size alone. Deep recesses, narrow channels, folded returns and enclosed sections can affect how powder travels and accumulates. The application method may need to incorporate changes in gun angle, spray sequence, part rotation or equipment settings. Where certain faces must remain uncoated, the design of masks, plugs and hanging points is also important, particularly for mating faces, threaded holes, earth points and close-tolerance interfaces.
Fluidised-bed application can be considered where a heavier, more enveloping coating is appropriate and the component can be heated before being immersed in a cloud of fluidised powder. It is often more suitable for parts that can tolerate the required heat and do not depend on a very thin or tightly controlled decorative layer. The method is less flexible where only selected areas are to be coated, where sharp dimensional limits apply, or where the component’s geometry could trap excess powder.
Required film build and dimensional tolerance are practical selection criteria. A thick coating may improve coverage and provide a substantial protective layer, but it can affect the fit of assemblies, the operation of moving parts and the engagement of threads or press-fit sections. A clear finish may also make uneven build more noticeable through variations in gloss or surface reflection. The application route should be selected alongside acceptable coating tolerances, not treated as a separate finishing decision.
Powder formulation and charging behaviour also affect method selection. Different powders can behave differently during electrostatic application, particularly on complex profiles or when a smooth, uniform layer is required. The suitability of corona charging, tribo charging or another spray arrangement depends on the powder, equipment and component. Black powder can also create practical production considerations where equipment is shared between colours, as residual material in hoses, guns or recovery systems may cause contamination. Clear powder is especially sensitive to visible contamination because particles or colour carry-over can show through the finished layer.
Temperature exposure and component construction must be reviewed before choosing a method. The metal itself may withstand the process, while attached seals, bearings, magnets, electronics, adhesives or other non-metallic elements may not. Fabricated assemblies should be assessed for distortion, trapped contaminants and areas that could retain powder or moisture. If a component cannot safely undergo the necessary heating or must remain assembled, the viable application options may be narrower.
Masking and rack design influence both finish quality and repeatability. Components need secure electrical contact for electrostatic spray, but the contact point will normally remain uncoated and must be located where it can be tolerated or subsequently treated. Racks should minimise contact marks, prevent parts from touching during application and allow adequate access to all required faces. For batch work, a consistent hanging arrangement helps maintain the same spray distance and orientation from one part to the next.
Clear coatings require particularly strict process control. Unlike an opaque black finish, a clear layer does not hide the underlying colour, texture or visual variation of the metal and pre-treatment system. The selected method should therefore minimise dust inclusion, uneven deposition, overspray and handling marks. It is sensible to confirm how the clear powder will affect the existing surface appearance before full production, especially where the component has a brushed, blasted or otherwise directional finish.
Black coatings still require controlled application. Their opacity can reduce the visibility of some substrate variation, but it does not remove the risk of orange peel, pinholes, thin edges, contamination or inconsistent gloss. A method that produces excessive build on corners or insufficient coverage in recesses can lead to a visibly uneven result and may compromise protection at vulnerable points.
Production requirements should be considered alongside the individual part. For repeat batches, the preferred method should support consistent loading, predictable powder consumption, manageable colour changes and straightforward inspection. For mixed component sizes or low-volume specialist work, a flexible spray process may be more practical than a method designed around a dedicated immersion arrangement. Any recovery system should also be assessed for the required colour and finish, since reclaimed powder can influence consistency if it is not properly controlled.
A sound selection process therefore compares the component drawing, coating specification, powder data, masking plan, hanging arrangement and curing limitations before production begins. Trial application on representative parts can identify problems with recess coverage, contact marks, edge build, clear-finish transparency or dimensional fit. For manufacturers and fabricators, this technical review helps match the application method to the component rather than choosing a process solely because it is suitable for black or clear powder in general.
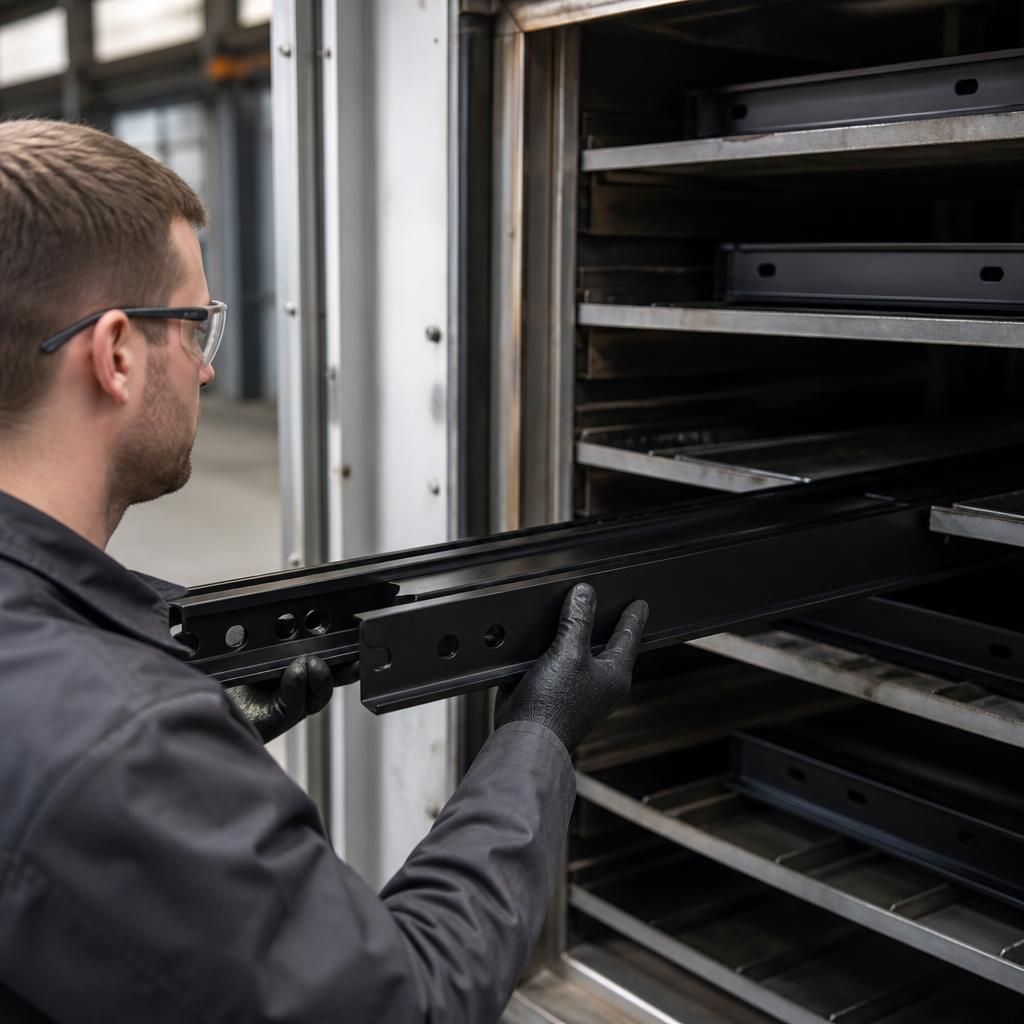
Curing capability should be assessed alongside the powder deposition method. The part must reach the coating manufacturer’s specified metal temperature for the required time; the oven air temperature alone does not confirm that the coating has cured correctly. Component thickness, load density and the way parts are positioned can all affect heat transfer, so a method that works for a light component may not produce the same result on a heavier fabricated assembly.
Incorrect curing can affect adhesion, hardness, gloss and chemical resistance. Under-cured powder may remain vulnerable in service, while excessive heat exposure can alter the appearance of a clear finish or affect heat-sensitive parts. Before selecting the application route, confirm that the available curing equipment can accommodate the component dimensions and maintain a repeatable temperature profile. A representative trial, with the part temperature checked rather than relying only on the oven display, helps establish whether the proposed process is suitable for both clear and black finishes.
Discuss the right application method for your components
Discuss your component drawings, coating specification and application requirements with Powder-coatings.co.uk to assess the most suitable method for a clear or black powder-coated finish. Representative parts can help clarify masking, coverage and dimensional considerations before production.