

What factors should be considered when selecting a stainless steel black coating supplier to ensure quality and reliability?
Select a stainless steel black coating supplier by assessing their experience with stainless steel, control of surface preparation and curing, ability to maintain consistent colour and film coverage, and approach to inspection and traceability. Reliability also depends on clear specifications, suitable handling of components, batch capacity and dependable collection and delivery across the Midlands.
A reliable stainless steel black coating supplier should be assessed against the complete coating specification, not simply the appearance of a sample. Quality depends on whether the supplier can match the coating system to the stainless steel grade, component design, service environment and required finish, while reliability depends on controlled processes, documented checks, clear communication and the ability to manage non-conforming work.
Confirm the required performance before comparing suppliers. The supplier should understand where the coated parts will be used and what they will be exposed to. Indoor architectural components, external fabrications, automotive parts and equipment used in damp or chemically aggressive environments may require different coating specifications. Discuss exposure to moisture, salt, cleaning chemicals, abrasion, heat and ultraviolet light. A supplier who asks about these conditions is better placed to recommend a suitable black coating rather than treating every component in the same way.
It is also important to define what “black” means for the project. Establish the required gloss level, texture, visual uniformity and acceptable variation between components or production batches. If the parts will be installed alongside existing black metalwork, provide a reference sample or an agreed colour standard. This reduces the risk of disagreement caused by different interpretations of matt, satin, textured or high-gloss finishes.
Check the supplier’s understanding of stainless steel as a substrate. Stainless steel can present particular coating challenges because its surface condition, alloy, fabrication history and contamination levels influence adhesion. Welded areas, laser-cut edges, polishing compounds, handling marks and embedded iron particles may all need consideration. Ask how the supplier identifies these risks and how unusual geometries, recesses, folded sections and exposed welds are assessed before coating.
The coating system should also be compatible with the intended use of the component. Ask which pre-treatment and powder type are proposed, why they are suitable for stainless steel, and whether the recommendation changes for indoor and outdoor service. A technically credible supplier should be able to explain the reasoning in practical terms rather than relying only on a generic product description.
Review the evidence behind the supplier’s quality claims. Useful evidence may include technical data sheets, product identification, process records, test results and documented acceptance criteria. Depending on the application, relevant checks can include:
- coating thickness across accessible and difficult-to-reach areas;
- adhesion after curing;
- gloss, colour and surface appearance against the agreed reference;
- resistance to relevant chemicals, moisture, abrasion or corrosion;
- inspection of edges, apertures, threaded areas and masked zones; and
- records linking the finished parts to the coating materials and production instructions used.
Testing should be proportionate to the risk. A decorative internal component may need different verification from a fabricated part exposed to weather or industrial cleaning agents. The key question is whether the supplier can explain which checks are relevant and provide suitable records when required.
Assess control of materials and process changes. Powder, pre-treatment chemicals and ancillary materials should be identifiable and handled in a way that protects their condition. Ask how the supplier manages changes to coating materials, equipment settings or process instructions. A change that appears minor can affect colour, texture, adhesion or durability. Good control includes approval of alternatives, communication of significant changes and retention of records for the relevant production run.
Consider how the supplier manages samples and approval parts. For a visible stainless steel black finish, an agreed sample panel can establish the expected colour, texture, gloss and level of permissible visual variation before the main work begins. It is worth confirming who approves the sample, how it is stored for comparison and what happens if finished parts fall outside the agreed standard.
Examine practical production capability. The supplier should be able to explain how components will be fixtured, racked, masked and protected during processing. This matters where parts have contact surfaces, tight tolerances, drainage requirements, threaded holes or areas that must remain uncoated. Ask whether the proposed method could leave hook marks, powder build-up, edge defects or damage during unloading. For repeat work, confirm how the approved finish and component-specific instructions will be reproduced consistently.
Reliability also includes how problems are handled. Before placing an order, establish the process for reporting defects, reviewing disputed parts, approving rework and documenting corrective action. A clear non-conformance procedure is particularly important where coating damage may not be visible until assembly or installation. The supplier should be willing to identify the affected batch or component group and explain the proposed resolution.
Check the commercial and operational detail. A useful quotation should distinguish coating work from preparation, masking, packing and any other agreed requirements. It should identify assumptions about component condition, access, acceptable cosmetic marks, inspection documentation and responsibilities for protecting the parts before and after coating. Confirm how drawings, revisions, special instructions and photographs are controlled so that production is based on the current information.
Finally, consider whether the supplier’s communication style suits the project. Reliable working relationships depend on prompt clarification of technical uncertainties, accurate documentation and early notification of issues that could affect the agreed work. For Midlands manufacturers, fabricators, construction firms and automotive businesses, a regional supplier offering collection and delivery can also simplify the movement of metal components, provided packaging and handling requirements are agreed in advance.
In practical terms, the strongest choice is the supplier that can demonstrate substrate knowledge, application-specific technical reasoning, controlled material and process management, appropriate testing, careful component handling and transparent problem resolution. Comparing suppliers against these points gives a more dependable indication of quality than judging a black sample by appearance alone.
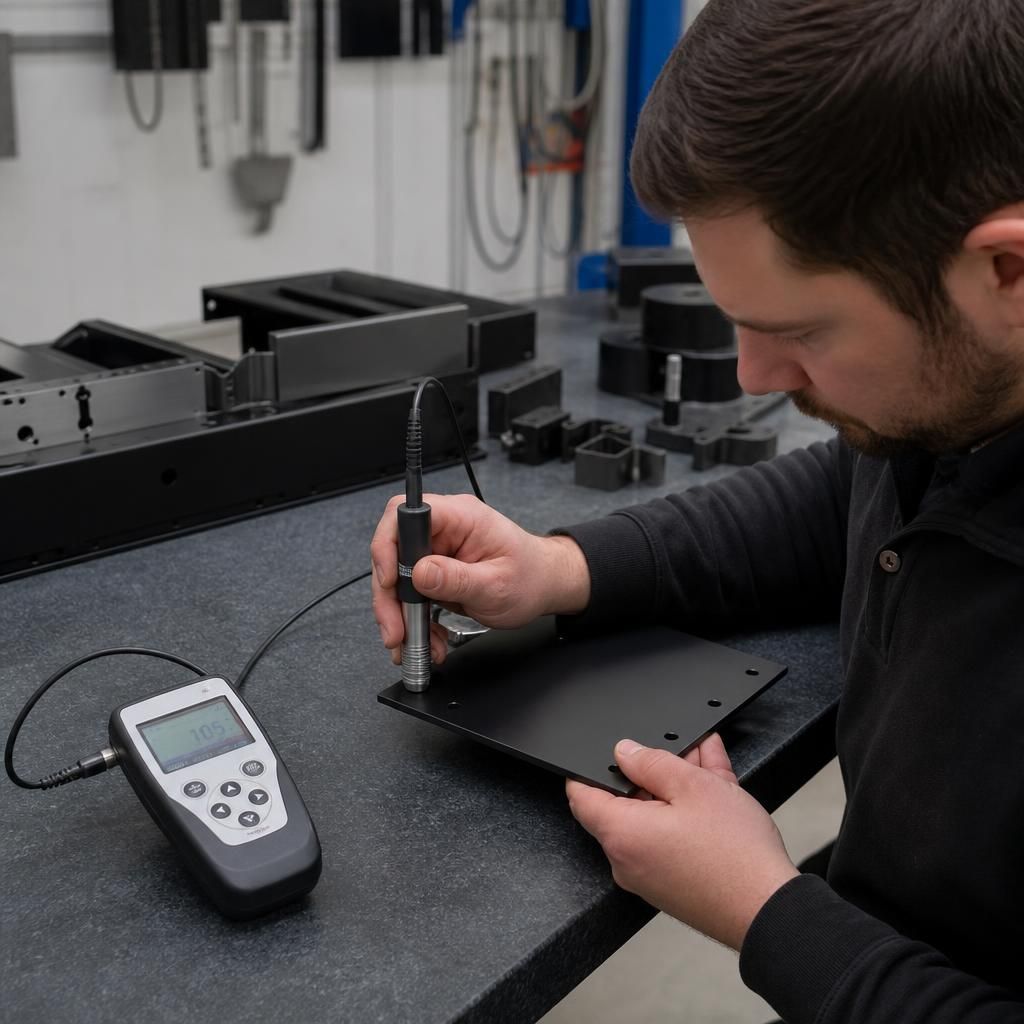
Another indicator of a reliable stainless steel black coating supplier is the quality of its inspection equipment and measurement methods. Visual checks are useful, but repeatable assessment also requires suitable instruments for coating thickness, gloss and, where relevant, colour comparison. Ask whether these instruments are maintained and calibrated, whether measurements are taken at defined locations, and how readings are recorded against the agreed specification. This helps distinguish a genuine process control system from an informal inspection based only on appearance. For repeat orders, consistent measurement methods also make it easier to identify whether a variation comes from the coating process, the component surface or the agreed acceptance criteria.