

What factors should I consider when selecting a shiny black powder coat finish for my metal components?
When selecting a shiny black powder coat finish for metal components, consider the required gloss level, substrate compatibility, operating environment, durability, application method and long-term maintenance needs. The finish should be specified to suit the component’s use, exposure to weather, handling, chemicals and expected appearance.
Choosing a shiny black powder coat finish is primarily a specification exercise: define the required visual standard, coating build, resin type, inspection criteria and production requirements before the components are processed. A high-gloss black surface reflects light strongly, so it can make minor preparation marks, inclusions, pinholes, uneven edges and handling damage more noticeable than a textured or low-sheen finish.
Set an objective gloss specification. “Shiny” is not a precise technical description. Agree the required gloss level with the coater and, where appearance is critical, specify how it will be measured and inspected. Gloss readings should be taken using an agreed method, while visual inspection should be carried out under consistent lighting and viewing conditions. Also confirm the acceptable degree of orange peel, waviness, cratering, dust inclusions and colour variation. A sample panel or approved reference component provides a more useful benchmark than a colour name alone.
Consider how black will appear across batches. Black powders can vary in undertone, gloss and visual depth even when they are described using the same general colour term. Components supplied in stages, or parts manufactured by different processes, may show differences caused by the substrate, surface profile, coating thickness or curing conditions. If parts are assembled together, request a retained reference sample and define whether matching applies to individual components, complete assemblies or future production batches.
Specify the coating system, not just the colour. The resin chemistry affects the way the coating responds to the component’s intended use, assembly conditions and exposure. For example, a system selected for interior fabricated parts may not be the appropriate choice for components exposed to weather, industrial contaminants or frequent contact. The powder supplier’s technical data should be checked for the relevant performance requirements, but the final specification should also account for the metal substrate and the preparation process available.
Check the required coating build and dimensional tolerances. Powder coating adds material to every coated surface, including holes, threads, mating faces, slots and close-fitting edges. Excessive build can affect fasteners, press fits, hinges, bearings and electrical contact points. Identify these areas on the drawings and state which surfaces require masking or should remain uncoated. Where a part must remain within a tight dimensional tolerance, agree how coating thickness will be controlled and verified.
Review the component’s geometry. Deep recesses, enclosed sections, sharp corners, narrow channels and closely spaced faces can influence powder coverage and the final appearance. Sharp edges may receive less effective coverage than adjacent flat areas, while recesses can collect powder or show differences in finish. Radiused edges, suitable drainage and access for cleaning can improve consistency. A design review before production may identify features that need masking, racking changes or a different coating specification.
Give surface preparation the same attention as the powder. The black finish cannot conceal oil, weld spatter, mill scale, corrosion, sharp burrs or contamination reliably. State how welds, seams and edges are to be finished before coating, and identify whether any existing coating must be removed. Parts should arrive free from substances that interfere with cleaning or adhesion. For steel, aluminium and other substrates, the preparation and pre-treatment must be suitable for that specific metal rather than treated as an interchangeable step.
Account for racking and contact points. The component must be electrically connected during powder application, so hooks or contact points leave a small uncoated area or require later touch-up. Decide where these marks may be placed, particularly on visible faces, assembly interfaces and conductive contact areas. The racking arrangement can also affect how parts hang, drain during pre-treatment and receive an even finish. Provide orientation requirements if appearance on a particular face is especially important.
Confirm curing requirements for the complete component. Powder curing depends on the metal reaching the specified temperature for the required time; the oven air temperature alone does not establish that the coating has cured correctly. Large, heavy or thermally varied parts may heat at different rates from small sections. Discuss the component’s mass, wall thickness and material with the coater, and agree how cure will be checked where performance is safety-critical or production consistency matters.
Define inspection and acceptance criteria in advance. A useful specification can include:
- the approved colour reference and gloss requirement;
- the permitted visual defects and the inspection distance or lighting conditions;
- the target coating thickness or acceptable range;
- areas that must be masked, left uncoated or protected during handling;
- the required adhesion, corrosion or chemical-resistance tests, where relevant;
- the treatment of rework, touch-up and rejected components; and
- the records or batch identification needed for traceability.
These details prevent disagreements based on subjective descriptions such as “deep black”, “perfectly smooth” or “high gloss”. They are particularly important when coated parts form part of a larger product or are supplied to another manufacturer for assembly.
Assess handling, packaging and assembly after coating. A cured powder finish can still be marked by metal-to-metal contact, abrasive packaging, straps or careless stacking. Parts should be supported at suitable contact points and separated where surfaces could rub. If components are drilled, cut, pressed, welded or machined after coating, decide whether those operations are practical and how exposed areas will be protected. Assembly tools and fasteners should not damage the visible finish or scrape coating from functional interfaces.
Allow for production and delivery practicalities. Batch size, component dimensions, part weight, packing requirements and the need to combine components into a single visual batch can affect the most suitable processing arrangement. Supply clear drawings, identify cosmetic faces and separate items requiring different specifications. Collection and delivery arrangements can also influence packaging and the condition in which parts arrive for coating or return to the production line.
The best shiny black specification therefore combines an approved appearance sample with measurable gloss, thickness, preparation, curing, masking and inspection requirements. This approach gives the coater clear technical boundaries and gives the manufacturer a consistent basis for accepting finished metal components.
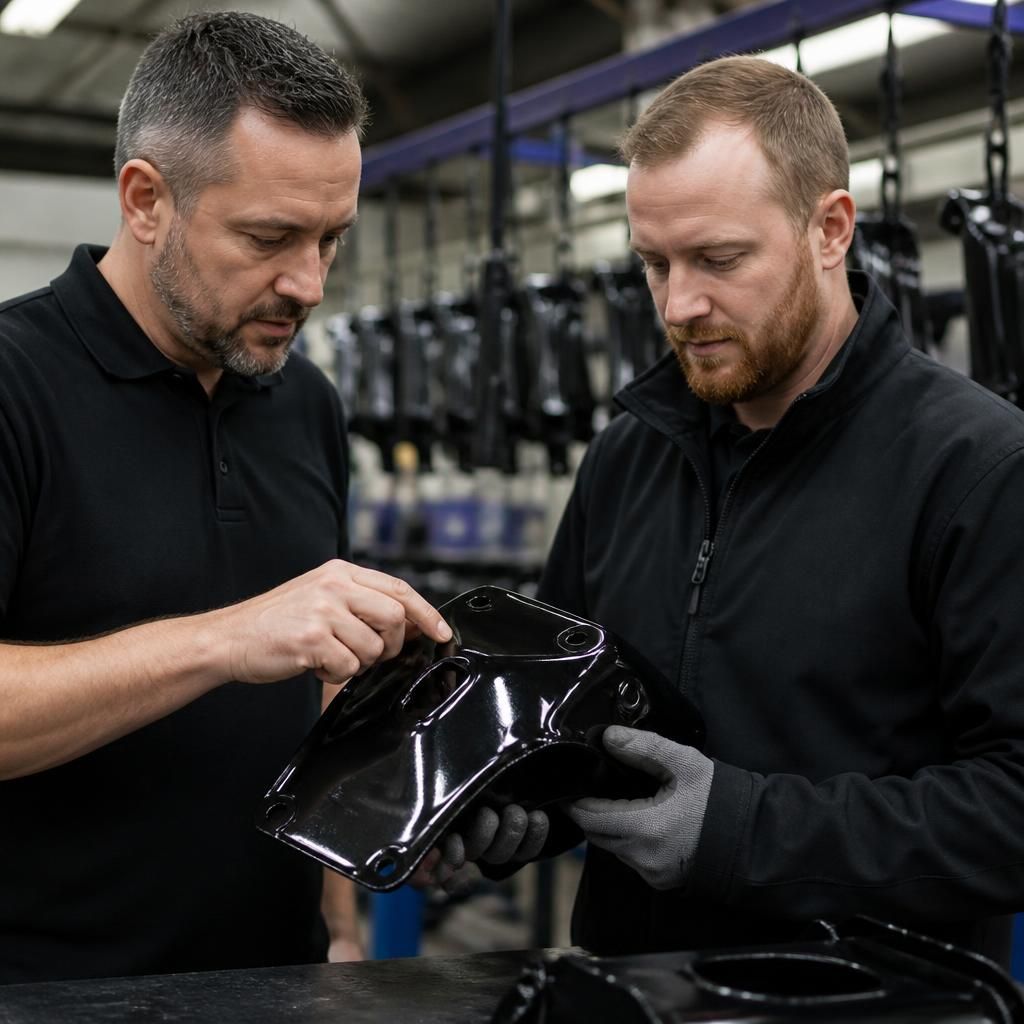
Check whether the finished component is subject to sector-specific performance or compliance requirements before choosing a shiny black powder coat. Parts used in regulated equipment, public-facing installations, electrical assemblies or environments with particular hygiene requirements may need documented evidence for properties beyond colour and gloss. The coating system should be assessed against the applicable specification rather than selected solely from an appearance sample.
Ask the coater or powder supplier what technical documentation is available for the proposed system, and retain it with the component specification. This can include declared resistance properties, application limitations and any relevant test information. Establishing these requirements at the design stage reduces the risk of selecting a visually suitable finish that cannot be used in the completed assembly.