

What is the environmental impact of using black powder coated metal products?
Black powder coated metal products can have a lower environmental impact than conventionally painted alternatives because powder coatings contain little or no solvent, produce lower volatile organic compound (VOC) emissions and create a durable finish that can extend product life. Their impact still includes energy used during curing and the manufacture and disposal of the metal and coating, so efficient application, responsible powder handling and end-of-life recycling are important.
The environmental impact of black powder coated metal products depends on their whole life cycle: the metal substrate, surface preparation, coating formulation, application method, curing, transport, maintenance and end-of-life treatment all contribute. Powder coating can reduce some emissions associated with solvent-based painting, but it is not impact-free. The most responsible choice is therefore one that combines an appropriate coating system with efficient production, controlled waste management and a clear plan for eventual recycling.
Material selection and product life
The metal beneath the coating is usually the largest material component of the product, so choosing an appropriate substrate and avoiding unnecessary over-specification can reduce resource use. Product design also matters. Components that can be repaired, refurbished, separated or reused generally have a better environmental profile than items designed for disposal after a single application.
A properly specified coating can help protect metal from corrosion, abrasion and weathering. This may reduce the need for replacement parts, repeated stripping and recoating, although the environmental benefit depends on the product’s actual service conditions and how well the coating system is matched to them. A finish intended for indoor use, for example, may be unsuitable for prolonged exposure to moisture, chemicals or ultraviolet light.
Formulation and chemical considerations
Powder coatings are supplied as dry particles rather than a liquid containing a large solvent carrier. However, the powder still contains resins, pigments, curing agents and other additives, each with its own manufacturing and disposal considerations. Black formulations can contain different pigment technologies, so colour alone does not establish the environmental credentials of a product.
Businesses comparing coating systems should request the relevant safety data sheet and technical information. These documents can help identify hazardous ingredients, handling requirements, curing conditions and disposal controls. Environmental assessment should consider the complete formulation rather than relying only on the absence of solvent or on general claims such as “green” or “eco-friendly”.
Surface preparation and pre-treatment
Pre-treatment is essential for adhesion and corrosion protection, but it can introduce additional environmental burdens. Degreasing may involve alkaline cleaners, while conversion treatments can use chemical solutions that require controlled storage and wastewater management. Rinsing also consumes water and can produce contaminated effluent containing oils, residues and dissolved metals.
The impact of this stage can be reduced through accurate process control, solution maintenance, water management and the correct treatment of waste streams. Parts should arrive suitably prepared where the agreed specification permits, and the coating provider should establish which cleaning and pre-treatment steps are actually required rather than applying unnecessary processes.
Application efficiency and production waste
Powder application can be highly controllable because unused airborne powder may be captured in suitable equipment. Whether it can be recovered and reused depends on the powder type, colour, contamination level and the required finish. Powder from different products or colours should not be mixed without confirming that the resulting material remains suitable for the intended application.
Good component racking, accurate gun settings and suitable application thickness help prevent rejects and excessive material use. Overspray, contaminated powder, used filters, masking materials and failed parts still need a defined waste route. Reclaiming material where technically appropriate is preferable to disposal, but recovery should not compromise coating performance or introduce defects that cause the part to be processed again.
Energy and transport
The coating has to be cured in an oven, and this makes the curing stage an important part of its environmental assessment. Energy use varies with the metal’s mass, the oven design, loading efficiency, cure schedule and the coating specification. Efficient loading and avoiding unnecessary rework can reduce energy associated with each usable batch.
Transport adds further impact through the movement of raw materials, metal components, finished goods, packaging and waste. Consolidating compatible deliveries, using suitable protective packaging and avoiding unnecessary journeys can help. For Midlands manufacturers and fabricators, collection and delivery arrangements can be considered as part of the wider process assessment, particularly where they reduce duplicated transport movements.
Maintenance, refurbishment and end of life
Routine cleaning with methods compatible with the coating can help prevent contamination and avoid premature stripping or replacement. When a component eventually reaches the end of its useful service, the metal should normally be directed into an appropriate scrap or recycling stream. The presence of a cured coating does not automatically make steel or aluminium unrecyclable, but local recyclers may have requirements concerning contamination, mixed materials, fixings or attached plastics.
Designing products for disassembly can improve recovery. Coated metal should be separated from non-metal parts where practical, and hazardous residues should not be sent into general scrap. Coating waste, chemical containers and contaminated consumables should be handled according to the applicable waste classification and disposal requirements rather than placed in ordinary commercial waste.
How businesses can make a better choice
- Define the actual exposure conditions before selecting the coating system, including moisture, chemicals, abrasion, temperature and ultraviolet exposure.
- Ask for formulation, safety and application information rather than assessing the product by colour or solvent content alone.
- Check how pre-treatment chemicals, overspray, filters and other process waste will be controlled.
- Use coating thickness and curing requirements appropriate to the specification to reduce rejects and unnecessary processing.
- Consider the product’s repair, disassembly and recycling route at the design stage.
- Compare the complete life cycle, including substrate, processing, transport, maintenance and end-of-life treatment.
For industrial buyers, environmental performance is best assessed as part of the coating specification and production process rather than as a standalone claim about black powder coating. A documented approach to materials, chemical control, waste, energy, transport and end-of-life recovery provides a more reliable basis for decision-making.
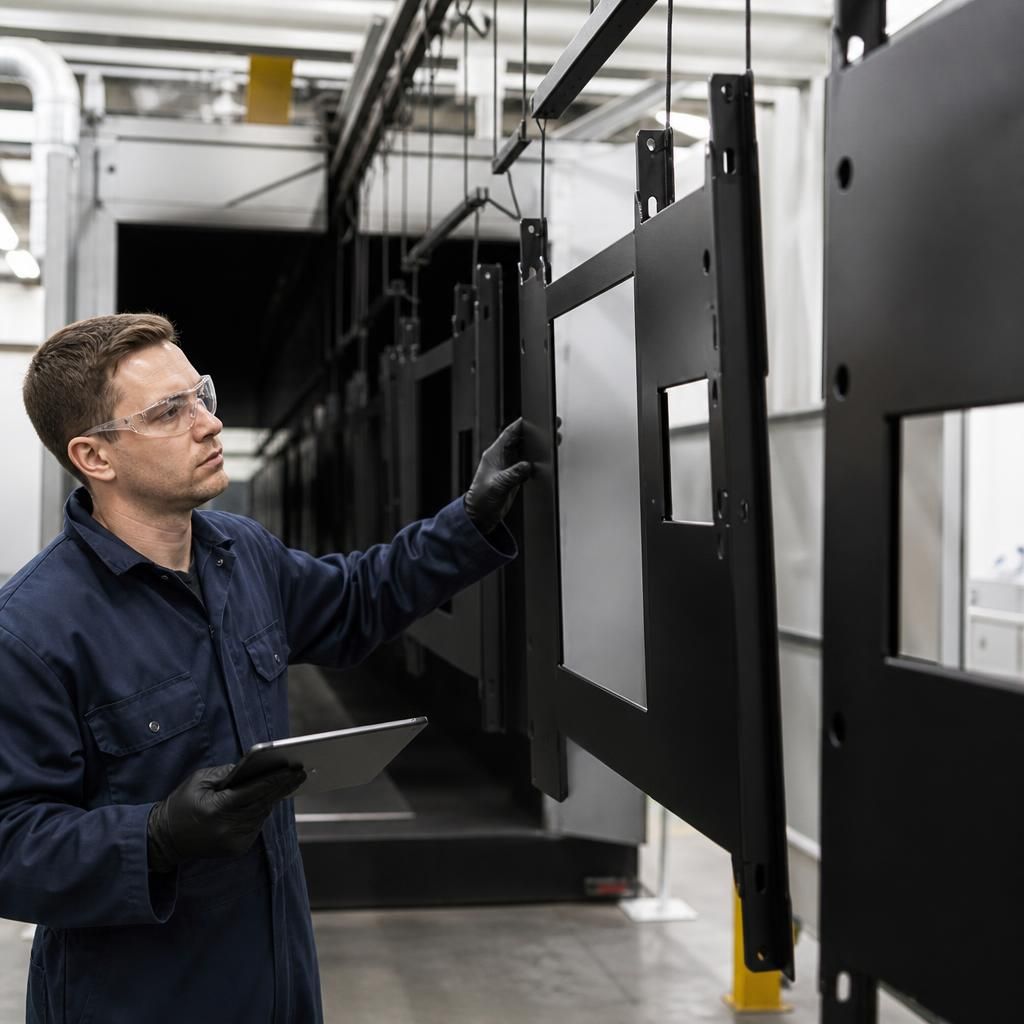
A meaningful environmental comparison should assess black powder coated products on a functional basis, rather than comparing coating materials in isolation. Review how much metal and coating are required, the expected service conditions, processing requirements and the likely replacement cycle for each option. Where available, environmental product declarations or lifecycle data can help, but check that the information covers equivalent products and uses the same assessment boundaries.
This approach prevents a lower-VOC coating from being treated as automatically sustainable. The relevant question is whether the complete product delivers the required performance with the least overall resource use and environmental burden.