

How can I ensure that my chosen corrosion coating will effectively handle the environmental conditions specific to my industry application?
Match the coating system to the steel component’s actual exposure, including moisture, salt, chemicals, temperature changes, abrasion and UV radiation, as well as the required service life. Confirm that the specification covers suitable surface preparation, coating thickness, powder chemistry and application controls, then use relevant performance testing or trial components to verify protection in the intended industry environment.
Choosing an effective corrosion coating means matching a documented coating system to the component’s complete duty cycle, not selecting a finish based on appearance alone. The decision should account for how the steel is designed, manufactured, installed, used, inspected and maintained, because these factors can determine whether corrosion begins at an exposed face, joint, edge or damaged area.
Start with the operating envelope. Record the conditions the component will experience throughout its intended service life. This includes whether exposure is continuous, intermittent or seasonal; whether the steel is indoors, outdoors, enclosed or partially sheltered; and whether contamination can accumulate on horizontal surfaces or in joints. A component that is nominally indoors may still encounter condensation, process vapours or wash-down water, while an outdoor item may be protected by a roof but remain vulnerable to trapped moisture.
Consider the consequences of coating failure as well as the likelihood of exposure. A decorative bracket and a structural or safety-critical component should not necessarily be specified in the same way. Where corrosion could affect fit, load-bearing performance, hygiene, electrical continuity or the operation of moving parts, the coating specification should be reviewed as part of the wider engineering risk assessment.
Check the design before specifying the finish. Coatings protect accessible steel surfaces; they cannot reliably compensate for poor drainage or inaccessible corrosion traps. Review folded sections, overlapping plates, threaded connections, welds, sharp internal corners and areas where dissimilar materials meet. Designs should allow water and residues to drain, avoid narrow gaps where possible, and provide access for coating, inspection and future maintenance. Weld spatter, porosity and rough transitions can create weak points even when the surrounding coating has been applied correctly.
Edges deserve particular attention. Powder can form a thinner film over sharp edges, and edges are also more likely to be damaged during handling and installation. Where the design permits, specify rounded or eased edges and make sure welds are finished to a suitable condition before treatment. Include lifting points, fixing holes and masked areas in the review rather than considering only the main visible faces.
Separate the coating requirement from the colour requirement. Colour, gloss and texture describe appearance; they do not by themselves define corrosion performance. The specification should identify the intended coating system, suitable substrate preparation, required film build, curing requirements and any topcoat or primer arrangement. If the component will be exposed to a particularly aggressive process or service condition, request technical confirmation that the selected system is intended for that duty rather than relying on a general-purpose architectural finish.
Assess compatibility with the surrounding process. Ask whether the finished part will contact oils, fuels, detergents, disinfectants, solvents, fertilisers, process chemicals or other substances during use or cleaning. The relevant question is not simply whether the coating is resistant to a chemical in isolation, but whether it can tolerate the chemical’s concentration, temperature, contact time and frequency of exposure. Occasional splashes may create a different requirement from permanent contact or immersion. Also establish whether the coating must remain stable when exposed to steam cleaning, pressure washing or repeated wetting and drying.
Temperature should be assessed as a range rather than a single operating figure. Repeated heating and cooling can place stress on the coating and the steel beneath it, particularly where the assembly includes materials with different rates of thermal expansion. Identify start-up and shutdown conditions, heat sources, cold storage, heat treatment after coating and any risk of condensation when a warm component enters a cooler environment. The powder manufacturer’s technical data should be checked for the intended service temperature and not only the curing schedule.
Account for mechanical damage. Abrasion, impact, sliding contact, vibration and repeated assembly can expose steel even where the chemical resistance of the coating is adequate. Identify contact points, loading zones, fork-lift routes, clamp locations and areas that will be bolted, drilled or cut after coating. If post-coating fabrication is unavoidable, define how exposed edges will be treated and protected. A coating selected for static atmospheric exposure may not be appropriate for components subject to regular impact or rubbing.
Use a recognised classification and evidence-based specification. For projects where corrosion risk is significant, the environmental category and expected durability should be recorded using the relevant project standard, such as the ISO 12944 framework where applicable. This creates a common basis for discussing the environment, preparation grade, coating system and inspection requirements. The specification should also state which test evidence is relevant. Laboratory results can help compare systems, but they do not reproduce every feature of a real installation, such as crevices, impact, contamination or poor drainage.
Ask for the information needed to verify the proposed system, including:
- the coating type and intended use;
- the approved substrate and preparation requirements;
- the specified film thickness and how it will be checked;
- the curing conditions and acceptable process tolerances;
- chemical, temperature, abrasion or weathering limitations;
- repair instructions for handling or installation damage; and
- inspection and documentation requirements for the finished parts.
Confirm the application route is suitable for the component. Large fabrications, enclosed sections, deep recesses and mixed assemblies may require more planning than simple, open profiles. Discuss masking, racking, access, handling and dimensional tolerances before production. These practical details can affect which surfaces receive a consistent finish and whether mating faces, threads, earth points or bearing areas need to remain uncoated.
Finally, define how the coating will be monitored in service. Inspection should focus on joints, edges, drainage points, fixings, impact zones and locations where deposits collect. Establish what constitutes acceptable damage and how repairs will be made without creating an incompatible patch. Keeping the coating specification, application records, inspection results and repair history together provides useful evidence if the operating environment changes or a recurring corrosion point is identified.
For a steel component being prepared for industrial powder coating, the most reliable approach is to give the applicator a complete duty description and engineering drawing, including any areas that must remain uncoated. A specialist coating provider can then assess the practical application requirements against the specified environmental duty, while the final choice remains tied to the component’s design, risk level and documented performance needs.
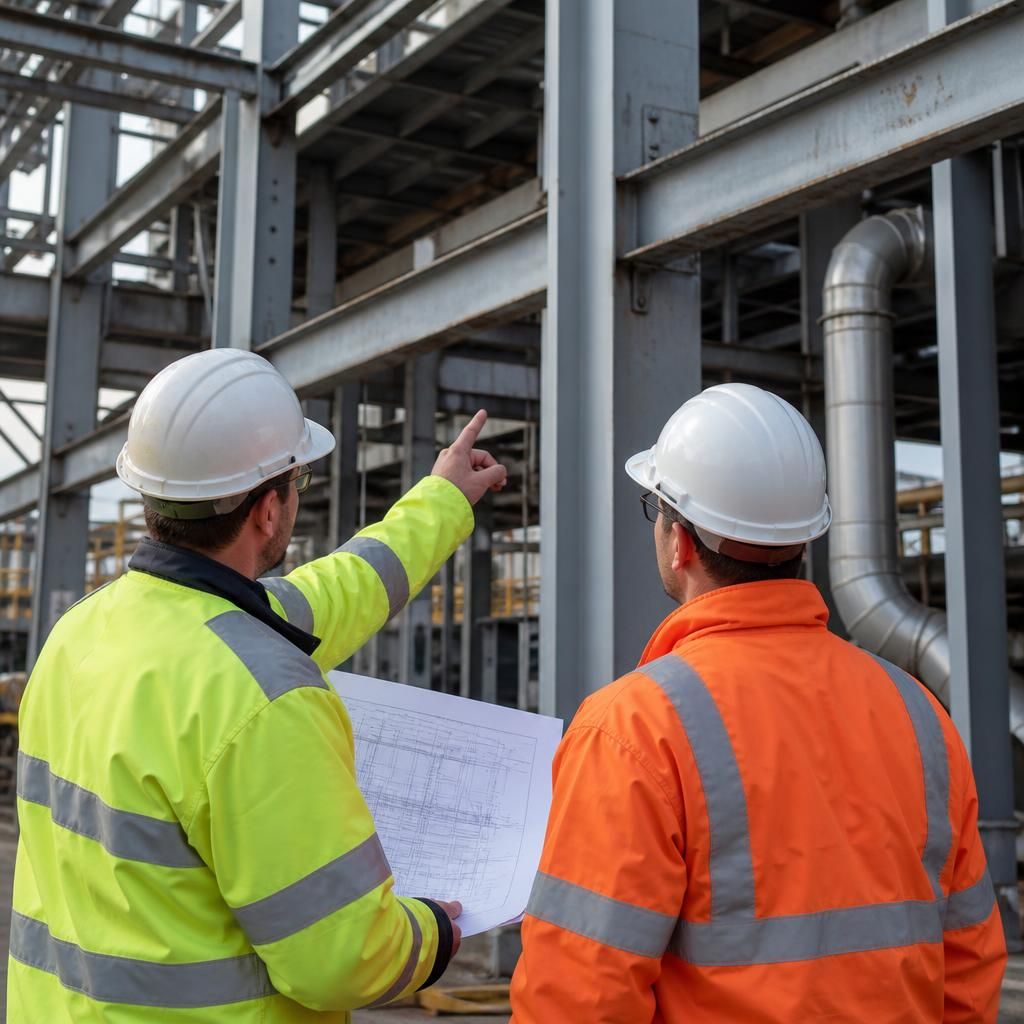
Environmental conditions can vary significantly across a single installation, so one coating specification may not suit every part of an assembly. Separate components by exposure zone, such as fully sheltered areas, open external faces, splash zones, plant-room interiors and locations near exhausts or wash-down equipment. Consider the least protected surface rather than the average site condition, particularly where steel passes through a wall, sits close to the ground or is positioned beneath equipment that can discharge water or contaminants.
Record these zones on the drawing or coating schedule and identify whether each requires the same system or a different level of protection. This approach helps prevent a component being specified for a mild indoor environment when part of it will experience outdoor moisture, concentrated deposits or repeated wetting in service.