

What are the specific industry standards for powder coating thickness on steel, and how do they ensure optimal performance and durability?
Powder coating thickness on steel is normally specified according to the required corrosion category, service environment and coating system rather than one universal value; standards such as BS EN ISO 12944 establish performance requirements, while BS EN ISO 2808 and BS EN ISO 19840 set out dry-film thickness measurement and acceptance principles. These standards support consistent inspection by defining how thickness is measured and assessed, helping ensure the coating provides the intended protection, adhesion and durability.
For a steel powder-coating specification, the key compliance chain is the corrosion-protection system defined under BS EN ISO 12944, the film-thickness measurement methods in BS EN ISO 2808, and the acceptance principles in BS EN ISO 19840. Together, these standards turn a general requirement for a durable finish into a controlled specification covering substrate preparation, coating system, target dry-film thickness, measurement method and permissible variation.
BS EN ISO 12944 establishes the performance framework. It classifies corrosive environments, considers the expected durability of the protective system and provides guidance on selecting coating systems for steel. The specification should therefore identify the conditions the component will face, such as indoor industrial exposure, persistent moisture, salt contamination, chemical contact or outdoor weathering. The selected powder system and its required thickness must match that environment; a coating suitable for a dry internal location should not automatically be treated as suitable for exposed steel.
ISO 12944 also makes clear that film thickness cannot be considered separately from the coating system. The specification may need to cover the steel grade, preparation standard, primer or pre-treatment, powder topcoat, number of layers and curing requirements. Where a primer and topcoat are used, the required thickness may apply to each layer as well as to the completed system. The agreed documentation should make this distinction clear so that an inspector does not assess a multilayer system against an unsuitable single-coat requirement.
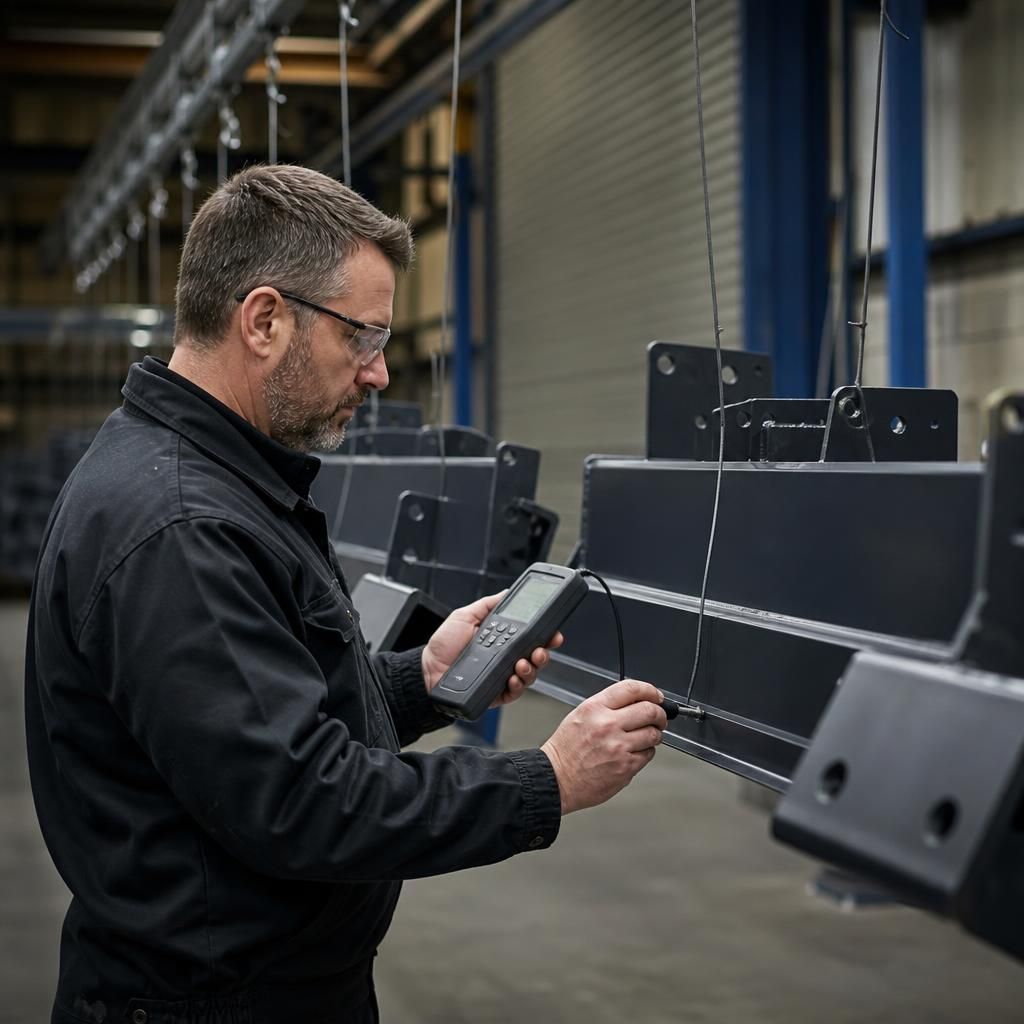
BS EN ISO 2808 defines how coating thickness is determined. It includes methods for measuring dry-film thickness using suitable gauges and, where necessary, destructive techniques. For powder-coated steel, non-destructive electromagnetic measurement is commonly practical because it checks the cured film without removing it. The selected instrument must be appropriate for the steel substrate, the expected coating range and the component geometry.
Measurement equipment should be checked, calibrated or verified in accordance with the applicable procedure before readings are taken. Readings taken close to edges, corners, holes, welds, folds or recesses may not represent the main surface because powder behaves differently around changes in geometry. A sound inspection plan therefore identifies measurement zones and records results from representative areas rather than relying on one convenient reading.
BS EN ISO 19840 provides the acceptance approach for rough steel surfaces. Abrasive blasting can create a surface profile that affects both coating coverage and gauge readings. The standard addresses how measurements are distributed across the inspected area, how individual and mean results are considered, and how surface roughness correction is applied where relevant. This prevents an apparently precise thickness result from being interpreted without accounting for the texture beneath the film.
The purchase specification should state which areas are subject to inspection, how many readings are required, how readings are grouped, and how borderline results are handled. It should also identify whether the requirement applies to the complete component or to defined coating zones. This is particularly important for fabricated steelwork containing flat plate, tubular sections, sharp edges, welds and sheltered recesses, as these areas may receive different amounts of powder during application.
Surface preparation standards support, rather than replace, the thickness standards. BS EN ISO 8501-1 is used to describe visual preparation conditions, while the ISO 8503 series concerns surface profile produced by abrasive blast-cleaning. These controls matter because contamination, mill scale, rust, weld spatter and an unsuitable profile can undermine the coating even when the measured film thickness is within specification. The steel should be clean and appropriately prepared before powder is applied, with welds and fabrication defects dealt with as part of the preparation process.
Where steel has been hot-dip galvanised, BS EN ISO 1461 may be relevant to the galvanised layer, but it is not a substitute for the powder-coating requirements. A galvanised-and-powder-coated component is a duplex system. Its specification should address the condition of the zinc surface, preparation compatible with galvanised steel, any required pre-treatment or primer, and the thickness and cure of the powder layer. Assessing only the powder thickness would not verify the performance of the complete system.
Thickness is accepted as part of a wider quality assessment. A coating that meets a dry-film requirement may still fail to perform if it is poorly cured, contaminated, poorly bonded or damaged during handling. Depending on the service environment and contract requirements, inspection may therefore also include visual appearance, adhesion, cure, surface cleanliness and checks for defects such as pinholes, runs, craters, missed areas or exposed steel. Corrosion and durability testing may be specified for the coating system, but laboratory test results should not be treated as a direct guarantee of identical field life.
Excess thickness can be as problematic as insufficient thickness. A thin film may leave weak coverage over peaks in the steel profile or vulnerable areas around edges. An excessively heavy film can affect appearance, curing behaviour, flexibility and the fit of assembled parts. The correct objective is not simply to apply as much powder as possible; it is to achieve the specified thickness consistently across the areas that control service performance.
A robust inspection record should link each result to the component or batch, coating system, preparation condition, powder identification, application settings and cure verification. If readings fall outside the agreed acceptance criteria, the cause should be investigated before rework is selected. Possible causes include incorrect gun settings, poor earthing, unsuitable hanging, contamination, inadequate preparation, excessive powder build-up or insufficient oven exposure. Rework should be controlled so that additional coating does not create a new thickness or adhesion problem.
For B2B steelwork, the most useful specification combines the relevant ISO standards with project-specific details: the corrosive environment, required durability category, substrate and preparation condition, coating layers, target dry-film thickness, tolerances, inspection locations, test methods and documentation. This approach ensures that thickness readings are interpreted in context and that the finished coating is judged against the performance required from the steel component, rather than against an arbitrary thickness value.
Industry standards for powder coating steel generally define how protection is specified and verified; they do not impose one mandatory thickness for every component. The required value is established by the agreed coating system, the steel’s service environment and the project specification. This distinction prevents a measurement standard from being mistaken for a universal application requirement.
A practical specification should therefore state which standard applies, the coating system being assessed, the target dry-film thickness and the acceptance criteria. It should also identify the relevant edition of each standard and resolve any differences between the client’s requirements, the coating system’s technical documentation and the inspection procedure. Clear allocation of these requirements makes results comparable between batches and gives any corrective action a defined technical basis.
Discuss your steel coating thickness specification
If you are preparing a steel coating specification, discuss the component, service environment and inspection requirements with the powder-coating team before production is arranged. This provides a practical basis for confirming the proposed coating system and thickness controls.