

What methods ensure proper thickness control during the powder coating of steel components?
Proper thickness control during powder coating of steel components relies on consistent powder application, controlled gun settings and regular measurement with a calibrated dry-film thickness gauge. Operators verify coverage across representative areas, adjust application where readings vary and record results against the specified coating thickness.
Proper thickness control for powder-coated steel is achieved through a defined coating specification, suitable component design, controlled preparation and a repeatable production process. The aim is not simply to apply as much powder as possible, but to produce a continuous film within the specified range while avoiding thin areas, excessive build, poor edge coverage and defects caused by over-application.
Start with a clear coating specification. The required dry-film thickness should be agreed before production and linked to the intended service conditions, powder type, colour and finish. The specification should identify the acceptable range, the areas that are critical to performance and whether edges, recesses, welds or concealed faces have separate requirements. A defined acceptance standard prevents operators from treating a visual impression of coverage as sufficient, particularly where a smooth finish can make a heavy or light film difficult to detect by eye.
Assess the component geometry before coating. Steel parts with deep recesses, narrow channels, closely spaced faces and sharp internal corners do not accept powder uniformly. Electrostatic powder can be repelled from areas where the electric field becomes concentrated, a condition commonly associated with Faraday cage effects. The coating plan may therefore need changes to part orientation, hook position, gun approach or the sequence in which surfaces are presented. These decisions are made around the shape of the component rather than applying one arrangement to every part.
Edges require particular attention. Powder can pull away from sharp corners during curing, leaving reduced coverage at the point most exposed to handling and environmental attack. Specifying suitable edge radii during fabrication helps the powder form a more continuous film. Where redesign is not possible, the coating process must recognise the edge condition and include appropriate checks rather than assuming that a reading on a broad flat face represents the whole component.
Control the condition of the steel and the pre-treatment. Surface contamination, residual oil, abrasive dust, flash rust or poorly treated weld areas can affect how powder deposits and flows. They can also create local defects that are mistaken for a thickness problem. Consistent cleaning, rinsing and drying provide a more uniform surface for application. Any blasted profile should be appropriate to the coating system: an excessively rough profile can consume part of the measured film and produce peaks with lower effective coverage, while an unsuitable profile can affect adhesion and appearance.
Use a controlled powder supply. Powder should be stored and handled in accordance with the product supplier’s requirements so that moisture, contamination and agglomeration do not alter its feeding or deposition characteristics. Reclaimed powder, where permitted by the coating system, needs controlled proportioning and suitable filtration. Unmanaged reclaim can change the blend’s behaviour, colour and finish, making the process less predictable even when the equipment settings remain unchanged. The powder batch, colour and finish should be traceable to the relevant production work.
Manage grounding and part presentation. A sound earth path through the rack, hooks and component is essential for electrostatic transfer. Paint build-up on contact points, poor hook contact or insulating contamination can reduce attraction between the powder and the steel. Racks and hooks should therefore be kept suitable for the work, with contact points positioned so they remain effective without creating unacceptable uncoated areas. Parts should also be spaced and oriented to avoid shielding one another or allowing powder to accumulate unevenly on adjacent faces.
Use a process control plan. A practical plan sets out the coating specification, component orientation, rack arrangement, powder identity, equipment checks, curing requirements and inspection points. It should distinguish between first-off approval, routine production checks and investigation of non-conforming parts. A trial component or test panel can be used to confirm the chosen process before a batch is released, especially where the shape contains difficult recesses or the coating system is being introduced for the first time.
Separate thickness from cure assessment. Thickness and curing are related but they are not interchangeable. A film can fall within the specified thickness range and still have inadequate performance if the steel does not reach the powder manufacturer’s required metal temperature and time. Conversely, increasing film build does not correct an under-cured coating. The curing cycle should account for the component’s mass and geometry, and the coating process should retain evidence that the required cycle has been followed.
When results fall outside the agreed range, the cause should be investigated systematically rather than corrected by adding powder indiscriminately. Review the component orientation, contact and grounding, powder condition, difficult geometric features, preparation quality and curing conditions. Rework decisions should also consider whether additional coating will create excessive build, interfere with assembly tolerances or obscure the original defect. This approach makes thickness control a repeatable quality process across steel components of different sizes and designs.
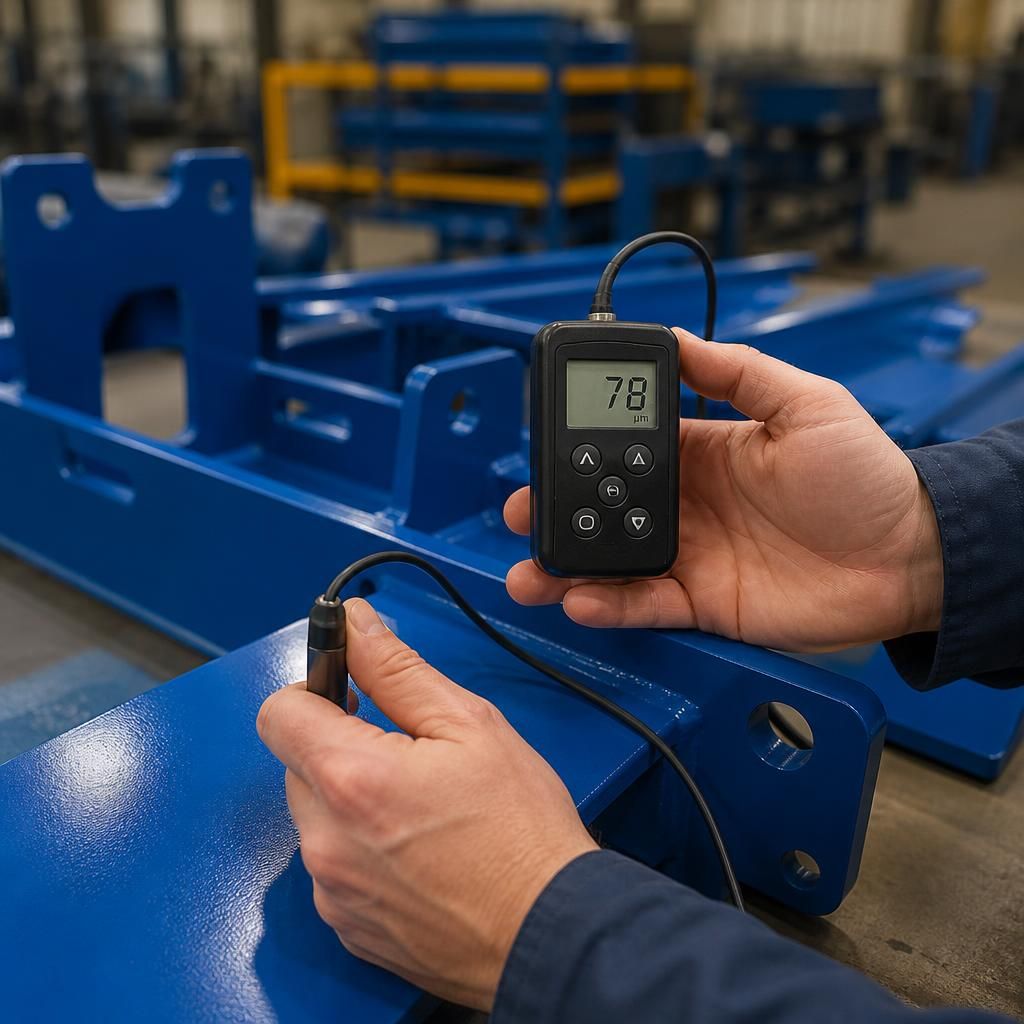
Reliable thickness verification depends on using a measurement method suited to the coated steel and applying it consistently. A dry-film gauge should be checked against suitable reference standards and, where necessary, adjusted for the steel substrate and surface profile before readings are taken. Measurements should follow a documented location plan covering broad faces, edges and less accessible areas, with several readings used to identify local variation rather than relying on one result. Recording individual readings also helps distinguish an isolated low spot from a wider application problem and provides evidence that the finished component meets its specified thickness range.