

What factors should be considered when deciding whether to use custom or standard pretreatment solutions for your metal components?
Choose a standard pretreatment when the metal type, operating environment and required coating performance fit an established process; choose a custom solution when unusual substrates, contamination, component geometry or demanding durability requirements need a tailored approach. The decision should also consider batch consistency, production volumes, compatibility with the powder and curing process, environmental obligations, and the total cost of preparation and rework.
Standard pretreatment is usually appropriate when a component fits a proven process, while custom pretreatment is justified when the substrate, surface condition or specification falls outside that process. The decision should be based on technical suitability first, then assessed against process control, compliance requirements and the full cost of achieving an acceptable coated part.
Start with the coating specification. Define what the pretreatment must achieve before comparing products or process routes. Relevant requirements may include adhesion after forming or assembly, resistance to moisture and chemicals, protection of cut edges and weld areas, and consistency of the visible finish. A standard system may meet a general specification, but a more tailored sequence could be necessary where the component has a critical service function or will be exposed to conditions that place greater demands on the coating interface.
Examine the actual condition of the components. The incoming surface may contain drawing oils, fabrication lubricants, mill scale, oxide layers, weld discolouration, handling marks or residues from previous operations. These conditions can vary between suppliers and production batches. If they are predictable and within the working range of an established cleaning and conversion process, standard pretreatment may be suitable. If they vary significantly, a custom approach may involve additional cleaning, activation, mechanical preparation or a revised process sequence.
Component design is also important. Deep recesses, narrow gaps, overlapping parts, threaded features and enclosed sections can restrict chemical contact and rinsing. Poor drainage can leave residues that interfere with powder adhesion or create staining during curing. In these situations, the question is not simply which chemical to use; the pretreatment stages, racking method, spray coverage, rinsing and drying conditions may all need to be reviewed.
Consider whether one process can accommodate the production mix. A standard solution may work well where parts are made from a consistent material and follow the same fabrication route. A mixed workload containing different grades, castings, galvanised items or aluminium parts may require separate treatment windows or a more carefully controlled universal process. Combining incompatible substrates without validation can produce uneven appearance, variable adhesion or excessive chemical consumption. Where separation is practical, a standard process for each defined component group may be more reliable than forcing one custom treatment across everything.
Check the pretreatment plant and operating controls. A chemical formulation cannot compensate for unsuitable application conditions. The assessment should cover bath or spray temperature, concentration, contact time, rinse quality, water management, drying and the method used to monitor the process. A custom solution may require extra tanks, dosing controls, filtration, more frequent checks or changes to line speed. If the existing plant cannot apply the process consistently, a theoretically superior chemistry may be less suitable than a standard system that can be controlled properly.
Review compatibility with the whole coating route. The residue left by pretreatment must be compatible with the selected powder, the drying stage and the curing schedule. Some surfaces or conversion layers can influence colour uniformity, gloss, edge coverage or the appearance of defects. Trials should therefore assess the complete sequence rather than the pretreatment in isolation. This is particularly important where the final finish has a tight visual specification, such as a smooth architectural surface, a textured coating or a dark colour that can reveal marks more readily.
Use validation to distinguish a genuine need from unnecessary customisation. A practical evaluation can include representative components or test panels processed through the proposed route. Assessment may cover visual uniformity, powder adhesion, cross-cut performance, resistance to handling damage and relevant corrosion testing. The results should be recorded alongside the substrate condition and process settings. If a standard system meets the required criteria repeatedly, customisation may add complexity without a corresponding technical benefit. If it fails at a specific stage, the evidence helps identify whether the remedy should be a chemical change, better cleaning, altered rinsing or a design adjustment.
Account for control, documentation and future repeatability. A custom process should have clear operating limits, inspection requirements and instructions for dealing with deviations. This is especially important when work is carried out in batches or by more than one operator. The process should remain understandable and repeatable when raw materials, component suppliers or production quantities change. A standard system is not automatically easier to control, but established operating guidance can reduce the amount of process development required.
Compare total operational impact rather than purchase price alone. The comparison should include chemical use, water and waste treatment, plant modifications, cleaning, maintenance, testing, operator training, line changes and the cost of rejected or reworked components. A custom solution can be worthwhile where it addresses a defined technical problem and reduces recurring defects. Conversely, a standard route may be preferable when it satisfies the specification and avoids additional handling or control requirements.
A sound decision therefore follows a documented sequence: define the performance requirement, inspect the substrate and component design, confirm what the existing plant can control, run representative trials, and compare the validated options over their complete operating life. Custom pretreatment should be selected for a demonstrated requirement, not simply because it is more specialised; standard pretreatment should be selected only after confirming that its process limits match the parts being coated.
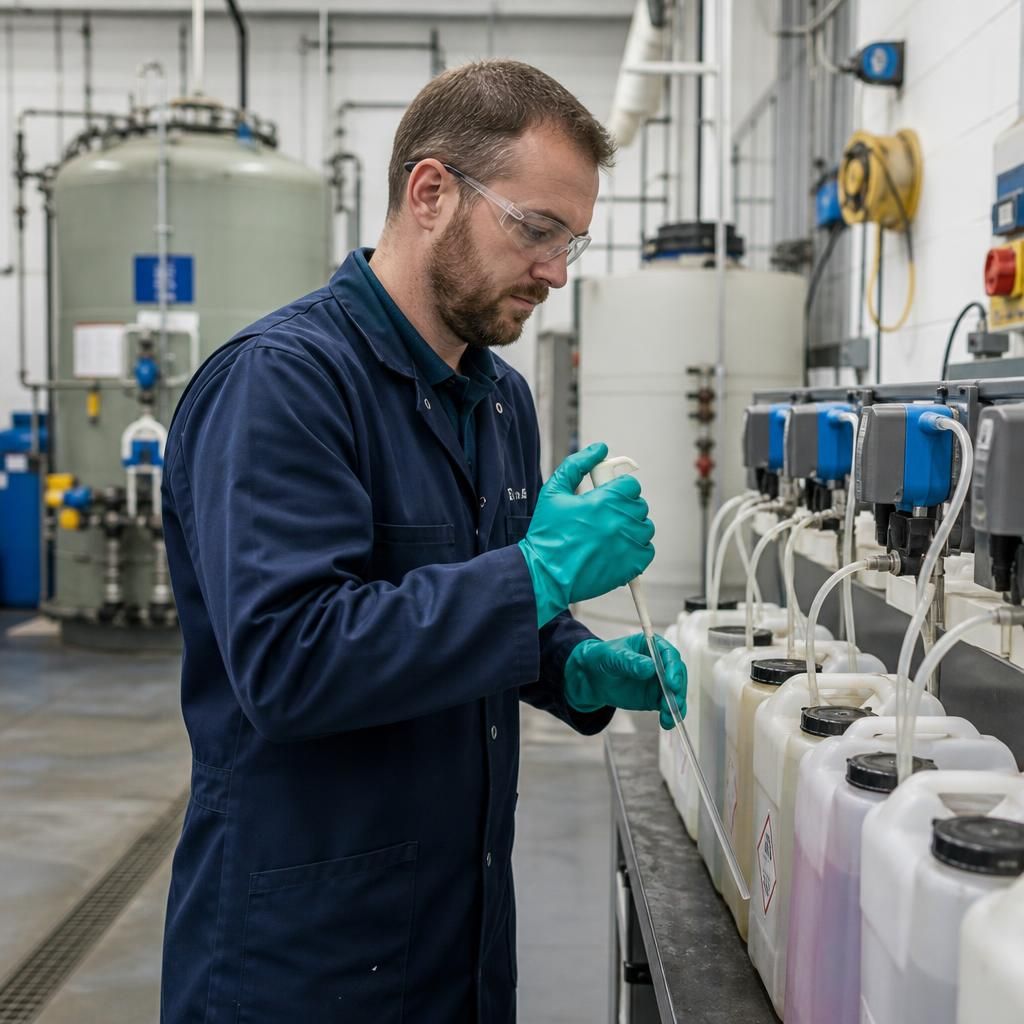
Environmental and handling requirements can influence the choice between standard and custom pretreatment as much as coating performance. Compare the chemical classification, storage needs, operator controls, rinse-water management and waste-treatment requirements of each option. A custom solution may deliver a useful technical improvement but become unsuitable if it creates disproportionate treatment, disposal or compliance demands.
Review these implications before approving production trials, using the actual plant and waste-management arrangements as part of the assessment. The preferred pretreatment is the one that achieves the required metal protection and coating compatibility while remaining practical to control, document and manage responsibly.
Discuss the Right Pretreatment for Your Metal Components
If you are unsure whether a standard or custom pretreatment is suitable, discuss your metal type, component design and coating specification with a powder coating specialist. This allows the proposed process to be assessed against the part’s actual requirements before production approval.