

What specific industry certifications and standards does the thermoplastic powder coating process meet or exceed?
Thermoplastic powder coating does not automatically meet one universal certification or standard; conformity depends on the powder formulation, substrate, surface preparation, application method and test results. Relevant requirements may cover coating thickness, adhesion, impact, corrosion, chemical resistance or electrical insulation, so compliance should be verified against the specific customer, product and sector specification.
The standards most often used to assess thermoplastic powder coating relate to surface preparation, coating thickness, adhesion, impact resistance, corrosion protection, chemical resistance, appearance and electrical performance. A coating specification normally identifies the required tests, acceptance limits and reporting method rather than relying on the term “thermoplastic powder coating” alone.
Commonly relevant standards include:
- BS EN ISO 8501-1 for assessing the visual cleanliness of steel surfaces before coating. Suitable preparation is essential because contamination, mill scale, rust or poorly prepared areas can reduce coating adhesion.
- BS EN ISO 8503 for describing and measuring the surface profile of blast-cleaned steel. The profile must be compatible with the coating system and specified film thickness.
- BS EN ISO 2808 for determining coating thickness. This helps confirm that the applied layer is within the range required for the component and its service conditions.
- BS EN ISO 2409 for cross-cut adhesion testing, where a lattice is made through the coating and the amount of detachment is assessed.
- BS EN ISO 4624 for pull-off adhesion testing. This is useful where a quantitative assessment is required or where the coating is being evaluated on a critical component.
- BS EN ISO 6272 for resistance to rapid deformation and impact. It can help establish whether the coating is suitable for parts likely to experience handling, knocks or mechanical service loads.
- BS EN ISO 9227 for neutral salt spray testing. This provides comparative information about corrosion resistance, although salt spray results should not be treated as a direct prediction of service life in every environment.
- BS EN ISO 2813 for measuring specular gloss. This is relevant where the finish must remain within a defined gloss range.
- BS EN ISO 12944 for the classification and selection of corrosion-protection systems in atmospheric environments. Its use depends on the substrate, coating system, preparation and corrosivity category specified for the project.
Other tests may be selected for the environment in which the coated part will operate. These can include resistance to water, humidity, oils, fuels, cleaning agents, acids, alkalis, solvents, abrasion and weathering. The appropriate method depends on the thermoplastic chemistry, such as nylon or another polymer, as well as the substrate and intended use. A test result for one formulation cannot automatically be transferred to another powder or application thickness.
Electrical applications require separate evidence. Where the coating is intended to provide insulation, the specification may include dielectric strength, insulation resistance, volume resistivity or tracking performance. Methods such as IEC 60243 or equivalent electrical test standards may be relevant, but the finished component must be tested in its actual configuration. Coating continuity, edges, apertures, film thickness and surface contamination can all affect the result.
Regulatory requirements are different from performance standards. UK REACH and restrictions on hazardous substances may affect the composition and use of coating materials. RoHS requirements may apply to electrical and electronic equipment placed on the relevant market. These regimes concern chemical content and product compliance; they do not, by themselves, demonstrate adhesion, corrosion resistance or mechanical durability.
Certification schemes should also be treated carefully. An applicator may hold a management-system certification such as ISO 9001, but that certification covers the organisation’s quality-management arrangements rather than proving that every thermoplastic coating meets a particular performance level. Sector schemes and project approvals may impose additional requirements, especially for architectural, transport, electrical or safety-related components. A scheme intended for a different coating technology should not be assumed to cover thermoplastic powder coating.
For a meaningful conformity assessment, the coating specification should record the powder type, substrate, preparation method, application process, curing or fusion conditions where applicable, target thickness, test methods and acceptance criteria. It should also identify any areas that are excluded from testing, such as masked surfaces, weld zones or difficult-to-coat recesses. Test certificates and batch records then provide traceability between the approved system and the finished parts.
Manufacturers and fabricators should therefore request evidence against the standards named in their drawing, contract or sector specification. The most useful documentation may include the product technical data sheet, preparation and application records, thickness measurements, adhesion and impact results, corrosion or chemical-resistance tests, and any electrical or sector-specific approvals. This approach establishes whether the particular thermoplastic coating system meets the required standard, rather than treating a general process description as certification.
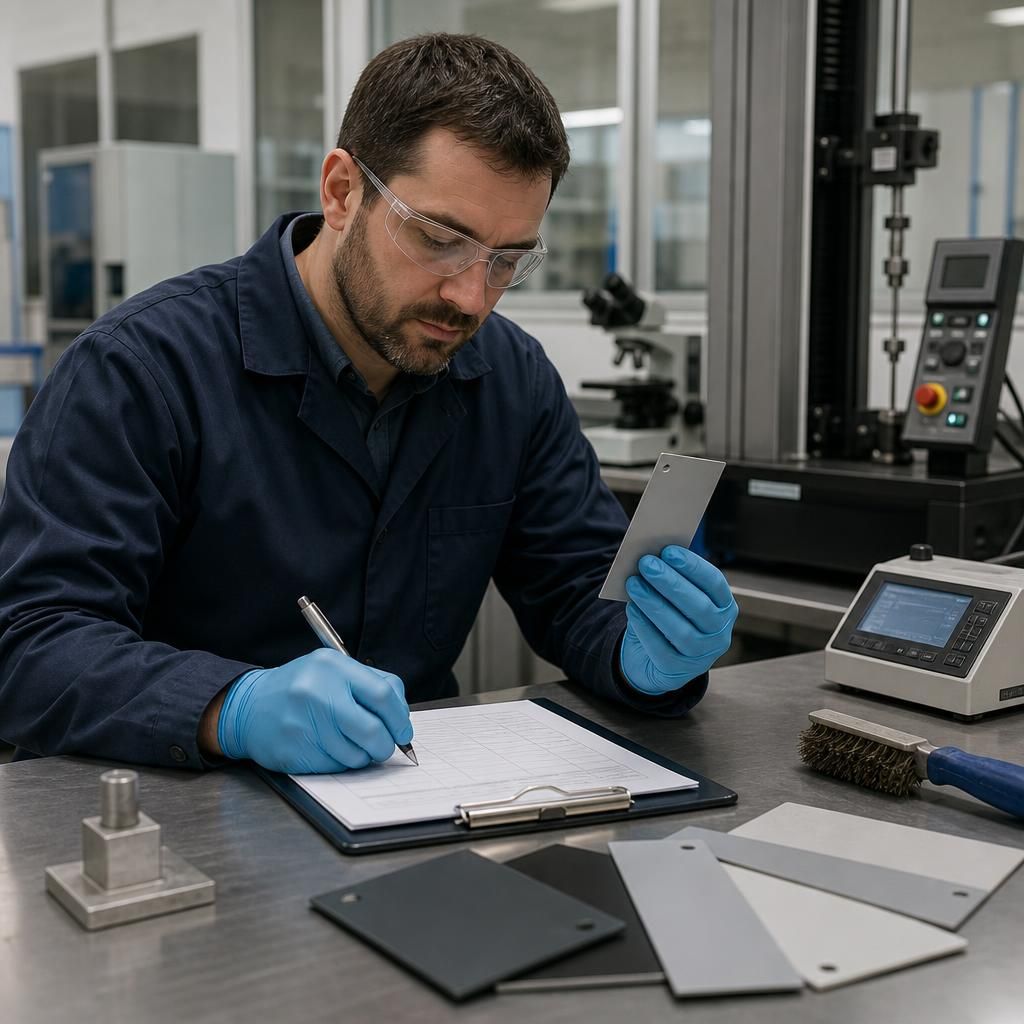
A coating test report is meaningful only when its result relates to the finished coating system being specified. The report should identify the thermoplastic formulation, substrate, preparation, applied thickness and test conditions, so the result can be interpreted against the component’s intended use rather than treated as approval of every application of that powder.
This distinction is particularly important when comparing suppliers or coating options. A named standard indicates how a property was assessed; it does not, by itself, confirm that the result is suitable for a particular service environment. Check the complete test context and the stated acceptance requirements before treating certification or test evidence as proof of conformity.