

What are the different stages involved in a powder coating process?
A powder coating process typically involves six stages: inspecting and masking the component, cleaning the metal, applying any chemical pre-treatment, spraying the powder electrostatically, curing it in an oven, and carrying out final inspection and finishing checks. Each stage contributes to adhesion, coating coverage, appearance and the long-term performance of the finished metal component.
A powder coating process is a controlled sequence that prepares a metal surface, deposits a dry polymer powder and converts it into a continuous protective film. The quality of the result depends on how well each operation is matched to the component’s metal type, geometry, intended use and specified finish.
1. Pre-process specification and component assessment
Before treatment begins, the component should be assessed for its substrate, dimensions, condition and service environment. Steel, galvanised steel, aluminium and other metals can require different preparation methods. The coating specification should also identify the required colour, texture, gloss level, film thickness, masking points and performance requirements.
This assessment identifies features that may affect the result, including threaded holes, tight corners, drainage points, welds, sharp edges and enclosed sections. Parts need suitable hanging or racking points so that they can be handled safely and coated without creating excessive contact marks. Any areas that must remain free of coating are protected with suitable plugs, caps or high-temperature masking materials.
2. Surface preparation
Preparation removes contaminants and creates a surface to which the coating can bond. Oil, grease, dirt, mill scale, rust, weld residues and previous coatings can all interfere with adhesion or cause defects. The appropriate method may include alkaline or solvent cleaning, mechanical preparation, abrasive blasting, or a combination of techniques.
Blasting can remove corrosion and provide a suitable surface profile, while cleaning processes remove residues that are not always visible. The selected method must be controlled carefully: excessive abrasion can alter dimensions or leave an unsuitable profile, whereas insufficient preparation may leave contamination beneath the coating.
After preparation, components must be handled in a way that prevents recontamination. Moisture is particularly important because trapped water can contribute to flash rusting, blistering or poor adhesion. Parts should therefore be dry before powder application.
3. Chemical pre-treatment
Where the specification calls for it, a chemical conversion treatment is applied after cleaning. This creates a more receptive surface and can improve resistance to corrosion beneath the coating, particularly where the finished component may encounter moisture or demanding industrial conditions.
The treatment sequence may include rinsing and controlled drying. Its effectiveness depends on factors such as chemical concentration, contact time, temperature, water quality and the condition of the underlying metal. Galvanised surfaces and aluminium, for example, may need treatment suited to their particular chemistry rather than a process intended for mild steel.
4. Powder application
Powder is applied using a spray gun that gives the particles an electrostatic charge. The earthed metal component attracts the charged powder, allowing it to form an even layer over accessible surfaces. Operators control gun distance, movement, powder output and voltage to achieve the specified coverage.
Component geometry affects how powder behaves. Recesses, internal corners and closely spaced sections can experience the Faraday cage effect, where the electrostatic field makes it harder for powder to reach the deepest areas. Application technique may need to be adjusted in these locations, while excessive powder at edges or corners may lead to runs, uneven texture or poor appearance after curing.
Film thickness is controlled according to the coating specification. Too little powder can reduce coverage and protection; too much can affect appearance, fit, flexibility or curing behaviour. In batch work, consistent racking, gun settings and part orientation help reduce variation between components.
5. Oven curing
Once coated, the component enters a curing oven. Heat causes the powder to melt, flow and chemically cross-link, changing it from a loose layer into a continuous solid coating. The required cure is determined by the powder formulation and the actual temperature reached by the metal, not simply by the oven air temperature.
Parts therefore need sufficient time at the required metal temperature. Under-curing can leave the coating weaker or less resistant to chemicals and impact, while excessive heat or dwell time can affect colour, gloss and coating performance. Component mass, shape, rack loading and oven airflow all influence heat transfer, so the process must be suitable for the particular batch rather than judged only by the oven setting.
Some systems involve more than one coating layer. In that case, the sequence may include an initial application and cure, followed by further preparation or application in accordance with the coating manufacturer’s technical requirements. The layers must be compatible and correctly cured to function as a system.
6. Inspection, testing and handling
After curing, the finish is checked once the parts have cooled sufficiently for safe handling and accurate assessment. Visual inspection looks for incomplete coverage, pinholes, craters, contamination, runs, uneven texture, colour variation, excessive orange peel and damage around contact points.
Depending on the specification, further checks may include coating thickness measurement, adhesion testing, colour comparison, gloss assessment, cure verification and dimensional inspection of masked or close-tolerance areas. Threads, mating faces and apertures should be checked because unwanted coating in these locations can affect assembly.
Any repair or rework should be considered against the original specification. Small defects may be treatable using an approved method, whereas widespread contamination, poor preparation or incorrect curing may require the coating to be removed and the component processed again. Finally, finished parts should be protected during handling, stacking and transport so that the new coating is not chipped, scratched or contaminated before installation.
In practice, the process is successful when preparation, application and curing are treated as connected controls rather than isolated tasks. The correct powder cannot compensate for contamination, and careful spraying cannot correct an unsuitable cure or damaged substrate. A clear specification and documented checks at each control point are therefore important for repeatable industrial results.
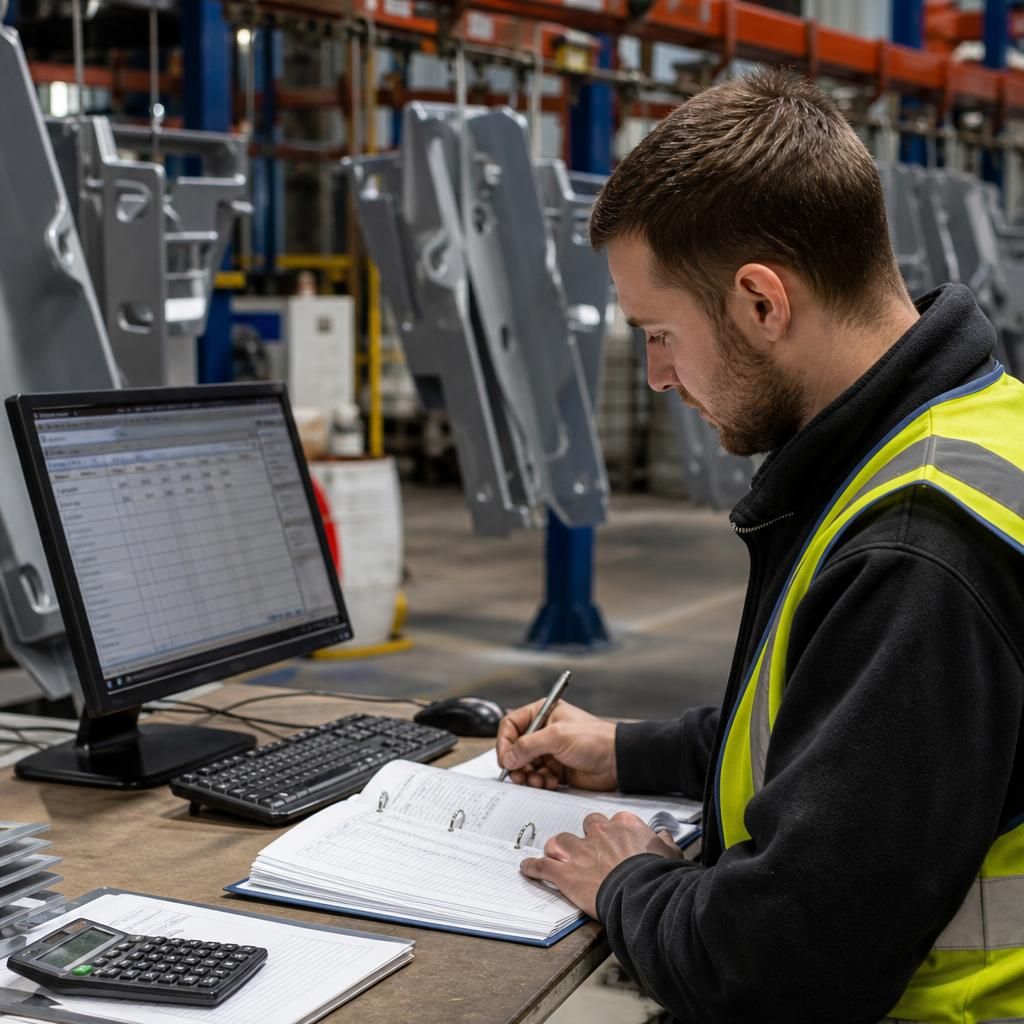
Process records link the individual stages into a repeatable powder coating system. A job record can identify the substrate, preparation method, powder specification, masking requirements, application settings, curing conditions and inspection results. This gives the operator a reference for processing subsequent batches to the same requirements.
Traceability is also useful when a finish does not meet specification. Comparing preparation, application and curing records can help determine whether the cause relates to contamination, film build, oven performance or handling. For manufactured components, retaining these records supports consistent production and provides evidence that the agreed coating requirements were checked at each relevant stage.