

What factors should be considered when determining the thickness and application method for nylon and protective coatings on metal components?
The required coating thickness and application method depend on the component’s material, shape, dimensions, intended use and exposure to abrasion, chemicals, moisture and temperature. Nylon and protective coatings should be specified with the required performance, surface preparation, curing requirements and production volume in mind, then confirmed through an application assessment.
Coating thickness and application method should be set by the required functional performance and the component’s tolerances, geometry and production process. The correct specification is not necessarily the thickest possible film: excessive build can affect fit, moving clearances, threads, apertures and the coating’s ability to bond and cure consistently.
Start with the component’s functional requirements
Separate the areas that need protection from those that must remain dimensionally precise. A nylon coating may be selected where the component needs a tough, resilient surface with resistance to wear, impact or friction. A protective coating may instead be specified primarily as a barrier against corrosion, moisture, chemicals or other service conditions. These requirements influence both the target film build and whether a single coating or a defined multi-coat system is appropriate.
Drawings and specifications should identify critical dimensions, allowable coating build, contact faces, mating surfaces, threaded sections, bores and areas requiring masking. If the finished component must fit another part, the coating allowance needs to be included before application rather than treated as an afterthought.
Consider how geometry affects film distribution
Edges, corners, recesses, holes and enclosed sections do not receive coating in the same way as broad, accessible faces. Sharp edges can produce a thinner film, while recesses and internal features may be difficult to reach or inspect. Deep cavities can also create problems with drainage, trapped pre-treatment chemicals or incomplete curing.
Parts should therefore be reviewed for racking and access before the process is chosen. The hanging position, contact points and orientation can affect coverage and may leave small uncoated areas that need to be positioned away from the service-critical zones. Where edge coverage is important, edge preparation and a suitable coating system may be more effective than simply specifying a heavier overall film.
Match the method to the coating material
Nylon is commonly applied as a thermoplastic coating. The process may involve heating the prepared component and applying nylon powder, or another controlled method suited to the specified material and part. The component must reach the appropriate process condition for the nylon to form a continuous film without degrading, sagging or producing an uneven surface.
Protective coatings may use different application principles, including powder application or liquid systems, depending on the product specification and the component. The selected method affects transfer efficiency, access to difficult areas, achievable finish, overspray control and the way the coating is cured. A method that works well for a flat, open fabrication may be unsuitable for a small part with internal features or a heavy component with significant thermal mass.
Account for substrate and surface condition
Coating thickness cannot compensate for poor adhesion or contamination. Rust, mill scale, oil, weld residue, sharp burrs and embedded particles can create defects beneath the film. Surface preparation should produce a clean, suitably profiled surface and remove features likely to cause pinholes, lifting or premature failure.
The condition of welds and fabricated joints deserves particular attention. Spatter, tight crevices and unsealed joints can interfere with cleaning and may retain contaminants. Where the coating is intended to provide corrosion protection, the specification should address these details before the component reaches the applicator.
Set a controlled thickness range
A target range is more useful than an informal instruction such as “apply a heavy coat”. The range should reflect the coating manufacturer’s technical requirements, the component’s tolerances and the service duty. The lower limit must provide continuous coverage and the required barrier or wear performance; the upper limit must avoid brittleness, cracking, poor flow, excessive build-up and dimensional interference.
Different zones may require different controls. For example, a broad exposed face may accept the normal specified build, while a masked bearing surface or threaded feature may require strict exclusion. If local reinforcement or extra protection is needed, this should be defined as part of the design rather than created through uncontrolled reworking.
Plan masking, racking and post-coating operations
Masking protects threads, electrical contact points, machined faces and other areas that must remain free of coating. Masking materials must withstand the application and curing conditions without leaving residue or damaging the finish. Racking should provide secure support while minimising contact marks and maintaining access to the required surfaces.
Post-coating operations can also influence the specification. If machining, drilling or assembly follows coating, the likely effect on the protective barrier and exposed edges should be assessed. Components that cannot be touched up reliably may need a different masking plan or application sequence.
Validate the process rather than relying on nominal settings
Trial pieces or representative production components can confirm whether the proposed method reaches the required areas and produces a consistent film. Checks may include dry-film thickness measurements at defined locations, visual inspection for pinholes and runs, adhesion assessment and dimensional verification on mating features. The inspection method should be suitable for the substrate and coating system, and measurements should be taken from repeatable points.
Process records should identify the coating material, preparation method, application settings, curing conditions, masking arrangement and inspection results. If the component design, batch size, coating material or process changes, the specification may need to be reviewed rather than carried forward automatically.
For B2B projects, the most useful starting information is a current drawing, the required coating system, critical dimensions, areas to be masked, service conditions and any inspection or traceability requirements. This allows thickness and application decisions to be assessed against the component’s actual function instead of selecting a nominal coating build in isolation.
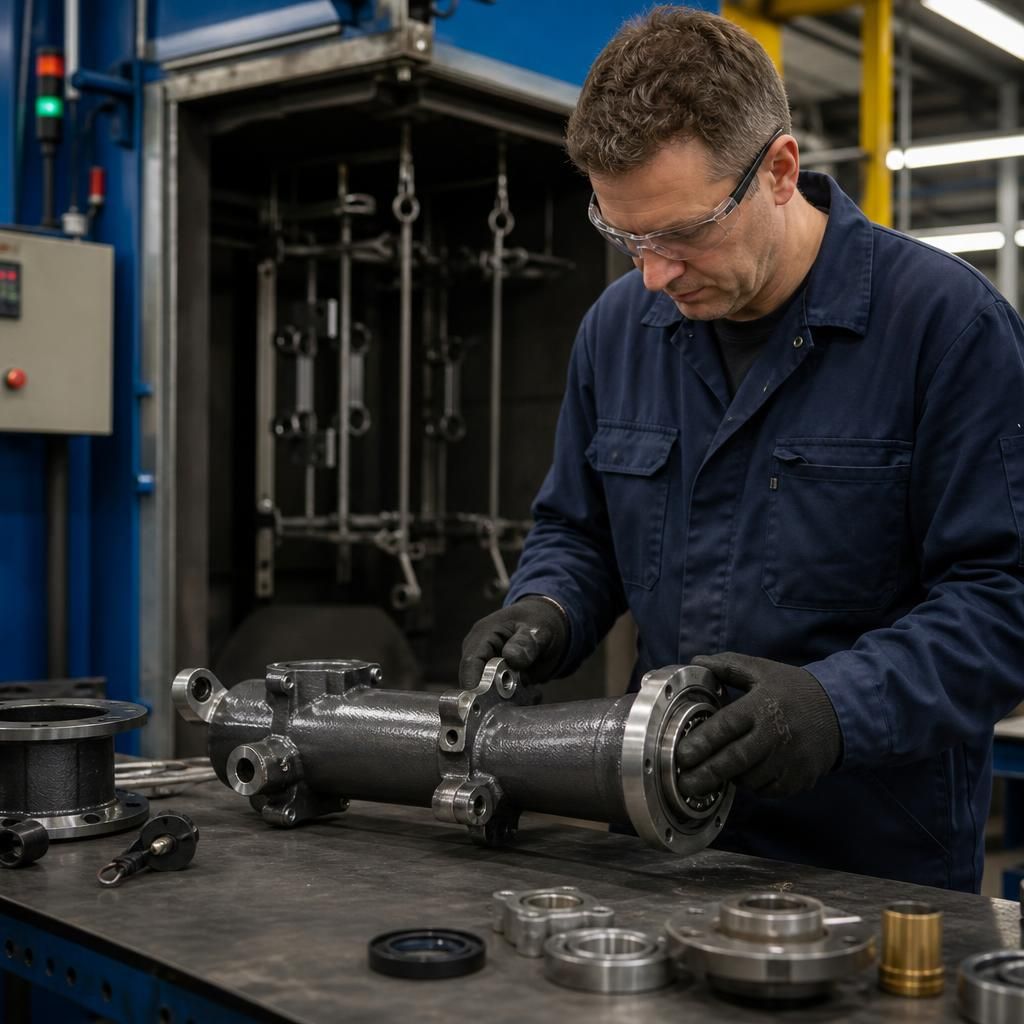
Check heat sensitivity before selecting the application method. Nylon coatings normally require the component to reach a controlled temperature, so the specification should identify any heat-sensitive inserts, seals, bearings, electrical parts or adjoining materials. These items may need to be removed before coating or protected through an alternative process arrangement.
For assembled components, confirm whether disassembly is practical and whether heating could alter dimensions, lubrication or material properties. This assessment can determine whether a thermoplastic nylon process is suitable or whether a different protective coating system should be considered.