

How important is pretreatment in the powder coating process, and what key steps must be taken to ensure its effectiveness in preventing failures?
Pretreatment is essential because it removes contaminants and conditions the metal surface so powder coating can bond properly and resist corrosion, peeling and other failures. Effective preparation requires thorough degreasing, rinsing, suitable chemical conversion or protective treatment, contamination-free handling and complete drying before powder application.
Pretreatment is a controlled process for creating a chemically suitable, stable interface between the metal and the powder coating. Its effectiveness depends not only on the treatment chemicals used, but also on selecting the correct process for the substrate, controlling each stage, and verifying the resulting surface before coating. A pretreatment system that is poorly matched to the metal or allowed to drift out of control can leave the coating vulnerable to underfilm corrosion, blistering, edge breakdown and loss of adhesion.
1. Identify the substrate and the service requirement
Steel, galvanised steel, aluminium and mixed-metal assemblies do not respond identically to pretreatment. The process should therefore be selected according to the alloy, the condition of the surface, the intended environment and the required durability. Galvanised material may need treatment that manages the zinc surface without damaging its protective layer, while aluminium requires chemistry suited to its oxide layer. If different metals are processed together, compatibility and cross-contamination risks must be considered.
The required performance should also be established before production begins. Indoor components, exterior fabrications and parts exposed to moisture, salts or industrial contaminants may need different levels of preparation and conversion protection. The specification should define acceptable surface condition, treatment type, coating system and any test requirements rather than leaving these decisions to the coating stage.
2. Account for fabrication details
Coating failures frequently begin in areas that are difficult for the pretreatment process to reach. Weld seams, lap joints, folded sections, drilled holes, recesses and sharp edges can retain fabrication residues or treatment liquid. These areas may also dry differently from open faces, creating localised corrosion or inconsistent coating performance.
Fabrication design should allow liquid to drain freely and should avoid sealed cavities that can trap rinse water or chemicals. Weld spatter, excessive weld discolouration, burrs, sharp corners and embedded abrasive particles should be addressed before the part enters the treatment line. Where a design cannot be changed, the preparation method and inspection plan should specifically include those vulnerable locations.
3. Control the process rather than relying on appearance
A part can look clean while still carrying residues or having an unsuitable surface chemistry. Pretreatment baths should therefore be monitored against the supplier’s operating requirements, including concentration, temperature, contact time and contamination levels. These factors interact: a reduced chemical concentration, inadequate temperature or insufficient contact can prevent the intended reaction even when the process appears to be running normally.
Rinse stages require equal attention. Carry-over from one stage into another can alter the chemistry, while accumulated salts or other residues in rinse water can be deposited back onto the metal. Water quality, flow, replenishment and drainage should be checked as part of routine process control. Treatment tanks and associated equipment also need cleaning so that sludge and built-up residues do not become a source of recontamination.
4. Confirm that the conversion layer is consistent
Where a chemical conversion treatment is specified, the objective is a uniform, adherent layer that improves the bond between the metal and the coating and provides additional protection at the interface. Excessive treatment is not automatically better: an unsuitable or uneven layer can create its own adhesion and corrosion problems.
Verification may include visual checks, control panels, chemical analysis and periodic performance testing, depending on the process and the required specification. A consistent appearance across the full component is useful, but it should not be the only acceptance criterion. Areas around welds, edges, recesses and joints deserve particular attention because treatment coverage may vary there.
5. Prevent damage between pretreatment and coating
Once the surface has been prepared, the parts should be protected from dust, moisture, fingerprints, oil and contact with unsuitable surfaces. Handling fixtures and conveyor points should be kept clean, and operators should avoid touching critical faces with bare hands. Parts should be moved through the remaining process without unnecessary delay or exposure to conditions that could cause oxidation or contamination.
Drying is also a process-control issue, not simply a final visual check. Water retained in holes, joints and recessed features can interfere with coating application and may later contribute to corrosion. Drying conditions should be sufficient for the geometry and material, with particular checks on areas where liquid can collect. Any sign of flash rust, staining or recontamination should trigger assessment and, where necessary, reprocessing rather than allowing the part to proceed.
6. Use inspection and testing to detect weaknesses
Pretreatment effectiveness should be assessed alongside the finished coating, not only after a failure has occurred. Useful controls can include surface cleanliness checks, coating adhesion testing, corrosion-resistance testing and inspection of cut edges or deliberately stressed test panels. The appropriate method depends on the coating specification and the conditions in which the component will be used.
When a defect appears, its location and pattern can help identify a pretreatment problem. Widespread blistering may indicate inadequate process control or residual contamination; isolated defects around joints can point to drainage or fabrication issues; and early edge corrosion may suggest insufficient preparation or weak coverage at vulnerable geometry. Comparing results with process records helps distinguish pretreatment faults from powder, curing or application problems.
7. Maintain traceability and corrective action
Records should show the substrate, treatment route, bath checks, rinse condition, inspection results and any deviations from the approved process. This makes it possible to identify trends before they become widespread failures. If a control value moves outside its permitted range, the cause should be investigated and affected parts assessed. Simply adjusting the bath without checking previously processed components can leave non-conforming work in the production flow.
In practice, effective pretreatment is achieved through a documented, substrate-specific process with controlled chemistry, sound component design, disciplined handling and objective verification. These measures reduce the risk that a powder coating will be asked to compensate for a surface that was not properly prepared in the first place.
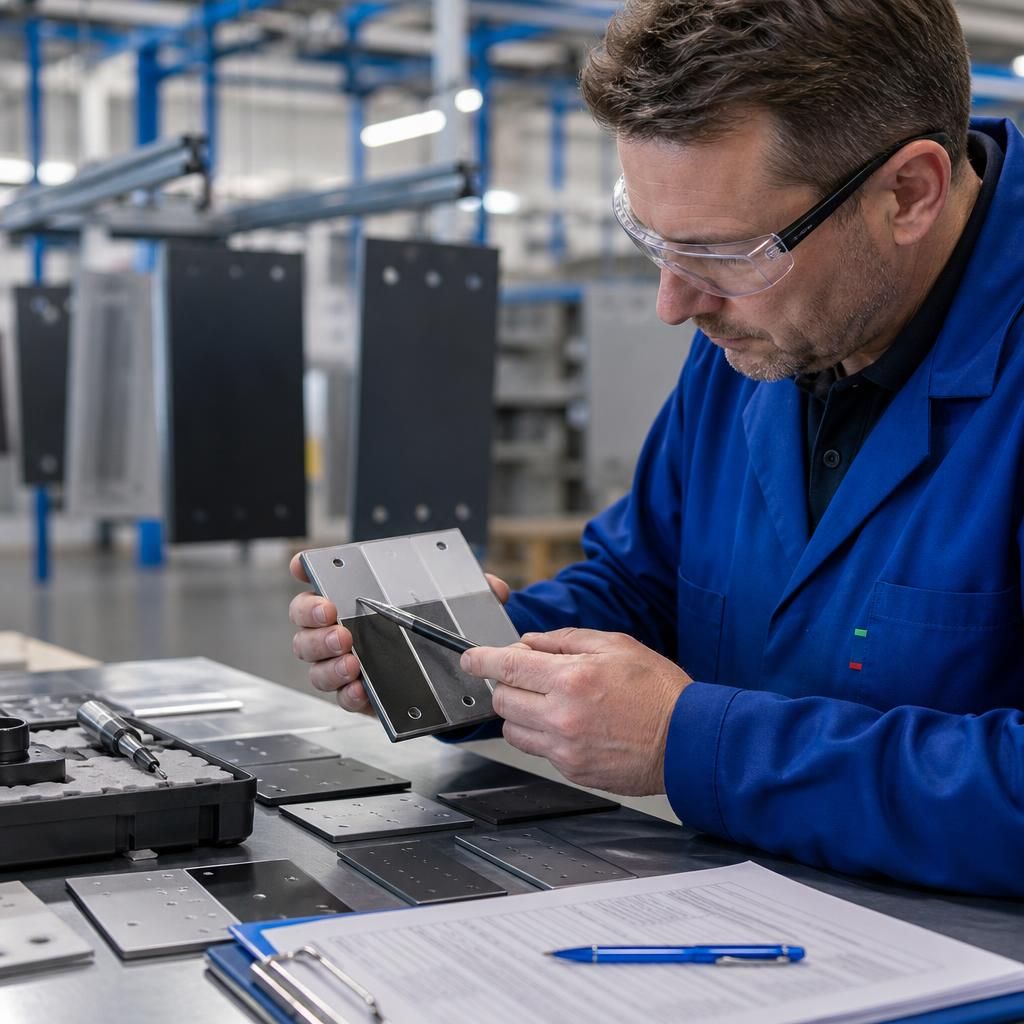
Pretreatment effectiveness should be revalidated whenever the process or the parts change. Introducing a different alloy, coating system, chemical supplier, line speed or component design can alter how the surface responds, even when the equipment settings appear unchanged.
Use representative test pieces or control panels to confirm that the revised process produces the required surface condition before full production begins. Assessment may include adhesion and corrosion testing, with particular attention to welds, edges, recesses and other features that behave differently from flat panels. This change-control approach helps identify incompatibility before it becomes a repeated production failure.