

How do thermoplastic powder coatings compare in terms of environmental sustainability and recyclability compared to other coating options?
Thermoplastic powder coatings can offer sustainability advantages because they contain no curing solvents, can achieve low-waste application through powder recovery, and may be softened and reprocessed rather than permanently cross-linked. Their recyclability is generally more favourable than thermoset powders and many liquid coatings, although the real environmental impact depends on the polymer type, additives, energy used during application, service life and how the coated component is separated and processed at end of life.
Thermoplastic powder coatings can have a favourable environmental profile, particularly where their long service life, repairability and potential for material recovery outweigh the impacts of producing and applying the polymer. They are not automatically the most sustainable option: the result depends on the coating chemistry, film thickness, preparation method, operating conditions and what happens to the coated component at the end of its life.
Comparison with thermoset powder coatings
The main distinction is what happens after heating. Thermoplastic powders melt and form a film without creating an irreversible cross-linked structure. With suitable equipment and controlled conditions, production overspray or clean surplus material may therefore be easier to handle as a material stream. A thermoset powder, by contrast, undergoes a chemical curing reaction. Once cured, it cannot simply be melted back into a powder that performs like the original coating.
This does not mean a thermoplastic-coated part can always be recycled without preparation. The coating may contain pigments, fillers, stabilisers or reinforcing ingredients, and it may be firmly bonded to steel, aluminium or another substrate. If the metal is recycled, the coating normally has to be tolerated by, removed during or managed within the recycling process. In practice, the ease of recovery depends on the part’s design, the coating thickness and the capability of the waste processor.
Thermoset powders can nevertheless be the better environmental choice for some applications. A coating that remains intact for longer, withstands chemicals more effectively or protects a component in a particularly demanding environment may avoid replacement, repair and repeated recoating. Sustainability should therefore be assessed across the working life of the asset rather than by comparing powder chemistry alone.
Comparison with liquid coatings
Many conventional liquid coatings use organic solvents to keep resins and pigments in a spreadable form. Those solvents can contribute to volatile organic compound emissions during application and drying. Powder systems avoid that particular solvent carrier, although their manufacture, storage, application and heating still require resources and energy. Water-based liquid coatings can reduce solvent-related impacts, so the comparison is not simply powder versus all liquid products.
Liquid coatings may also be advantageous where a very thin film, on-site touch-up or application to heat-sensitive materials is required. Using a coating system that needs less material or avoids heating a large component can reduce the total environmental burden. Conversely, a durable thermoplastic finish may reduce future stripping and recoating where the component is exposed to abrasion, impact, moisture or corrosive conditions.
Why durability matters
Service life is one of the most important sustainability factors. Manufacturing a replacement metal component, transporting it and preparing it for coating can have a greater impact than the original coating application. A finish that retains its protective function and appearance for the intended duty can extend the useful life of the underlying part and reduce the frequency of intervention.
Durability must be matched to the application rather than assumed from the word “thermoplastic”. Different polymers vary in resistance to ultraviolet exposure, chemicals, abrasion, impact, temperature and moisture. A coating selected for the wrong environment may deteriorate early, making its theoretical recyclability less significant. Specification should consider the actual exposure conditions, required film performance and expected maintenance method.
Energy and process considerations
Thermoplastic powder application generally requires the powder to soften and flow on the component. The energy demand is influenced by the metal’s size, mass, geometry, required temperature, line configuration and production volume. Heating a heavy assembly or repeatedly reheating a part can change the environmental balance compared with a coating that cures at a lower process temperature.
Preparation also matters. Degreasing, blasting, chemical treatment and rinsing may consume water, energy and treatment chemicals. A coating should not be assessed independently from these stages. Good process control can reduce rejects, unnecessary stripping and repeat preparation, while suitable part design can make cleaning, coating and eventual separation more straightforward.
Recyclability at the end of life
There are two separate questions: whether the coating itself can be remelted, and whether the complete coated article can enter an established recycling route. A thermoplastic film may be softened or reprocessed in controlled industrial conditions, but that does not guarantee that household, commercial or metal-recycling facilities will accept it as a separate recyclable material.
Coated metal is commonly managed according to the value and recovery route of the substrate. In some processes, the coating is removed or separated; in others, small quantities are managed as part of the overall scrap stream. Mixed polymers, bonded inserts, labels, oils and other contaminants can make separation more difficult. Designing components for disassembly, identifying the coating chemistry and keeping different materials separate can improve the prospects for recovery.
Recycling is also affected by colour and formulation. A mixed stream of several thermoplastic chemistries may not produce a consistent secondary material, while pigments and additives can limit where recovered material is suitable for use. For this reason, reuse, controlled industrial recovery and substrate recycling should be considered separately rather than treated as one universal route.
How to make a meaningful comparison
- Compare the expected service life and failure mode of each coating system, not just its application method.
- Include surface preparation, heating, transport, maintenance and likely recoating in the assessment.
- Check whether the coating is appropriate for the component’s chemical, mechanical, thermal and outdoor exposure.
- Ask how production waste, rejected parts and removed coatings will be handled.
- Consider whether the coated article can be dismantled and whether its metal substrate has a practical recovery route.
- Use product-specific environmental information where available, such as technical data, safety information and life-cycle assessment results, rather than relying on broad claims about powder coatings.
Overall, thermoplastic powder coatings are often strongest from a sustainability perspective when they provide long protection, avoid frequent refurbishment and fit a controlled recovery process. Thermoset powders and liquid coatings may be preferable where their performance, lower process demand or established end-of-life route delivers a better whole-life result. The soundest choice is therefore the coating that meets the technical specification with the least material, energy and maintenance burden over the complete life of the component.
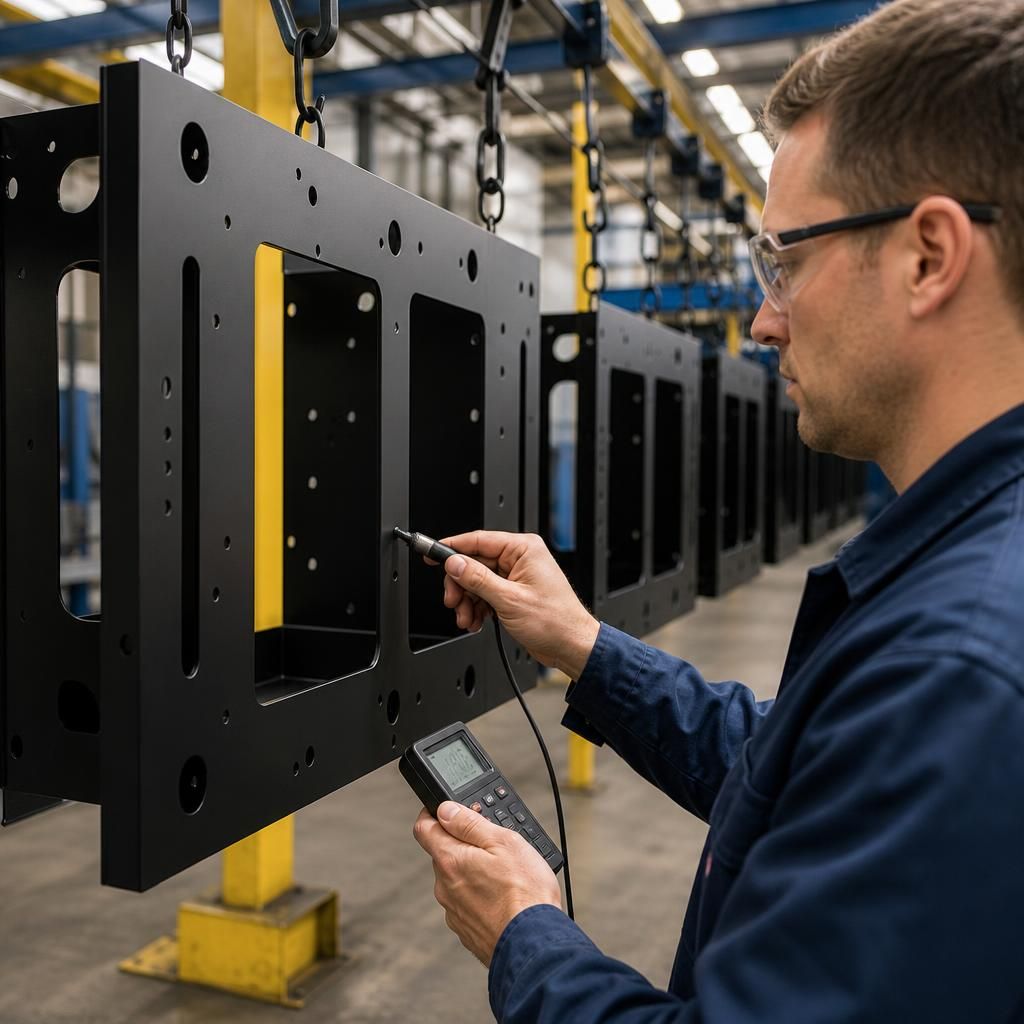
Coating thickness is a practical factor in the environmental performance of a thermoplastic powder coating. The film should be thick enough to provide the specified protection, but applying more material than the component requires increases polymer use and may require additional heating or rework.
Thickness should therefore be controlled according to the service conditions, substrate profile and performance requirements. Consistent application helps avoid thin areas that fail prematurely and thick areas that waste material or affect the finish. The most sustainable specification is not necessarily the thinnest coating, but the one that achieves the required protection with minimal excess and remains suitable for the component’s intended working life.