

What are the environmental considerations and benefits of choosing nylon and speciality powder coatings for sustainable manufacturing processes?
Nylon and speciality powder coatings can support more sustainable manufacturing by producing durable finishes with little or no solvent use, while reducing recoating, material waste and maintenance over a component’s service life. Environmental assessment should also consider curing energy, powder recovery, pre-treatment chemicals and end-of-life recycling, as the most suitable coating depends on the part, performance requirements and application process.
Nylon and speciality powder coatings can support sustainable manufacturing when the complete coating process is assessed rather than judged by the coating material alone. The relevant considerations include raw material selection, application efficiency, curing or melting energy, pre-treatment, overspray handling, part design, service conditions and end-of-life treatment. Nylon coatings are thermoplastic finishes, while “speciality” powder coatings may be formulated for properties such as chemical resistance, electrical insulation, low friction, UV resistance or enhanced corrosion protection. Their environmental performance therefore depends on the specific formulation and how it is applied.
Material efficiency during application
Powder is supplied as a dry solid and can be applied in a controlled layer rather than being carried in a liquid solvent. This allows the coating process to avoid the solvent evaporation stage associated with many liquid systems. Unused powder may also be collected where the equipment and coating specification permit, although recovered material must be managed carefully to prevent colour, resin or performance contamination. Powder that cannot be returned to the process should be segregated and handled through an appropriate waste route.
Application control is important because excessive coating thickness uses more material and can affect the finished component. Correct earthing, gun settings, part positioning and rack design can improve transfer to the workpiece. For nylon coatings, the selected application method and melt-flow behaviour must also be matched to the component geometry. Recesses, sharp edges and complex shapes may require different process controls from flat or regularly shaped parts.
Energy use and process selection
Powder coating is not automatically low impact: the finish normally requires heat to melt, flow or cure. Nylon coatings are commonly processed as thermoplastic powders, so the required heating profile may differ from that of thermosetting powders. Speciality formulations can have their own temperature and dwell-time requirements. The most responsible choice is therefore the lowest-energy process that achieves the necessary film formation and performance, rather than selecting a coating solely because it is powder-based.
Energy use can be reduced through suitable oven loading, effective insulation, accurate temperature control and avoiding unnecessary heating of empty space. Parts should be arranged to allow consistent airflow and heat transfer, reducing the risk of rejected work caused by under-processing or overheating. Where a component can be coated in a single controlled pass instead of requiring repeated processing, this may also reduce process energy and material consumption, provided the required specification is met.
Pre-treatment and water management
Pre-treatment removes oil, oxides, scale and other contaminants so that the coating can form a reliable bond. Its environmental profile depends on the chemicals used, the cleaning method, bath management and how waste water or spent solution is controlled. A process using aggressive chemistry is not necessarily more sustainable if it creates avoidable hazardous waste or requires excessive rinsing.
Manufacturers should consider whether mechanical preparation, a lower-impact chemical system or a reduced-rinse process is suitable for the substrate and service environment. This decision must not compromise adhesion or corrosion protection. Pre-treatment waste should be stored, tested and disposed of in accordance with the relevant UK requirements; it should not be discharged without suitable control. Substrate type, contamination level and the intended duty of the component all influence the appropriate preparation route.
Durability as a lifecycle consideration
A coating with the right resistance for its operating environment can reduce the environmental burden associated with premature component replacement. The relevant property may be resistance to abrasion, impact, chemicals, moisture, outdoor exposure, heat or electrical conditions. Nylon is often considered where a tough, low-friction or wear-resistant surface is required, while other speciality powders may be selected for a more specific operating demand.
This benefit should be assessed against the actual duty of the part. Applying a highly specialised coating where a simpler finish would perform adequately can introduce unnecessary material and process requirements. Conversely, using an unsuitable coating may lead to early damage, stripping and recoating. A lifecycle comparison should therefore include expected operating conditions, cleaning regime, contact with chemicals, exposure to sunlight and the consequences of coating failure.
Waste prevention and quality control
Defects such as poor adhesion, pinholing, contamination, uneven coverage and incorrect colour can result in additional preparation and processing. Good process control is consequently an environmental measure as well as a quality measure. Clear specifications should identify the substrate, required film build, appearance, performance properties and inspection criteria before production begins.
Batch size, component geometry and the number of colours or coating types being processed can affect changeover waste. Grouping compatible work and planning coating sequences can limit cleaning and purge material, although this must be balanced against production requirements. Protective handling and suitable packaging can also prevent damage after coating, avoiding waste caused by transit or storage defects.
Recycling and end-of-life planning
Powder-coated metal components can generally enter established metal recycling streams, but the exact route depends on the substrate, the coating system and the recycler’s requirements. The coating should not be described as automatically recyclable simply because the underlying metal is recyclable. Mixed-material assemblies, bonded inserts, rubber components and heavy contamination may complicate separation or processing.
Designing components for disassembly can improve end-of-life recovery. Where practical, manufacturers should identify the substrate and coating system in technical records, avoid unnecessary combinations of inseparable materials and ask the intended recycling route whether any restrictions apply. Coating removal may be possible in some industrial situations, but it uses additional energy, chemicals or mechanical processing and should not be assumed to be the preferred option.
How to compare coating options responsibly
- Define the performance needed for the component and avoid specifying properties that will not be used.
- Compare the complete process, including preparation, application, heating, inspection, rework and waste handling.
- Check whether the powder can be applied efficiently to the part geometry and whether overspray can be managed appropriately.
- Consider the energy source and oven utilisation rather than looking only at the coating formulation.
- Review chemical use, water consumption and waste controls in the pre-treatment stage.
- Assess expected service conditions and the likely effect of coating failure on replacement or repair.
- Confirm how the finished metal component can be handled at the end of its useful life.
For manufacturers and fabricators, the most credible environmental assessment is a process-specific comparison between suitable coating systems. Nylon or another speciality powder may offer a strong sustainability case where its performance matches the component’s duty and the application process is well controlled. The decision should be supported by technical data, coating specifications and practical information from the applicator, rather than by a general claim that one coating type is environmentally preferable in every situation.
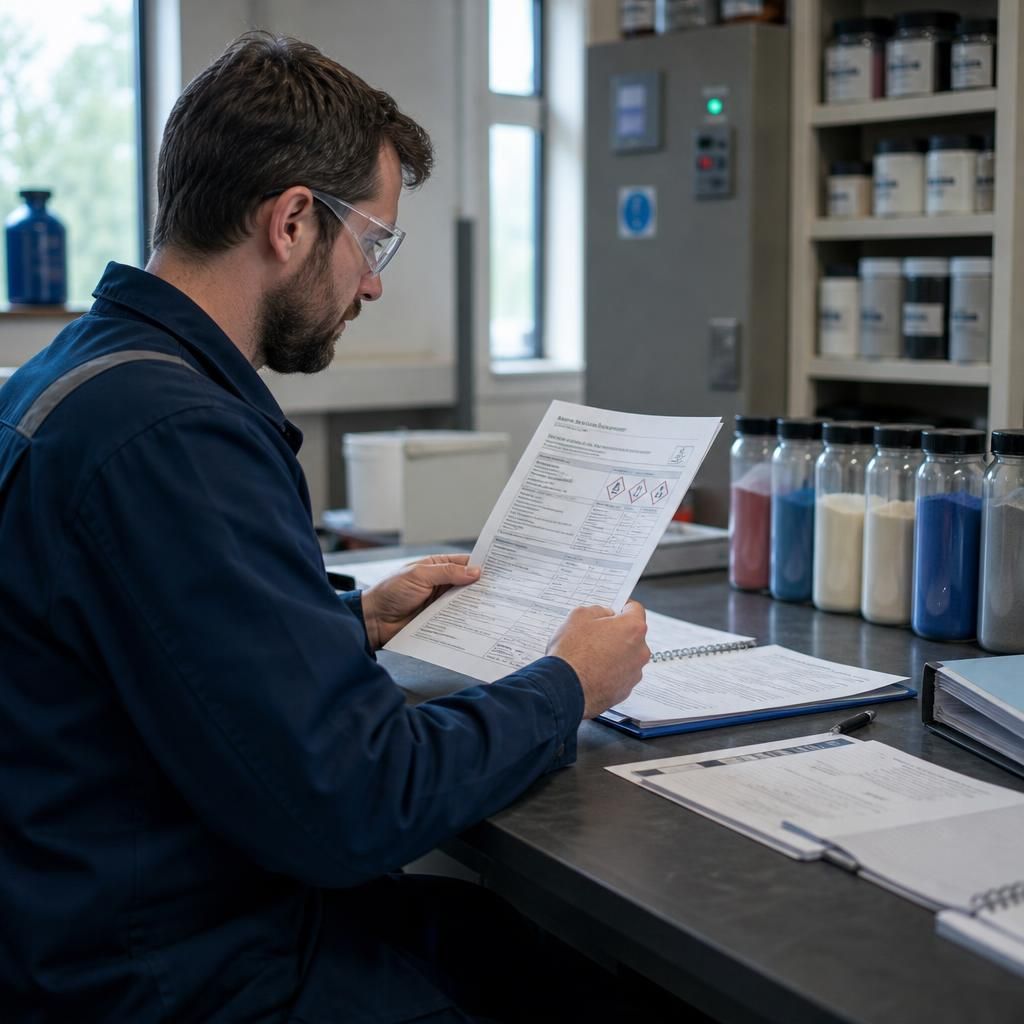
Environmental documentation is essential for comparing nylon and speciality powder coatings because the impact depends on the specific formulation and process, not simply on the word “powder”. A technical review should cover the product’s safety data, recommended application conditions, curing or melting requirements, overspray handling and any restrictions on waste disposal.
Manufacturers should also ask whether the supplier can provide formulation-specific environmental information, such as volatile organic compound data or an environmental product declaration where available. This helps distinguish verified characteristics from broad sustainability claims and allows the coating to be assessed alongside the energy, chemicals and waste generated during application.
Discuss Sustainable Nylon and Speciality Coating Options
Discuss your component’s substrate, operating conditions and required finish with a powder-coating specialist to compare suitable nylon and speciality coating options. Request a process-specific assessment covering application requirements, environmental considerations and end-of-life handling.