

What factors should be considered when scheduling maintenance for nylon and speciality coatings in industrial settings?
Maintenance for nylon and speciality coatings should be scheduled according to operating conditions, exposure to chemicals or abrasion, component criticality and inspection findings rather than a fixed interval alone. Planned access, cleaning requirements and the time needed for coating repair or reapplication should also be coordinated to minimise disruption to production.
Maintenance scheduling for nylon and speciality coatings is a documented plan for preserving the coating system, the underlying metal and the component’s intended function. It should define what is inspected, how condition is assessed, which maintenance actions are permitted and what evidence is required before the component returns to service.
Start with a coating and component register. Each asset record should identify the substrate, coating type, application date, colour, nominal coating thickness where known, curing requirements, service location and any previous repairs. Include design features that may affect maintenance, such as sharp edges, threaded sections, moving interfaces, drainage points, welds, joints and areas concealed by brackets or fixings. This information prevents a generic maintenance instruction being applied to coatings with different properties or limitations.
A baseline condition assessment is useful after installation or initial commissioning. Record the coating’s appearance, adhesion assessment where appropriate, surface finish, dimensions at critical interfaces and the condition of adjacent metalwork. Photographs and marked-up drawings can help identify gradual changes. The baseline should also state the acceptable condition for continued service, rather than relying solely on an inspector’s general judgement. For example, a small cosmetic change may be acceptable on a non-critical enclosure but not where coating integrity affects a sealed joint, electrical isolation or a close-fitting component.
Match the inspection method to the coating system. A visual check may identify colour change, gloss loss, staining, pinholes, blisters, cracking, flaking or exposed substrate. Tactile checks can reveal raised edges, roughness or localised loss of adhesion, while dimensional checks are important where the coating sits within a bearing, seal, thread or sliding clearance. Any test method should be selected so that it does not damage an otherwise serviceable nylon coating. Where the condition beneath the coating cannot be confirmed, the inspection plan should define when a more detailed assessment or controlled removal is justified.
Nylon and other speciality coatings should not be treated as interchangeable. The technical data for the specific system may set limits for temperature, solvents, cleaning agents, contact materials, flexibility, electrical performance or permitted repair methods. A nylon coating may remain visually intact while repeated heat exposure, solvent contact or movement has altered its performance. Conversely, a change in colour or gloss does not automatically prove loss of protective function. Scheduling decisions should therefore consider both visible condition and the property that the coating is required to provide.
Separate routine care from corrective work. Routine cleaning should use methods compatible with the coating and the deposited material. The maintenance instruction should specify suitable cleaning fluids, dilution requirements where applicable, cloths or brushes, rinsing and drying procedures, and substances to avoid. Abrasive tools, aggressive solvents and uncontrolled high-pressure cleaning can damage the finish or force contamination into edges and joints. Cleaning records should distinguish removable deposits from defects in the coating itself, so that unnecessary repairs are not scheduled.
Repair criteria should be agreed in advance. Local repair may be suitable when damage is confined, the surrounding coating remains firmly bonded and the substrate is sound. Larger areas of delamination, repeated failure around a joint, corrosion beneath the coating or widespread loss of the required property may require removal and complete reapplication. The repair specification should cover preparation of the exposed metal, treatment of edges, masking, coating compatibility, curing and final inspection. A repair that restores appearance but leaves contamination, weak adhesion or an unsuitable coating transition is not a complete maintenance outcome.
Consider component interfaces and tolerances before taking a part out of service. Coating removal and reapplication can affect dimensions, threads, holes, seals and sliding surfaces. Masking requirements should be recorded before the component is sent for treatment, and critical dimensions should be checked after work is complete. Where components are dismantled, replaceable seals, fasteners and insulating parts may need separate inspection. This is particularly important for assemblies in which the coating forms part of a controlled clearance or prevents contact between dissimilar materials.
Practical scheduling also depends on the work required to access and handle the component. The plan should identify isolation requirements, lifting equipment, protection for nearby parts, contamination controls and the route for sending components away for specialist treatment if necessary. For batch-maintained equipment, grouping compatible parts can simplify identification and inspection, but only if each item remains traceable. Tags, photographs and job records help prevent incorrect masking, mixed coating specifications or the return of an item without its associated inspection information.
Maintenance records should capture the date, asset identity, observed defect, inspection method, cleaning or repair carried out, materials used, coating batch information where available, curing evidence and final acceptance decision. Record the reason for changing the planned task as well. Repeated local repairs, recurring damage at the same interface or a shortening interval between defects may indicate a design, installation or service problem rather than a coating problem alone.
Finally, review the schedule after each significant maintenance event. Compare the latest condition with the baseline, check whether the chosen repair method has remained sound and update the task instructions if the coating system or component has changed. For industrial users, a written schedule supported by coating records, clear acceptance criteria and competent inspection provides a more reliable basis for maintenance decisions than appearance alone.
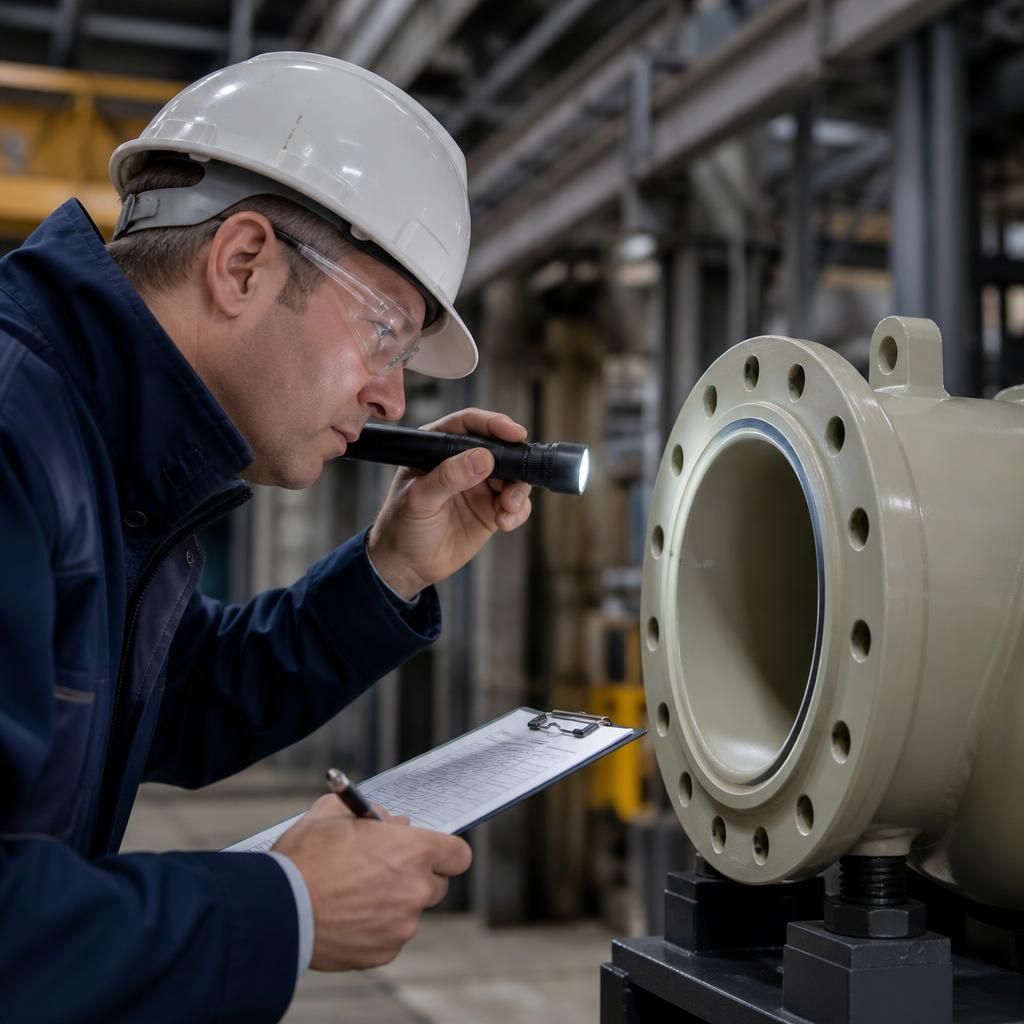
A trigger-based review is a maintenance control that reassesses a nylon or speciality coating after a change or abnormal event, rather than waiting for the next planned inspection. This is important where the component’s exposure may have changed without any visible defect appearing immediately.
Define review triggers such as a new cleaning chemical, process-temperature change, altered operating material, impact, flooding, fire exposure, prolonged contamination or a change in the component’s duty. The review should confirm whether the existing coating remains suitable, whether inspection needs to be brought forward and whether the maintenance instructions require revision. This approach links the schedule to actual service conditions and helps identify coating risks introduced by process changes.
Plan maintenance for nylon and speciality coatings
If you are planning maintenance for nylon or speciality-coated components, discuss the coating specification, service conditions and inspection requirements with a specialist before work is scheduled. Providing details of the component’s use and any known defects helps establish a suitable maintenance or repair approach.