

What considerations are involved in selecting a suitable speciality coating for industrial use?
Selecting a suitable speciality coating for industrial use involves matching the coating’s chemical, mechanical and temperature resistance to the component’s operating environment. Also assess the substrate, required finish, application method, service life, maintenance demands and total lifecycle cost before specifying the system.
A suitable speciality coating is selected by matching the coating system to the component’s function, design constraints and required evidence of performance. The correct choice depends not only on the coating material, but also on how the finished part will be handled, assembled, inspected and used within the wider product or structure.
Start with the component’s function. Identify what the coating must enable or prevent. A coating may be required to reduce friction between moving parts, provide electrical insulation, protect a surface from repeated contact, prevent marking of a mating component, or create a resilient barrier between metal surfaces. These requirements can point towards different coating characteristics, so a general-purpose specification may be unsuitable where the part has a specific functional role.
Consider the interfaces around the coated part as well as the part itself. A coating that performs well on an exposed surface may affect the fit of a thread, bearing seat, hinge, shaft, seal or press-fit assembly. Contact with rubber, plastics, lubricants or other metals should also be assessed. Where coated and uncoated components move against one another, friction, transfer of material and possible noise should form part of the specification.
Check the design before choosing the application route. Large panels, small components, deep recesses and complex fabrications present different coating challenges. Narrow gaps, internal corners, blind holes and enclosed sections can affect powder access and coverage. Threads, machined faces, drain holes, earth points and other areas that must remain free of coating should be identified on the drawing. Masking requirements need to be agreed before production, particularly where tight assembly tolerances apply.
Coating thickness must be considered as part of the component design rather than treated as an afterthought. Build-up on edges, holes and mating faces can change dimensions, while insufficient coverage in difficult areas can reduce the intended protective function. A supplier should be able to discuss critical dimensions, masking locations and inspection points from the component drawing or sample part.
Assess the metal preparation in practical terms. Weld spatter, sharp edges, oil, dirt, previous finishes and embedded contamination can affect the consistency of the result. Fabrications may need edge treatment, cleaning or other preparation before coating. Different substrates and existing surface conditions can require different preparation methods, and a proposed system should be checked for compatibility rather than selected solely by appearance or nominal coating type.
Compare coating systems against the actual specification. Nylon and other speciality coatings can be supplied as part of different system designs, including single-coat arrangements or combinations with a primer or base layer. The selection should account for the required build, adhesion strategy, finish, masking method and curing sequence. A two-coat system may be appropriate where an additional barrier or bonding layer is needed, but it introduces another interface that must be controlled and inspected.
Colour and surface texture should be recorded accurately, but they should not take precedence over functional requirements. Gloss level, texture and colour can influence appearance, cleaning and the visibility of handling marks. If parts are assembled into a larger product, specify whether visual uniformity is required across separate batches and which surfaces are subject to formal acceptance.
Define how suitability will be demonstrated. For a new application, representative trial parts or test panels can help confirm coverage, adhesion, dimensional impact and the suitability of the finish before routine production. Testing should reflect the component’s intended use rather than relying on a generic visual inspection. Depending on the application, the agreed inspection plan may include:
- visual checks for runs, pinholes, bare areas, inclusions and unacceptable surface defects;
- coating thickness checks at defined locations;
- adhesion assessment using an agreed method;
- checks on masked areas, threads, holes and other functional features;
- assembly or movement checks on representative parts; and
- resistance testing where the coating has an electrical, insulation or barrier function.
Any testing should be linked to clear acceptance criteria. Terms such as “good finish” or “fully covered” can produce inconsistent decisions unless the drawing, purchase order or inspection plan defines what is acceptable and which areas are critical.
Consider production control and repeatability. A coating that works on a prototype must also be suitable for the expected batch process. Discuss part orientation, loading, masking, handling points and whether different component sizes will be processed together. Records of the coating specification, preparation requirements, colour or finish reference, inspection results and any approved samples help reduce variation between production batches.
It is also sensible to consider future work at the specification stage. Identify how damaged areas will be treated, whether a repair coating can bond to the original system, and whether components can be recoated without affecting dimensions or assembly. This is particularly important for parts that are difficult to remove, expensive to replace or incorporated into larger equipment.
A specialist coating provider should therefore be able to review the part drawing, intended use, substrate condition, critical dimensions and inspection requirements before recommending a system. Sharing photographs, technical drawings, material details and details of mating components will produce a more reliable assessment than requesting a coating by name alone. The final specification should state the coating system, preparation, masking, finish, critical measurements, inspection method and approval requirements in one controlled document.
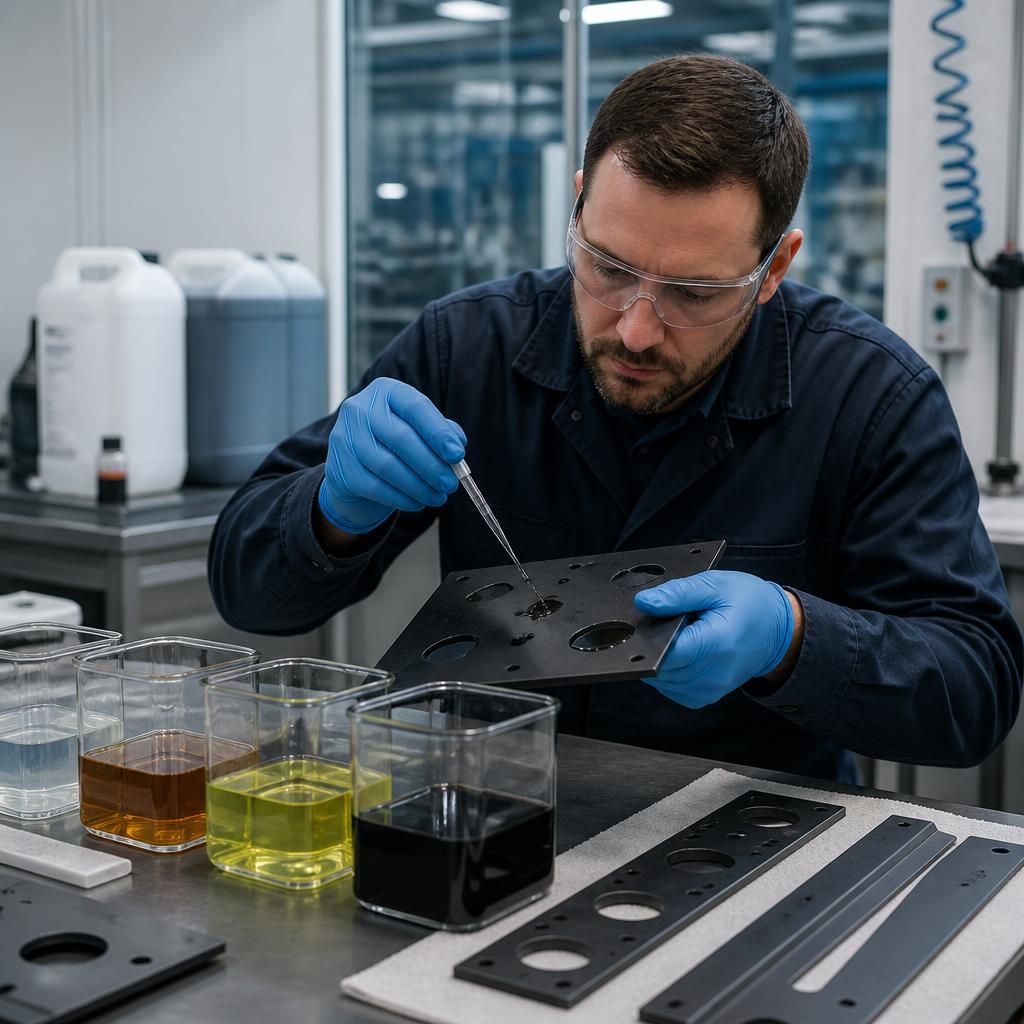
Chemical exposure should be assessed in detail rather than described simply as “chemical resistance”. Identify the substances the component will contact, including process fluids, detergents, oils, fuels and solvents, then record their concentration, temperature, contact frequency and whether exposure involves immersion, splashing or vapour. A coating suitable for occasional contact may not be appropriate for continuous immersion or repeated cleaning.
Use this exposure profile to compare documented compatibility information and, where the service conditions are unusual or critical, consider testing representative coated parts. The assessment should also account for combined stresses, such as chemical contact alongside abrasion, heat or pressure. This helps distinguish a coating that is suitable in isolation from one that is suitable for the component’s actual working environment.