

What maintenance is required for metal components coated with Rilsan Nylon 11 to ensure longevity?
Maintain Rilsan Nylon 11-coated metal components through regular visual inspections, gentle cleaning and prompt attention to chips, cuts, abrasion or exposed metal. Use non-abrasive methods and compatible cleaning products, avoid harsh chemicals and impact where possible, and arrange professional assessment if the coating is damaged or begins to lift.
Rilsan Nylon 11-coated metal components require a planned maintenance regime rather than routine recoating. The essential approach is to control the conditions that can shorten coating life, keep a record of the coating’s condition and service environment, and deal with changes before they affect the underlying metal.
Maintenance planning should take account of the component’s exposure to moisture, chemicals, heat, sunlight, movement and contact with other parts. The inspection frequency should reflect that risk: equipment exposed to abrasive materials, outdoor conditions or aggressive chemicals needs closer attention than components operating in a clean, sheltered environment. Keep the original coating specification and any available application information with the asset record, as this helps determine suitable cleaning products and repair methods later.
- Control handling damage: use suitable lifting points and protective packing when moving coated parts. Avoid dragging components across hard surfaces or allowing them to strike one another during storage and installation.
- Protect the coating during nearby work: shield coated areas from welding spatter, grinding debris, sharp tools and hot work. Metal swarf or abrasive dust should not be allowed to remain trapped against the surface.
- Manage contact points: review brackets, clamps, fasteners and supports that may rub against the coating or concentrate loads at an edge. Where practical, use compatible separators or adjust the assembly to prevent repeated friction.
- Prevent standing moisture: check that the component’s orientation, drainage paths and surrounding fittings do not create pockets where water or contaminants can remain against the coating.
Chemical exposure should be managed against the actual operating environment, not against a general assumption that nylon is resistant to every substance. Keep a record of process chemicals, cleaning agents, oils and solvents that may contact the component. If a new substance is introduced, confirm its compatibility with the specific Rilsan Nylon 11 system before use. Concentration, temperature, contact time and repeated exposure can all affect the result.
Operating conditions should also remain within the limits established for the particular coating specification. Unexpected heating, repeated impact, vibration or abrasive contact may indicate that the component is being used differently from the conditions considered during coating selection. In that situation, review the application rather than simply increasing the maintenance frequency.
Inspection records should identify the component, date, service conditions and any change from its previous condition. Pay particular attention to edges, holes, bends, joints, mounting points and areas subject to repeated movement, since these locations are more likely to experience mechanical stress. Record the extent and location of any defect so that deterioration can be compared over time and repair work can be prioritised.
Repairs should use a method compatible with the existing coating and the service environment. Local preparation, edge treatment and curing requirements are important; an unsuitable touch-up product can create a weak boundary or interfere with the surrounding finish. Where the coating has separated from the metal, damage is extensive or corrosion is suspected beneath the finish, the component should be assessed by a powder-coating specialist before it is returned to service. A repair may require more extensive preparation or complete recoating rather than a superficial patch.
For larger equipment fleets or production batches, a written maintenance procedure is useful. It should define approved cleaning materials, handling controls, inspection criteria, chemical restrictions, documentation requirements and the point at which specialist assessment is required. This prevents different operators from applying inconsistent methods and helps preserve the protective function of the Rilsan Nylon 11 coating throughout the component’s working life.
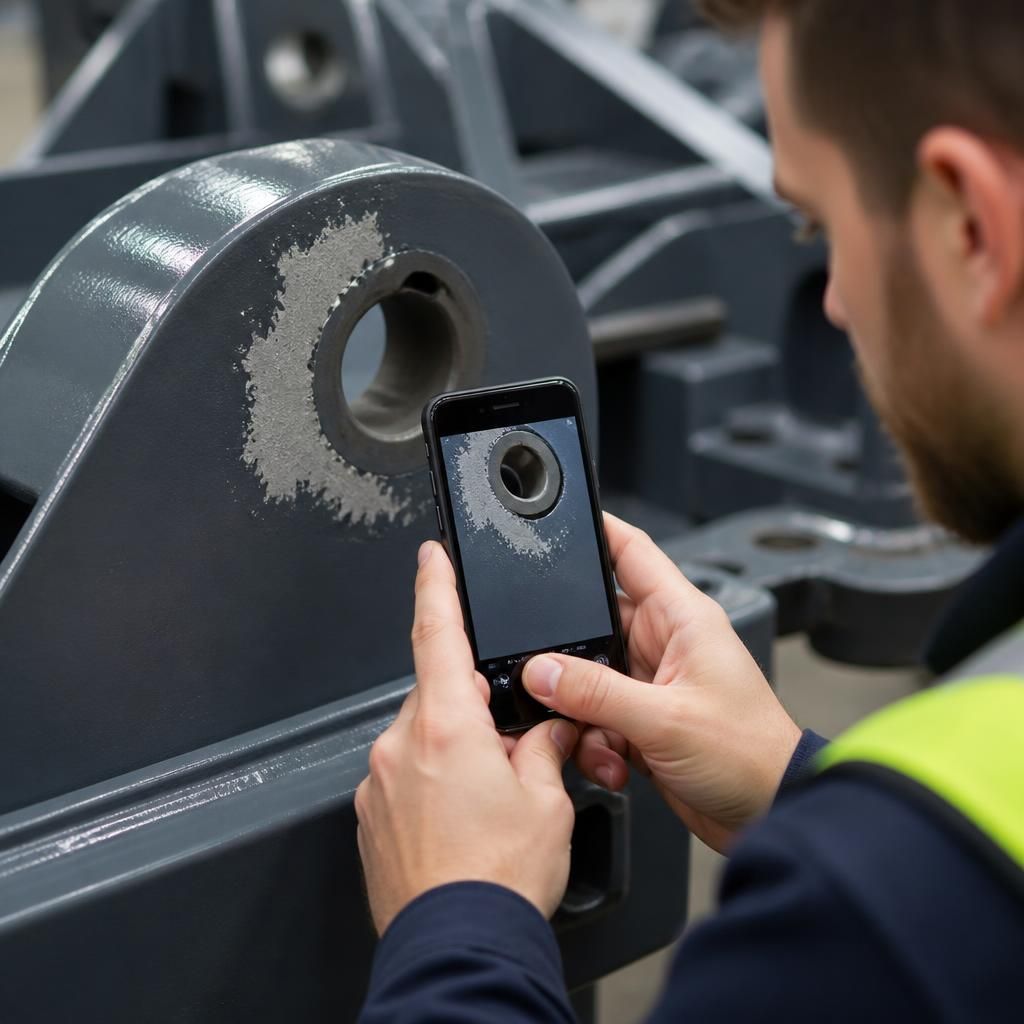
Not every change in appearance means that a Rilsan Nylon 11 coating has failed. Staining, light marking or gradual colour variation may be cosmetic, whereas blistering, bubbling, cracking, flaking or a visible change in adhesion can indicate that moisture or contamination is affecting the coating system. Exposed metal is a higher-priority defect because it removes the protective barrier at that point.
When inspecting a component, assess whether the affected area is isolated or spreading, whether it is close to a joint or edge, and whether the surrounding coating remains firmly bonded. Photographing the area and comparing it during later inspections helps distinguish a stable surface mark from progressive deterioration. If a defect is expanding or the coating can be lifted at its edge, remove the component from conditions that may worsen the damage and obtain advice on the appropriate repair method.
Discuss Rilsan Nylon 11 Maintenance Requirements
If you need to confirm the most suitable maintenance approach for a Rilsan Nylon 11-coated component, discuss its coating specification and service conditions with a powder-coating specialist. This can help identify appropriate cleaning, inspection and repair requirements before deterioration becomes more extensive.