

What considerations should be taken into account when selecting between Nylon and Rilsan coatings for industrial applications?
Select between Nylon and Rilsan coatings by assessing the component’s operating temperature, chemical and moisture exposure, abrasion and impact risks, required flexibility, coating thickness and substrate preparation. Also consider the required finish, application method, specification or compliance requirements, expected service life and whole-life cost, then match these factors to the performance characteristics of the specific coating formulation.
The choice between Nylon and Rilsan coatings should be based on the coating specification required by the component, not on the material name alone. “Nylon” can describe several polyamide powder coating formulations, whereas Rilsan is a specific polyamide 11 coating system. The correct selection depends on the exact grade, the substrate, the service environment, the component’s geometry and any regulatory or customer requirements attached to the finished part.
Start with the coating specification. Ask the coater or powder manufacturer for the technical data sheet and identify the relevant grade rather than relying on a general reference to nylon. Important details include the recommended film build, curing requirements, allowable substrate types, resistance data, colour and gloss range, and any limitations on use. Two products described generally as nylon coatings may have different performance characteristics, so the product designation and approval status should be recorded in the drawing or purchase specification.
Consider whether the coating has to perform as an engineered lining. Rilsan PA11 is often selected where a continuous, chemically resistant and electrically insulating barrier is needed around a metal component. It can be suitable for applications involving contact with fluids, salts or process chemicals, subject to confirmation that the particular grade is compatible. A conventional nylon powder may be more appropriate where the requirement is primarily a tough decorative or functional finish and the operating conditions are less demanding. This is not an absolute distinction: the properties of the chosen formulation and the quality of application remain decisive.
Assess the component’s design and the way it will be used. Recesses, internal passages, threaded features, sharp edges and narrow gaps can affect powder access, film formation and masking. A coating that performs well on an open fabricated part may require a different application approach on a valve body, pipe fitting, bracket or complex machined component. Check whether coating thickness could affect tolerances, assembly clearances, threads, seals or moving interfaces. Areas that must remain uncoated should be identified before processing, with suitable masking specified at the design stage.
Review mechanical contact conditions separately from general abrasion. Determine whether the surface will experience sliding contact, repeated impact, point loading, clamping or contact with another hard material. The relevant question is not simply whether the coating is described as durable; it is whether the selected grade and film construction suit the particular contact pattern. Where parts are handled, assembled or transported after coating, the specification should also address protection against marking and damage before installation.
Check compatibility with adjoining materials and substances. Seals, gaskets, lubricants, cleaning agents and process fluids can affect the suitability of a coating even when the metal component itself is protected. Confirm that the coating will not interfere with sealing, bonding, earthing or electrical contact. If the finished item will be used with potable water, food, medical equipment or a regulated process, the applicable approval must relate to the exact coating grade and end use. A general statement that a coating is nylon or Rilsan is not a substitute for the required compliance evidence.
Give attention to colour, texture and appearance requirements. Nylon and Rilsan finishes may be available in different colours, gloss levels and surface textures, but the available range can depend on the formulation and application method. Appearance can also vary with film thickness, substrate profile and component geometry. If multiple batches need to match, define the accepted colour reference, gloss expectation and inspection method in advance. Where appearance is secondary to protection, a wider finish specification may provide greater practical flexibility.
Consider production and quality-control requirements. The preferred coating must be compatible with the part’s size, weight, handling method and batch volume. Large or awkward components may require particular racking and spraying arrangements, while small parts may need a process that controls coverage and prevents excessive build-up. Agree how coating continuity, thickness, adhesion, visual defects and masking will be checked. For critical applications, representative samples or a trial batch can help confirm that the selected system works on the actual substrate and geometry rather than only on a test panel.
Use testing where the consequence of failure is significant. Laboratory resistance data provides useful guidance, but it cannot reproduce every combination of temperature, chemicals, loading, cleaning and weathering found in service. A trial should use the intended preparation, coating grade and curing conditions. The evaluation may include adhesion, thickness, visual inspection, dimensional checks and exposure to the relevant service media. Results should be judged against defined acceptance criteria agreed by the manufacturer, coater and end user.
Finally, compare the complete specification rather than the powder price. Include preparation, masking, application, inspection, handling, potential rework and the consequences of replacing or recoating the component. A more specialised Rilsan system may be justified where its performance matches a demanding service environment, while a suitable nylon formulation may be the more proportionate choice for a less severe duty. The decision should be documented by linking the selected grade to the operating conditions, design requirements, compliance evidence and inspection plan.
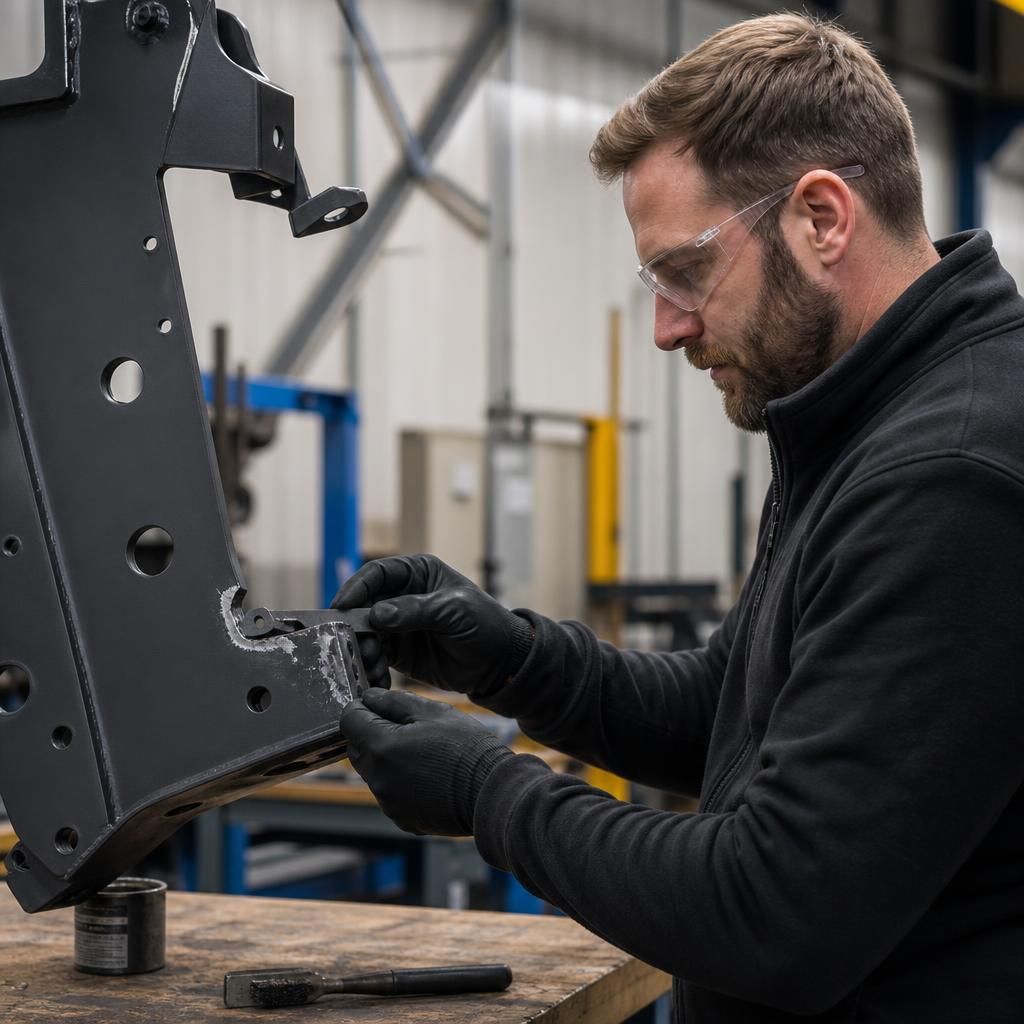
Repair requirements should be considered before selecting a Nylon or Rilsan coating. If a component may be damaged during installation or service, establish how local defects will be identified, prepared and repaired, and whether the approved repair method is compatible with the original coating. A repair system may not reproduce the same film thickness, texture or appearance as the factory-applied finish, so the specification should define acceptable repair areas and inspection criteria. For components that are difficult to remove or replace, the feasibility of future recoating can be an important factor in the initial coating decision.
Discuss Your Nylon or Rilsan Coating Requirements
Discuss your component’s substrate, geometry, operating conditions and performance requirements with the powder-coating.co.uk team to identify whether a Nylon or Rilsan system is appropriate. Sharing the relevant drawings, specifications and service information can support a more informed coating recommendation.