

What is the process for preparing metal surfaces before applying a nylon coating?
Metal surfaces are prepared for nylon coating by removing oil, dirt, rust and existing scale, typically through degreasing and abrasive blasting. The surface is then inspected, treated or primed where required, and kept clean and dry so the nylon can bond evenly during application.
Preparing metal for a nylon coating is a controlled process of making the substrate chemically compatible, physically suitable and correctly presented for application. Beyond removing visible contamination, the preparation must account for the metal type, component design, expected service conditions, coating thickness, masking requirements and the way the nylon powder will be applied.
1. Review the component and coating specification
Preparation begins with assessing the component rather than applying one identical treatment to every part. The relevant factors include:
- the substrate, such as mild steel, stainless steel, aluminium or galvanised metal;
- the required nylon coating system and whether a primer or bonding layer is specified;
- the operating environment, including moisture, chemicals, abrasion and temperature changes;
- areas that must remain free from coating, such as threads, bearing seats, electrical contact points and close-tolerance faces; and
- how the component will be supported, heated, coated and handled.
This review establishes the correct preparation route and prevents a treatment being selected that is unsuitable for the substrate or the finished component.
2. Deal with design features that could affect the finish
Welds, sharp corners, deep recesses, holes and overlapping sections can influence how nylon forms over the surface. Weld spatter and raised edges may create thin spots or visible defects, while sharp corners can reduce coating coverage at the edge. Where appropriate, these features are dressed or corrected so the coating can form a more consistent film.
Welded assemblies also need particular attention because residues from fabrication can remain around joints and in crevices. Any trapped moisture, abrasive media or processing residue must be removed before the component proceeds to coating. Enclosed sections should have suitable drain or vent arrangements where the design allows, especially if the part will be heated during application.
3. Confirm compatibility of any existing treatment
Previously coated, plated or chemically treated components require a separate decision. An existing finish may need complete removal, or it may be retained only where its compatibility and adhesion have been established. Unknown coatings are not a reliable foundation for nylon because they can soften, release gases or separate from the metal when heated.
Where a primer is part of the specified system, it must be suitable for both the substrate and the nylon layer. The primer is applied only after the underlying surface has reached the required condition, and its coverage, drying and handling requirements must be controlled before the topcoat is introduced.
4. Protect areas that must not be coated
Masking is planned before the part enters the coating area. Threads, bores, machined faces, hinges and connection points may need plugs, caps or other suitable masking materials. Masking must remain stable during handling and heating without introducing fibres, adhesive residue or other contamination.
Masking design also affects the edge of the nylon film. A poorly positioned mask can leave an excessive build-up, an exposed strip or an uneven transition. For components assembled after coating, the required clearance should therefore be considered before preparation starts rather than corrected after curing.
5. Establish the required surface profile
The surface must have a profile that gives the nylon system a reliable mechanical key without damaging critical dimensions. The appropriate profile depends on the substrate, component thickness and coating specification. Excessive treatment can distort thin sections, round precision edges or alter the fit of mating parts, whereas insufficient profile may reduce the available key for the coating.
Particular care is needed with aluminium and other relatively soft metals. They can be marked more easily than steel, so the treatment must balance adhesion requirements with dimensional control. Galvanised surfaces may also require a substrate-specific approach because the zinc layer forms part of the finished system and must not be needlessly removed.
6. Control handling before coating
After the prepared condition has been achieved, components should be handled with clean gloves or suitable contact points. Bare hands can transfer oils and salts back onto the surface, while unprotected storage can allow flash corrosion or airborne contamination to develop. Parts should be supported so that prepared faces do not contact dirty racks, floors or other untreated items.
Hanging points are selected with the final coating in mind. They should provide secure support and, where the application method requires it, a dependable electrical path. Contact points are normally located in areas where a small uncoated mark can be accepted or subsequently addressed without affecting function.
7. Verify the condition before application
Final checks should confirm that the component is free from visible residue, unwanted oxidation, loose material, masking debris and moisture. The preparation record may also identify the substrate, treatment route, primer details, masking arrangement and any areas requiring special attention.
Only after these checks should the component move into nylon application. This sequence is important because preparation defects are generally more difficult to correct once the coating has been applied. A controlled handover from preparation to coating helps maintain consistent adhesion and finish quality across individual parts and production batches.
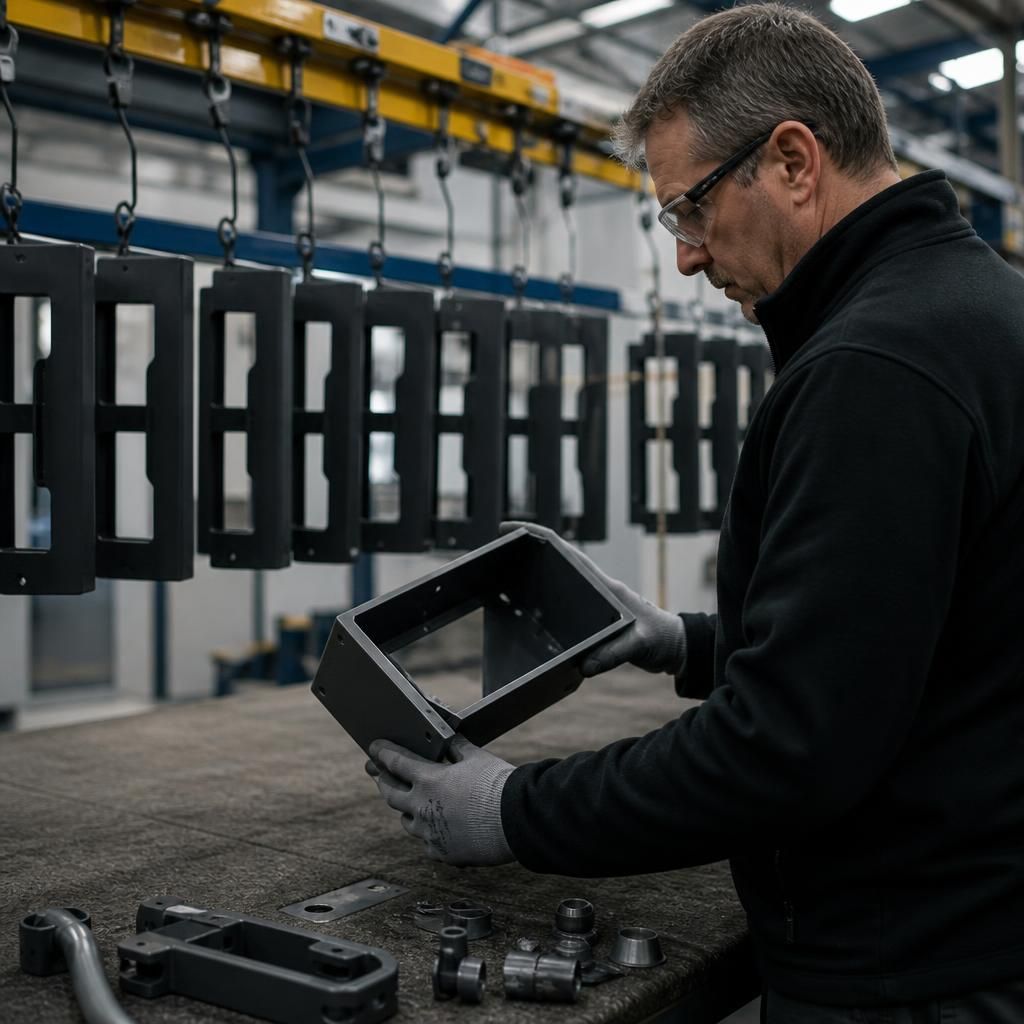
For unfamiliar substrates, unusual geometries or a newly specified nylon system, a representative trial component can be prepared before the full batch is processed. This allows the preparation route, masking arrangement and coating behaviour to be reviewed under the same handling and heating conditions intended for production.
The trial should be inspected after coating for consistent coverage, edge definition, visible contamination and adhesion. Any adjustment to the preparation method can then be made before the complete batch enters production, reducing the risk of repeating a substrate or design-related defect across multiple components.