

What are the key considerations for determining the optimal powder coat thickness for different steel applications?
The optimal powder coat thickness for steel depends on the application’s corrosion exposure, mechanical demands, required finish and the component’s dimensional tolerances, rather than on applying the thickest possible layer. Specify the coating system and target thickness against the steel substrate, pretreatment, service environment and relevant technical guidance, then verify the cured film consistently across the component.
Optimal powder coat thickness is the specified dry film thickness (DFT) range that gives a steel component the required corrosion protection, wear resistance and appearance without creating defects or interfering with assembly. It should be selected as part of a complete coating specification, taking account of the steel grade, surface preparation, service environment, component design, powder chemistry, curing conditions and dimensional tolerances.
Start with the service environment
The surrounding conditions are usually the first consideration. Steel used indoors in a dry, low-contamination environment may not require the same coating build as steel exposed to persistent moisture, condensation, road salts, industrial pollutants or coastal conditions. Outdoor components and items in aggressive environments generally need a coating system designed for the relevant corrosion category, rather than simply an unusually thick layer of powder.
Exposure can also vary across one component. A frame may have sheltered faces, exposed horizontal surfaces, concealed joints and areas where water collects. The specification should consider the most demanding parts of the intended installation and whether the design allows water or contaminants to drain away. Powder thickness cannot compensate fully for poor drainage, unsealed crevices or inadequate pretreatment.
Match the thickness to the performance requirement
Thickness should reflect what the coating must withstand. A decorative steel panel has different requirements from a bracket subject to abrasion, handling, impact or repeated contact. Where wear is the main concern, the powder type, substrate preparation and curing profile are as important as the film build. A thicker coating is not automatically harder or more resistant; excessive build can make the film more prone to cracking, sagging, edge defects or poor adhesion if the system is not designed for it.
Where corrosion protection is critical, specify the powder coating alongside the pretreatment and any primer or multi-coat system. A single decorative coat may not provide the same protection as a system designed for severe exposure. The required film build should therefore be defined for the complete system, including any primer layer, rather than treating the topcoat in isolation.
Consider the steel and its surface condition
Steel condition affects how consistently a coating can be applied. Mill scale, rust, oil, grease, welding residues and fabrication marks can prevent proper adhesion or create local failures beneath an otherwise adequate film. Cleaning, preparation and chemical pretreatment must be suitable for the steel and the selected powder system.
Surface roughness also influences the result. On a rough or blasted surface, part of the coating film follows the surface profile, so a single reading may not represent the protection over the peaks and valleys. The specified thickness must be achievable over the prepared surface without obscuring required detail or leaving the coating too thin on high points.
Galvanised or previously treated steel may need a different specification from untreated mild steel. Outgassing, trapped gases and differences in surface chemistry can cause pinholes, bubbling or adhesion problems. These risks should be assessed before setting the target thickness, since adding more powder does not remove the underlying cause.
Account for component geometry
Powder is attracted to the component during application, but electrical field effects mean that coverage is not always uniform. External corners, sharp edges, recesses, internal faces, holes and areas close to welds can receive a different build from broad, accessible faces. Faraday cage effects can make it difficult for powder to reach deep recesses, while corners and edges may collect more material.
Complex fabrications should therefore be reviewed before coating. Drainage and vent holes may be needed in hollow sections, and the design should avoid narrow gaps that are difficult to clean and coat. If a coated part must fit inside another component, the coating allowance needs to be included on all relevant faces. Threads, bearing seats, locating surfaces, electrical contact points and close-fitting holes may need masking or a controlled coating limit.
Protect dimensional and functional tolerances
Thickness adds material to the steel and can affect assembly, movement and alignment. The specification should identify surfaces where coating build is restricted, including mating faces, sliding areas, hinges, threaded features and precision interfaces. Masking may be preferable to accepting a reduced or variable coating thickness in these locations.
For assemblies, define whether the target applies to the individual part, the visible face, or a particular functional area. A general target may be suitable for open structural sections but insufficiently precise for components that must fit to a controlled tolerance. Drawings should show uncoated areas, masking requirements and any surfaces where measurement is required.
Choose the powder system before finalising the target
Different powder technologies and formulations have different application characteristics and curing requirements. The manufacturer’s technical data should be used to confirm the suitable film-build range, cure schedule, substrate temperature and permitted application method. The powder must reach the specified cure, not merely appear dry, because under-cured or over-cured material can affect adhesion, flexibility, colour and durability.
Colour, gloss and texture can also influence the visual result. Textured finishes may disguise minor variation differently from smooth finishes, while dark or high-gloss coatings can make surface defects more noticeable. Appearance requirements should be agreed separately from corrosion or mechanical performance, with representative samples used where colour and texture are important.
Specify a range rather than a single isolated reading
In practice, the requirement should define a target range, a lower acceptable limit and, where necessary, a maximum build. A single nominal value does not describe the variation that may occur across a fabricated component. The acceptance criteria should state where readings are taken, how many areas are assessed and how local variations are treated.
Measurement should use a suitable calibrated dry-film thickness instrument for the substrate and coating. Readings should be taken on representative flat areas as well as locations that are critical to performance, such as edges, corners and recesses where access permits. Results should be recorded by batch or component group so that inconsistent application can be investigated rather than concealed by an overall average.
Verify the complete process
Thickness control starts before powder application. Confirm the steel condition, preparation method, masking, powder identification and equipment settings. During application, check gun distance, voltage, powder flow, part earthing and line conditions, as these influence transfer and uniformity. After curing, inspect the finish for runs, pinholes, craters, orange peel, poor coverage, contamination and signs of inadequate cure.
Where the application is safety-critical, exposed to severe corrosion or subject to contractual requirements, the coating specification may also require adhesion, cure, porosity, impact or corrosion testing. The appropriate tests depend on the component and governing standard. Standards such as ISO 2808 can provide a framework for determining film thickness, while the relevant corrosion-protection specification should define the performance expected from the full system.
Use a written, application-specific specification
A robust specification should record the steel substrate, preparation and pretreatment, powder system, coating sequence, target DFT range, restricted areas, cure requirements, inspection method and acceptance criteria. It should also state whether the requirement applies to the whole component or only to defined surfaces.
The best thickness is therefore the lowest controlled film build that meets the application’s verified performance requirements across the component. Setting it in consultation with the powder coater, fabricator and, where relevant, the powder manufacturer helps reconcile corrosion protection with appearance, fit and production repeatability.
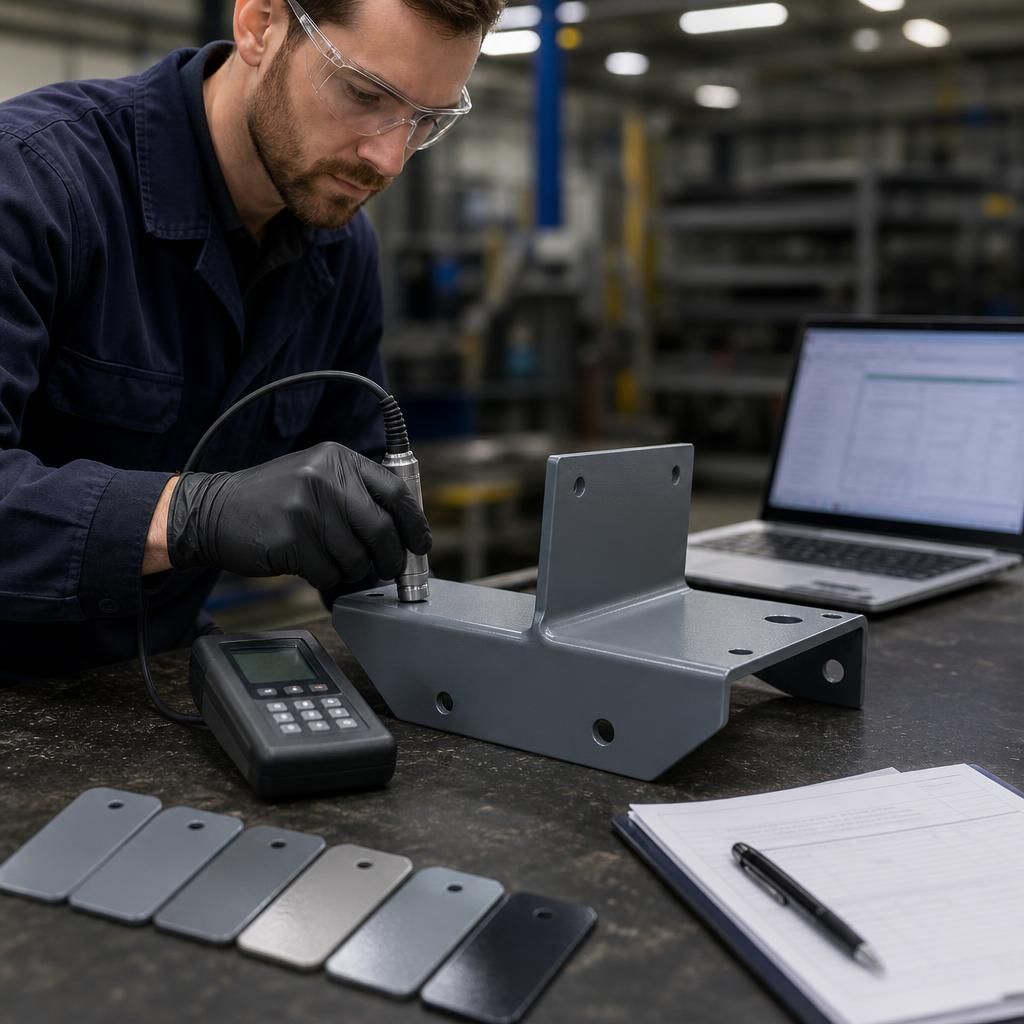
A representative test piece can help establish an achievable powder coat thickness before production begins. It should use the same steel type, surface preparation, powder system and curing conditions as the finished components, and should reflect important features such as edges, recesses or joints.
Assess the test piece against the agreed dry film thickness range and visual requirements, then record any areas where the coating build differs. This provides a practical basis for confirming the specification, refining application settings and identifying design features that could make consistent thickness difficult. For repeat batches, retain the agreed criteria so that subsequent components are assessed against the same standard.