

What are the essential considerations when selecting a powder coating provider for electrical insulation purposes?
When selecting a powder coating provider for electrical insulation, assess their understanding of the required dielectric performance, suitability of the powder for the component and operating environment, surface preparation, coating thickness, curing control and inspection requirements. Also confirm they can maintain consistent results across the required batch size, handle the component dimensions and geometry, provide appropriate technical documentation, and support practical collection and delivery across the Midlands.
Selecting a powder coating provider for electrical insulation requires more than checking whether a coating is described as insulating. The provider must be able to translate the component’s electrical, mechanical and dimensional requirements into a controlled coating specification, then demonstrate that the finished parts meet the agreed acceptance criteria.
Clarify the electrical duty of the coating. Before requesting a quotation, define what the coating is expected to do. Relevant information may include the working voltage, required insulation resistance, exposure to heat or moisture, contact with chemicals, and whether the coating forms part of a safety-critical assembly. The provider should understand the difference between general electrical isolation and a coating that must withstand a defined dielectric test. This helps prevent a technically suitable powder from being used in an application for which its electrical properties have not been verified.
Check how requirements will be tested. A capable provider should discuss the proposed test method, test conditions, sample selection and pass or fail criteria rather than relying on a general statement that the finish is non-conductive. Depending on the application, testing may involve dielectric withstand, insulation resistance, continuity checks on masked areas, visual examination or adhesion assessment. It is also important to establish whether testing is carried out on production parts, representative samples or both, and how results are recorded.
Review masking and electrical contact control. Many insulated components still require bare areas for earthing, bolted joints, terminals, sliding fits or electrical connections. Ask how the provider will define and protect these areas, including holes, threads, mating faces, slots and narrow edges. Masking must be repeatable and removed without damaging the surrounding finish. The drawing should identify prohibited coating zones and permissible overspray, since an otherwise sound insulating layer can cause assembly or earthing problems if it reaches the wrong surface.
Consider dimensional effects. Powder coating adds a measurable layer to the component and may affect clearances, threaded features, press fits, hinges and moving interfaces. Discuss critical dimensions before processing and agree how they will be checked afterwards. The provider should also identify areas where geometry could produce thin coverage, heavy build-up or difficulty in achieving a continuous layer. This is particularly relevant to folded fabrications, enclosed sections, sharp transitions and parts with close-fitting interfaces.
Ask about sample approval and first-off work. A representative trial or first-off inspection can confirm the colour, appearance, masking lines, coverage and fit before a larger production run proceeds. For electrical insulation, the approval process should include the relevant functional checks, not just visual acceptance. The approved sample or specification should state the agreed finish, protected areas, test requirements and any acceptable cosmetic limits, giving both parties a clear reference for subsequent work.
Assess traceability and change control. Electrical performance can be affected by changes in powder formulation, substrate condition, preparation method or processing settings. Ask whether the provider can identify the material used, link parts to a production batch and retain appropriate process or inspection records. There should also be a clear process for approving changes to the powder, masking arrangement, preparation system or finishing sequence. This is valuable when coated parts are incorporated into equipment that must be investigated or reproduced later.
Understand defect management and rework. Agree how the provider will handle pinholes, contamination, poor coverage, impact damage, incorrect masking or other non-conformities. Rework is not automatically suitable for an electrically insulating component: removing and recoating an area may affect adhesion, dimensions, edge coverage or the cleanliness of an electrical contact. A sound specification should set out when a part can be repaired, when it must be rejected and which checks are repeated after rework.
Examine handling and packaging arrangements. The coating must remain intact between finishing and assembly. Parts should be supported without marking important surfaces, separated where contact could cause abrasion and protected at vulnerable edges or masked zones. Ask how the provider identifies parts, prevents mixing between batches and communicates any handling restrictions. This is especially important where a small scratch, uncoated patch or displaced mask could affect the intended insulation function.
Use a practical supplier checklist. When comparing providers, ask:
- Can the provider review drawings and identify electrically critical features?
- How will insulation performance be verified and documented?
- How are earthing points, terminals, threads and mating surfaces protected?
- Which dimensions and tolerances require checking after coating?
- How are non-conforming or damaged parts controlled?
- Can the provider maintain consistent identification and records for each production batch?
A provider that answers these questions clearly is better placed to deliver an insulating finish that works as part of the complete component, rather than simply producing a visually uniform surface. For a Midlands manufacturer or fabricator assessing a specialist service, the most useful comparison is therefore the quality of the technical discussion, documented controls and agreed inspection plan—not coating description alone.
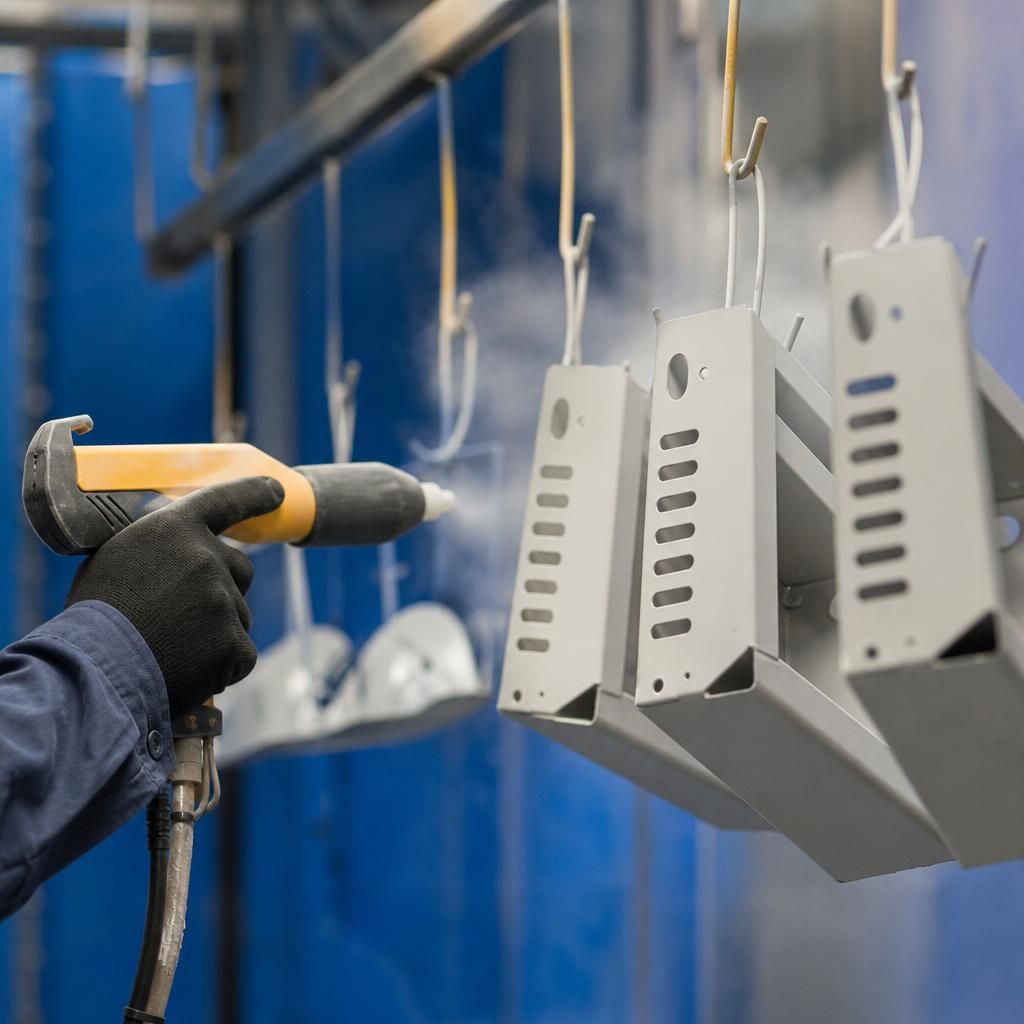
A suitable powder coating provider should distinguish between evidence about the coating and certification of the finished electrical product. A coating may provide an insulating barrier, but the component’s compliance depends on the complete design, including substrate, clearances, creepage distances, connections and operating conditions.
Before appointing a provider, establish how technical information will be shared with the design authority or compliance team. Useful documentation may include:
- the powder manufacturer’s technical data and stated electrical properties;
- the agreed coating specification, including areas to be insulated and areas that must remain conductive;
- records from any agreed dielectric or insulation-resistance testing;
- details of the substrate, preparation system and curing conditions; and
- identification of the parts or batches covered by the evidence.
The provider should be clear about the limits of its test evidence and avoid treating a general non-conductive finish as proof of product compliance. This makes it easier for the responsible engineer to assess whether the coated component is suitable for its intended assembly and to identify any further validation required.