

What quality control measures should be implemented to ensure the reliability and performance of electrostatic epoxy powder-coated components?
Reliable electrostatic epoxy powder-coated components require controlled preparation, application and curing, supported by documented inspections at each stage. Quality checks should include surface cleanliness, coating coverage and thickness, cure verification, adhesion and finish testing, with batch records providing traceability from incoming metalwork to final release.
Quality control for electrostatic epoxy powder-coated components should be a documented, risk-based system covering the specification, materials, equipment, process conditions, testing and final handling. The purpose is to ensure that every batch meets its agreed appearance and performance requirements, rather than relying on a visual check at the end of production.
Define acceptance criteria before production. The job specification should state the required powder type, colour, gloss level, coating thickness range, masked or uncoated areas, edge requirements and intended service environment. It should also identify any performance requirements such as resistance to chemicals, abrasion, impact, moisture or outdoor exposure. Agreeing these points in advance prevents subjective decisions about whether a component is acceptable and ensures that inspection results can be compared with the correct criteria.
The specification should also account for the component itself. Drawings and work instructions need to identify holes, threads, contact points, mating faces and surfaces that must remain free from coating. Weld spatter, sharp burrs, distortion and poorly finished repairs can affect both the finished appearance and the way the component fits its assembly. Recording these features before coating helps separate substrate-related defects from process-related defects.
Control incoming materials and powder. Metalwork should be checked against the order and drawing before it enters the coating process. Useful checks include dimensions, surface condition, quantity, identification and any damage caused during fabrication or transport. Components with oil, corrosion, weld residue or incompatible previous finishes should be segregated until their condition has been assessed.
Powder should be identifiable by product information and batch reference, with storage conditions controlled in line with the manufacturer’s instructions. Different colours, formulations and reclaimed materials should not be mixed without an approved process. Where powder recovery is used, the proportion and treatment of reclaimed material should be controlled because uncontrolled variation can affect appearance and performance.
Keep application equipment under control. The spray equipment, booth, extraction system, compressed-air supply and earthing arrangements should be included in a planned maintenance programme. Guns and nozzles can wear or become contaminated, while poor earthing can reduce transfer efficiency and produce uneven deposition. Settings such as voltage, current, powder output and air flow should be established for the component and recorded where they are critical to repeatability.
Calibration and verification are important for instruments used to make acceptance decisions. This can include coating thickness gauges, temperature recorders, gloss meters, colour-measurement equipment and test apparatus. Equipment should be checked at defined intervals, identified with its status and removed from use if it is damaged or gives questionable readings.
Control the curing process using the metal temperature. Oven air temperature alone does not demonstrate that an epoxy coating has received the required cure. The control plan should consider part mass, geometry, loading pattern and the specified powder’s cure schedule. Temperature profiling with suitable recording equipment can show how quickly the metal reaches the required temperature and how long it remains there. This is particularly important for heavy fabrications and mixed-size batches, where heat-up rates may differ considerably.
Oven performance should be checked periodically at representative positions, with attention to cold spots, excessive temperature variation and changes caused by maintenance or altered loading. Any deviation should trigger an assessment of affected work rather than being treated as an administrative issue only.
Use a planned inspection and test schedule. Inspection should be proportionate to the risk and value of the component. A first-off or approval piece can be examined before a full batch proceeds, followed by defined in-process and final checks. The plan should state the sampling approach, inspection conditions, equipment to be used and the person responsible for accepting or rejecting the work.
- Visual examination should be carried out under consistent lighting and from an agreed viewing distance, looking for runs, craters, pinholes, inclusions, orange peel, bare areas and unwanted contamination.
- Colour and gloss checks are more reliable when measured against an approved reference or retained standard rather than judged solely by eye.
- Coating thickness measurements should be taken at representative locations, including areas prone to excessive build-up or insufficient coverage, while avoiding misleading readings over edges or holes.
- Adhesion, flexibility, impact, abrasion or chemical-resistance tests should be selected according to the component’s operating conditions and the purchaser’s specification.
Test methods should be agreed before work starts. Standards such as ISO or ASTM methods may be appropriate, but the method, equipment, conditioning and acceptance limit must be defined because results from different procedures are not necessarily interchangeable. Destructive tests should normally be performed on representative samples, test panels or agreed sacrificial areas so that production components are not unnecessarily damaged.
Manage non-conforming work formally. A failed inspection should result in clear identification and segregation of the affected batch or components. The record should describe the defect, its location, likely cause and disposition. Possible outcomes may include approved rework, stripping and recoating, repair of the substrate, use under concession or rejection. Rework should not be assumed to solve every problem: excessive build, poor intercoat compatibility or an unsuitable substrate condition may require technical review before further coating is applied.
Recurring defects should be investigated for their underlying cause. Useful evidence may include powder batch information, equipment settings, oven profiles, operator records, component orientation and environmental conditions. Corrective action is more effective when it changes the relevant process control rather than simply increasing final inspection.
Protect quality after coating. Finished components should be handled with clean equipment and suitable protective materials to avoid scratching, impact damage and contamination. Contact points, threaded features and edges may need specific protection during stacking and movement. Packaging should support the component’s geometry and prevent coated surfaces rubbing together. The release record should confirm the applicable checks, identify the batch and show any approved deviations or concessions.
A robust quality system therefore combines defined requirements, controlled materials and equipment, verified process conditions, proportionate testing, disciplined non-conformance handling and traceable release documentation. This approach provides objective evidence that electrostatic epoxy powder-coated components are suitable for their intended use and makes it easier to identify the source of any issue that arises during assembly or service.
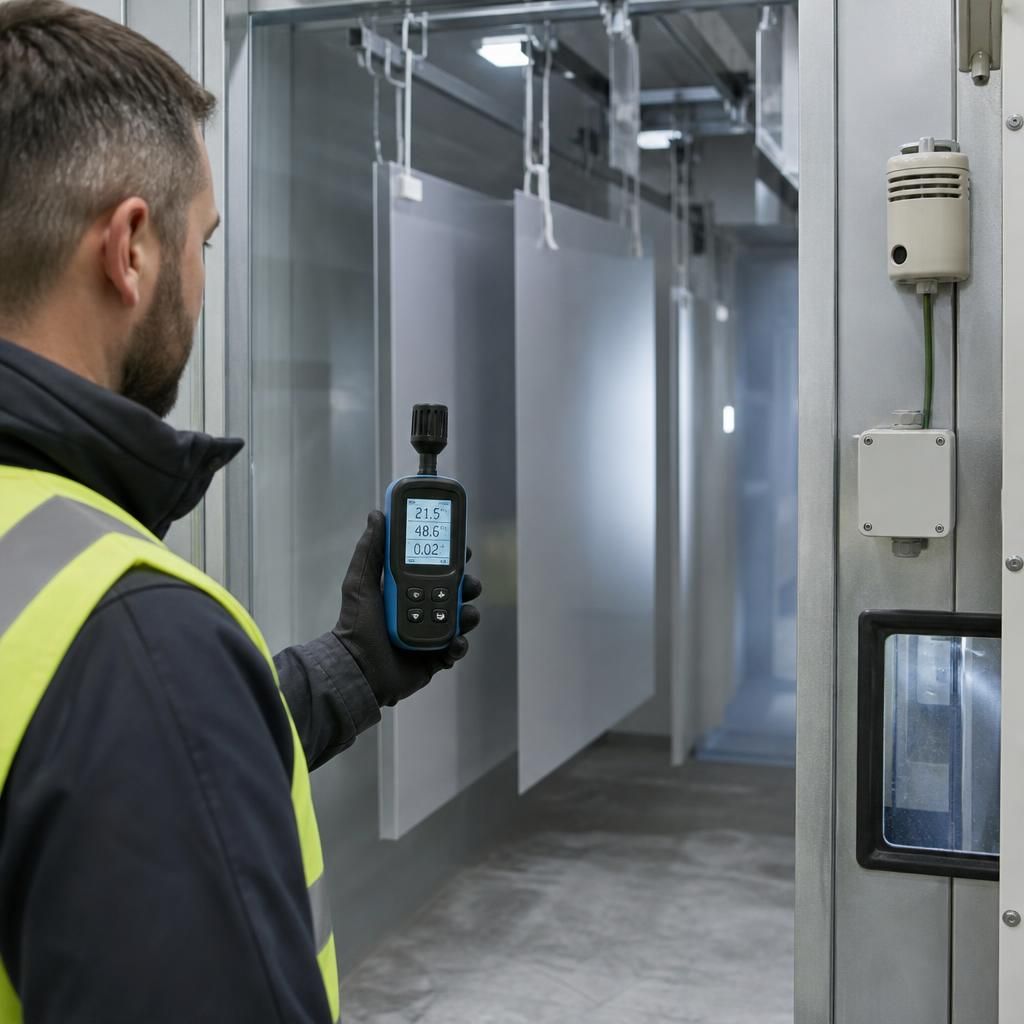
Environmental control is an important quality measure during electrostatic epoxy powder coating because air temperature, humidity and contamination can affect powder application and film formation. The spray area should be kept suitable for the powder system, with conditions monitored rather than judged by comfort or appearance alone.
Before coating, the component temperature should be considered alongside the surrounding air conditions. A cold surface may attract condensation, while excessive airborne dust, oil vapour or moisture can become trapped in the finish. Monitoring and recording relevant conditions provides useful evidence when investigating defects such as poor appearance, pinholing or reduced adhesion.
Where conditions fall outside the agreed process limits, coating should be paused or the work assessed before proceeding. This control is particularly useful for large fabrications and components moved between different preparation, coating and storage areas.