

How does the thickness of the powder coating layer impact the performance and longevity of aluminium frames and parts in industrial applications?
The thickness of a powder coating layer affects an aluminium frame or part’s coverage, corrosion resistance, impact protection and service life. A correctly specified, evenly applied thickness provides durable protection, while an excessively thin or thick layer can reduce performance through incomplete coverage, brittleness, poor adhesion or curing problems.
Powder coating thickness is the depth of the cured dry film covering the aluminium surface. Its effect on performance depends on whether the specified film build is suitable for the component’s environment, geometry, handling requirements and coating system. A greater thickness does not automatically provide a longer service life; consistency within the appropriate specification is usually more important than applying the maximum possible build.
Thickness is specified as a target range rather than a single ideal value. The correct range depends on the intended use of the frame or part. An internal enclosure, architectural frame, plant component and heavily handled fabricated part may require different coating specifications. Exposure to moisture, ultraviolet light, chemicals, abrasion or outdoor pollutants should be considered alongside the aluminium alloy, component design and expected handling. The coating supplier can then select a suitable powder system and process settings rather than treating thickness as an isolated requirement.
The stated thickness normally refers to the dry film after curing, not the amount of powder initially sprayed. During production, the coating is applied electrostatically and then cured so that the particles flow together into a continuous film. Film build can vary across a component because of its shape, the position of edges and recesses, the electrical characteristics of the substrate and the way the part is hung. Large frames, folded sections and assemblies with enclosed areas therefore need particular attention to representative coverage and measurement.
Dimensional fit is one of the most important practical effects of coating thickness. The coating adds material to every coated surface, which can affect holes, threads, bearing seats, sliding fits, hinge locations, interlocking sections and mating faces. If a part has close tolerances, these areas may need to be masked, plugged or allowed for during design. Contact surfaces used for electrical earthing or bonding may also require defined uncoated zones or post-coating treatment, depending on the assembly design.
Film build also influences the finished appearance. An even thickness supports consistent colour, gloss and texture across a batch, whereas variation can make adjacent surfaces look different even when the same powder has been used. Excessive build may make edges appear rounded, reduce the definition of details or produce surface defects if the powder does not flow and cure as intended. These considerations are particularly relevant where aluminium frames are visible or where coated parts are assembled alongside one another.
Thickness must be considered with the curing cycle. The metal temperature, time at temperature, component mass and oven loading all affect how the powder forms its final film. A heavier coating or a complex assembly may need process control to ensure that the material reaches its specified cure without damaging the finish. Measuring thickness alone cannot confirm that the coating has been correctly cured, so production checks may also include visual assessment, adhesion testing or other checks agreed for the application.
For reliable results, the coating requirement should be defined before manufacture or finishing. Useful information includes:
- the component’s operating environment and likely exposure to moisture, chemicals, sunlight or abrasion;
- critical dimensions, threaded areas, mating faces and surfaces that must remain conductive;
- areas requiring masking, plugging or special handling;
- the required colour, gloss and texture, where appearance is important;
- the acceptable dry-film thickness range and the locations to be inspected; and
- any requirements for adhesion, cure, hardness or batch-to-batch consistency.
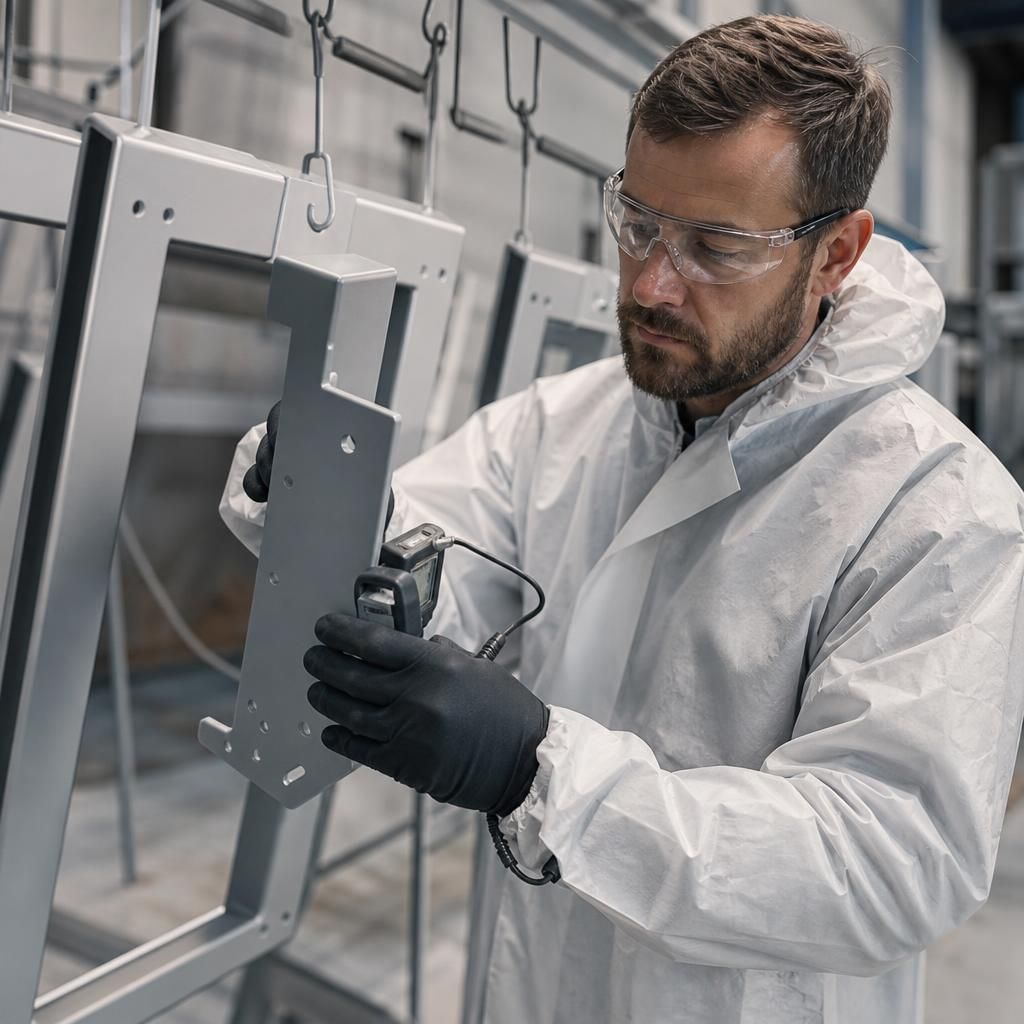
Dry-film thickness is commonly checked with a suitable calibrated gauge at multiple representative points rather than at one convenient location. A sensible inspection plan considers flat faces, edges, corners, recesses and areas close to fixtures. The results should be assessed against the agreed specification, taking account of the instrument’s capability and the normal variation created by the component’s geometry.
In practice, the most durable specification balances protection, appearance, dimensional control and process repeatability. Too little film may leave some features outside the intended specification, while too much can create fit, finish or curing issues. Selecting the coating system and target thickness together, then confirming the result through controlled application and inspection, gives aluminium frames and parts a more predictable performance in industrial service.
Powder coating thickness can only protect aluminium effectively when the coating is properly bonded to a clean, prepared surface. Film build does not compensate for oil, oxidation, dust or other contamination beneath the coating. If the interface is weak, moisture can reach the substrate through damaged areas and cause loss of adhesion, regardless of how thick the outer layer is.
Surface preparation and the coating system therefore need to be considered alongside the specified thickness. Cleaning, suitable pretreatment and correct handling before application help establish a stable bond between the aluminium and the powder coating. This is particularly important for frames and parts exposed to condensation, road pollutants, industrial contaminants or repeated handling.
In practical terms, a moderately built film on a well-prepared surface can provide more dependable protection than an unnecessarily heavy film applied over an inadequately prepared substrate. When assessing coating performance, review the complete system: substrate preparation, powder selection, application, curing and the finished dry-film thickness.
Discuss the right powder coating thickness for your aluminium parts
Share your aluminium frame or part drawings, operating conditions and dimensional requirements with the coating team to discuss a suitable powder coating specification. This allows the required thickness, finish and inspection requirements to be considered before production.