

What specific qualities should you look for in a coating provider to ensure your steel tubes meet rigorous industry standards?
Choose a steel tube coating provider that can demonstrate controlled surface preparation, consistent powder application and curing, documented quality checks, and traceability from incoming material to finished components. They should also understand the relevant industry requirements, discuss the required finish and service conditions clearly, and provide collection and delivery arrangements suited to your production schedule.
A suitable steel tube coating provider should be able to translate the required industry standard into a documented coating specification, prove that the finished work meets that specification, and manage the practical risks associated with tubular components. The strongest indicators are technical competence, appropriate testing, controlled inspection, clear records, and an ability to identify non-conforming work before it reaches the customer.
Look for standards knowledge rather than general assurances. A provider should ask which industry, product specification and service conditions apply to the tubes. The correct requirements may relate to corrosion protection, coating thickness, appearance, adhesion, chemical exposure, outdoor use, temperature or subsequent fabrication. A technically capable supplier will explain which requirements are relevant, identify any conflicts between them and confirm the agreed acceptance criteria in writing.
This is important because “powder coated” does not describe a single level of performance. A finish intended for an internal framework may not be suitable for tubes exposed to moisture, road contaminants, cleaning chemicals or industrial atmospheres. The provider should therefore assess the intended use before recommending the coating system, rather than treating colour selection as the main specification.
Check how the specification is controlled. The quotation or order confirmation should record more than a colour reference. It may need to include the coating type, required appearance, target film build, areas to remain uncoated, masking requirements, edge or end treatment, inspection criteria and any restrictions on handling. Clear documentation reduces the risk of assumptions being made between the purchaser, coating provider and end user.
For steel tubes, dimensional and handling details also matter. The provider should confirm the tube size, wall construction, length, weight, quantity and any holes, threads, joints or attached components that could affect processing. They should discuss how tubes will be supported, protected and inspected without damaging the finish. This is particularly relevant where long or hollow sections must be moved through the works or where coating must not interfere with assembly.
Ask what evidence is supplied with the completed work. Depending on the project, useful records may include inspection results, coating identification, batch details, non-conformance records and a certificate confirming that the work was completed against the agreed specification. Test evidence should be relevant to the requirement: for example, adhesion testing for bond performance, coating-thickness checks for coverage, and visual inspection for runs, pinholes, contamination, impact damage or unacceptable variation.
A professional provider should also be able to explain the limitations of each test. A thickness reading alone does not demonstrate suitability for a corrosive environment, while a visual check cannot confirm adhesion. Evidence is valuable when it is linked to a defined acceptance limit and the particular batch of tubes supplied.
Evaluate consistency across batches. If tubes are being coated in stages, the supplier should have a method for maintaining the agreed appearance and performance from one batch to the next. Relevant controls include consistent identification of the powder and substrate, separation of different specifications, inspection of first-off work where appropriate, and comparison against an approved reference. This helps prevent differences in colour, gloss or texture becoming apparent only after components have been installed.
Assess their approach to non-conforming work. No coating process should rely on defects being overlooked. Ask what happens if a part fails inspection, is damaged during handling or does not meet the specified appearance. The provider should isolate the affected components, record the issue, determine whether repair or reprocessing is technically acceptable, and obtain approval where the original specification would be changed. Rework should not be presented as acceptable without considering its effect on dimensions, appearance and long-term performance.
Choose a provider that communicates technical risks early. Tubes may arrive with weld spatter, oil, marking residue, moisture, sharp edges, incompatible previous finishes or fabricated attachments. Although the coating provider is not responsible for every upstream manufacturing issue, it should identify conditions that could compromise the result and state what needs to be corrected before processing. This is more useful than accepting unsuitable parts and discussing the problem after coating.
Finally, consider whether the provider can support the documentation requirements of your own quality system. A reliable supplier should give consistent job records, use unambiguous part identification and make it clear which checks were performed, by whom and against what criteria. For regulated, safety-critical or customer-audited work, agree these requirements before production begins.
In practical terms, the best choice is not simply the provider offering the lowest coating price. It is the one that can connect the end-use conditions, written specification, component details, inspection evidence and handling arrangements into one controlled process. Requesting a sample record, inspection plan or example of the information supplied with a completed job can reveal far more about suitability than a general claim of high quality.
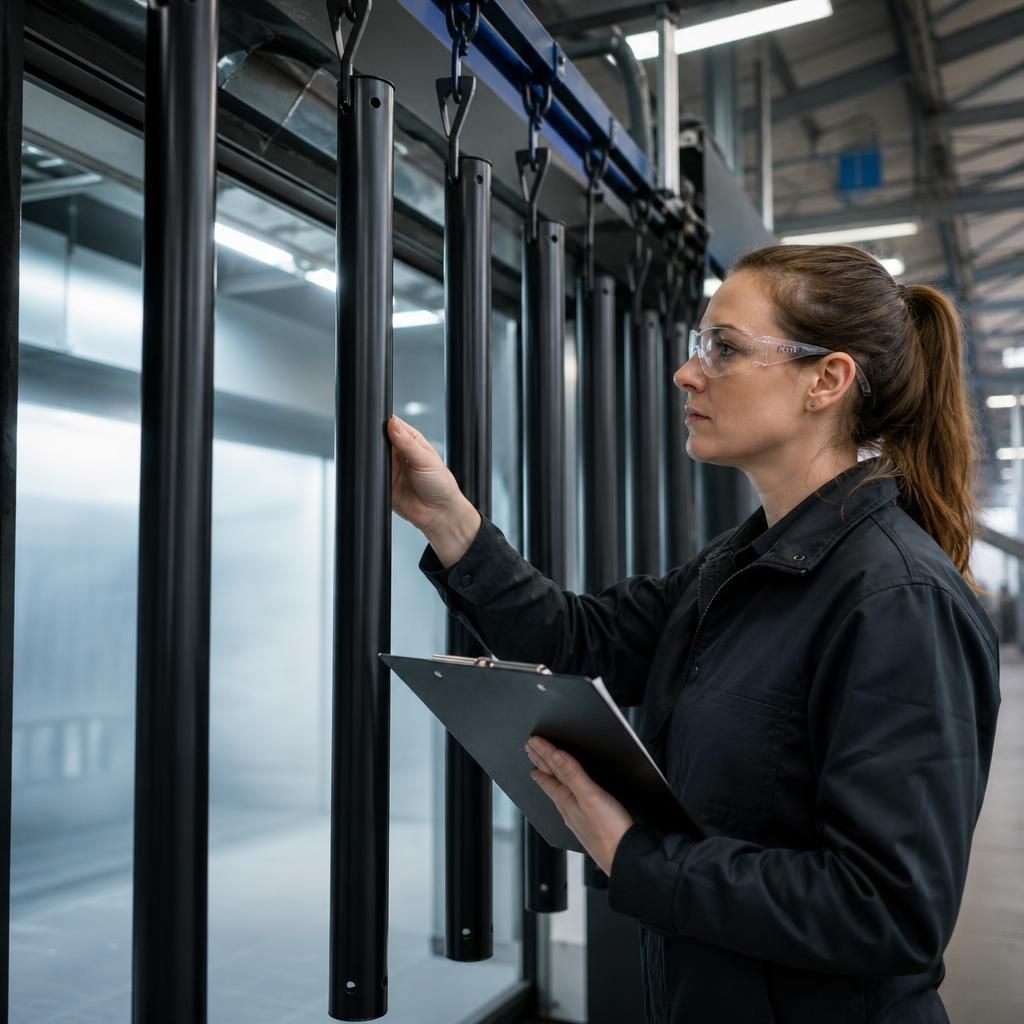
A useful quality indicator is how the provider controls the coating process before the finished tubes reach inspection. Powder should be identified correctly, stored in suitable conditions and kept separate from other specifications. Application equipment should be maintained and checked so that coverage remains stable, while the curing cycle should be verified against the coating system and tube characteristics rather than assumed from conveyor settings alone.
Ask whether these controls are recorded for each relevant production run. Records of powder identification, equipment checks and cure verification provide stronger evidence of process control than a final visual inspection by itself. This is particularly important for steel tubes with different wall thicknesses or complex profiles, as heat-up behaviour can vary and affect the final coating performance.
Discuss your steel tube coating requirements
Discuss your steel tube coating requirements with our team, including the tube dimensions, intended service conditions and documentation needed for your quality process. We can help establish the information required to assess a suitable coating specification.