

How do powder colour paint options support compliance with industry standards and regulations?
Powder colour paint options support compliance by providing a controlled, specified finish that can be matched to requirements for corrosion resistance, adhesion, hardness, chemical exposure and appearance. Compliance depends on selecting a suitable coating system, preparing the metal correctly, controlling application and curing, and retaining the relevant product and inspection records as evidence.
Powder colour paint options support industry compliance when the selected coating, colour and finish are demonstrably suitable for the component’s intended use and the applicable specification. The powder itself is only one part of compliance: the substrate, pre-treatment, coating build, curing, inspection and supporting documentation must all align with the relevant standard, regulation or customer requirement.
Regulations and standards have different roles. Regulations are legal requirements, while standards are usually technical methods or performance benchmarks used to define and verify quality. A project specification may require a particular corrosion category, chemical resistance, surface appearance, colour reference or test method. In other cases, a coating may need to support wider obligations relating to restricted substances, workplace handling, product safety or sector-specific approvals. The correct powder colour paint therefore depends on the end use rather than colour preference alone.
Colour can have a compliance function as well as an aesthetic one. Components may need a specified colour for identification, warning markings, equipment grouping, architectural control or consistency across an installation. A recognised colour reference should be agreed before production, together with acceptable tolerances for shade, gloss and texture. This is particularly important where coated parts from different batches will be assembled together or compared with existing equipment.
For regulated or tightly specified applications, the coating supplier’s technical documentation should be reviewed before approval. Relevant information may include:
- the powder’s technical data sheet and recommended application conditions;
- the intended service environment and limitations of use;
- available evidence for adhesion, hardness, corrosion or chemical resistance;
- information about restricted substances and applicable material declarations;
- recommended film thickness, curing requirements and inspection methods; and
- storage, handling and safety information for the coating material.
Where UK REACH, GB CLP, RoHS or another sector-specific requirement is relevant, the responsibility should be assigned clearly between the coating manufacturer, applicator, component manufacturer and end customer. A powder coating cannot be described as compliant with every regulation simply because it is a powder product. The specific formulation, application and finished component must be assessed against the requirement in question. For food-contact, electrical, medical or other controlled uses, the relevant declaration or approval must relate to that application and not merely to the colour or coating type.
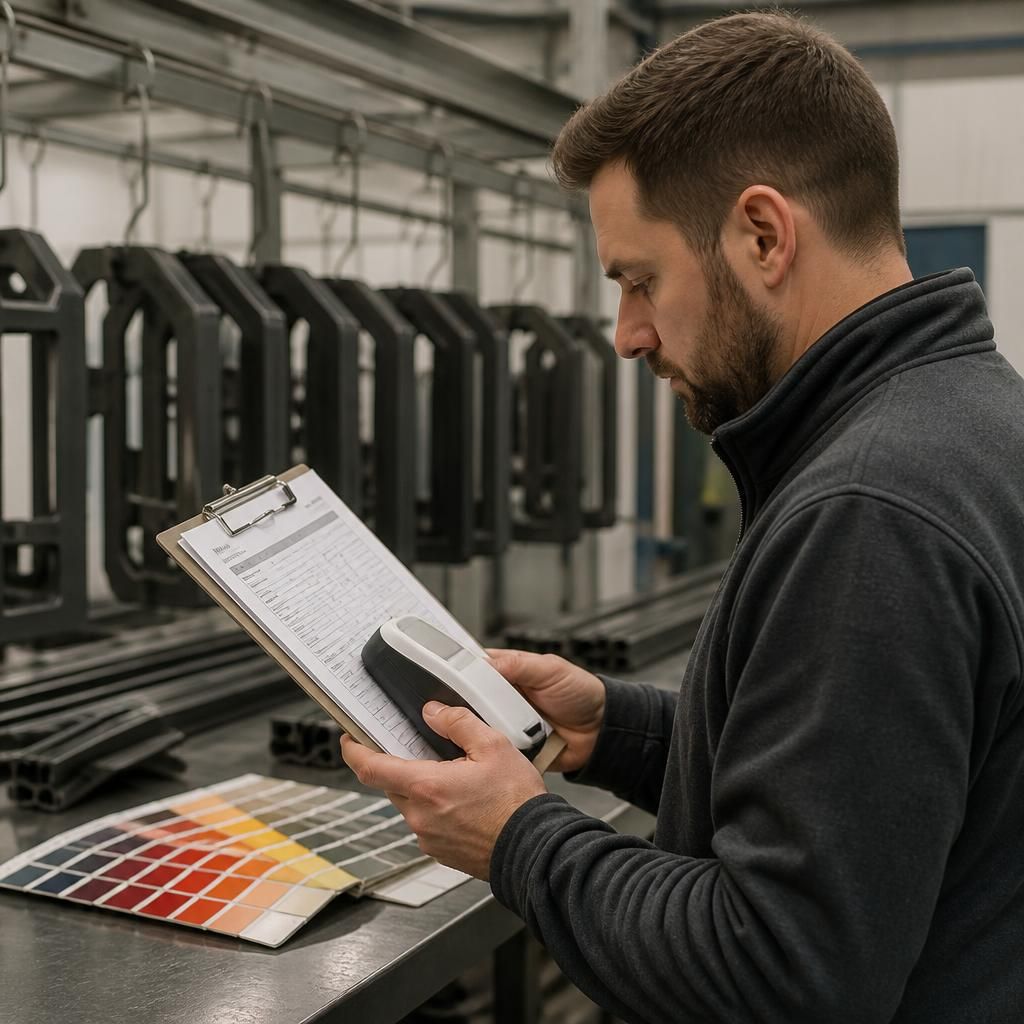
Evidence and traceability are central to demonstrating compliance. A suitable quality record can link the finished part to the powder product, colour reference, batch information, coating specification and inspection results. Retaining this information helps establish what was applied and whether the finished work was assessed against the agreed acceptance criteria. It also makes non-conforming work easier to investigate without relying solely on visual judgement.
Acceptance criteria should be agreed before production begins. These may cover permitted colour variation, gloss level, texture, visible defects, edge coverage, film thickness and the extent of any repair. Visual inspection should be carried out under consistent conditions, because lighting, viewing distance and surrounding colours can affect how a shade is perceived. Where the specification requires instrumental colour measurement or physical testing, those methods should be defined in advance rather than introduced after a disagreement.
Powder colour paint also needs to be considered as part of the component design. Sharp edges, recesses, welds, threaded areas, contact points and areas subject to assembly damage can affect the final result and the suitability of the finish. Masking, racking and grounding arrangements may be needed to keep critical interfaces free from coating. If a component forms part of a safety-critical or fire-rated assembly, the coating should not be assumed to provide that performance unless the complete system has the necessary evidence.
A practical compliance review should therefore confirm:
- which legal requirements, recognised standards and customer specifications apply;
- what the component will encounter during service, including weather, chemicals, abrasion, heat and cleaning;
- which colour, gloss, texture and appearance tolerances are acceptable;
- what technical evidence is required for the chosen coating system;
- how the finished work will be inspected and recorded; and
- which documents must be retained for handover, audit or future production.
For manufacturers and fabricators, discussing these points with the coating specialist before a batch is released reduces the risk of selecting a colour or formulation that looks correct but fails a technical requirement. Compliance remains the responsibility of the relevant parties and should be confirmed against the current project documentation, legislation and product information rather than inferred from the term “powder coating” alone.
Compliance must also be maintained when a coating specification changes. A different powder formulation, colour reference, gloss level or application method may require fresh technical review, even if the replacement appears visually identical.
For controlled production, treat the approved coating system as part of the component specification. Before making a change, check whether it affects the required performance, material declarations, curing conditions or inspection method. Record the reason for the change, obtain the relevant technical information and secure approval from the responsible parties where the project requires it.
This approach helps prevent an unrecorded substitution from separating later production from the evidence supporting the original approval. It is particularly relevant for repeat batches, outsourced coating work and components supplied into assemblies with documented technical requirements.