

What are the key indicators that a substrate is adequately prepared for electrostatic powder coating?
A substrate is adequately prepared for electrostatic powder coating when it is clean, dry and free from oil, grease, rust, loose scale, dust and other contaminants. Its surface should have a consistent profile appropriate to the metal and coating system, with any required chemical pre-treatment intact and the component suitable for effective electrical grounding.
The most reliable indication of adequate preparation is consistency: every accessible area of the component should show the intended surface condition, chemical treatment and electrical contact characteristics, rather than preparation being judged from one clean-looking face. Inspection should cover edges, welds, recesses, holes, joints and other areas where residues or surface defects are commonly retained.
Visual uniformity across the whole component is the first practical check. Under suitable lighting, the surface should have an even appearance appropriate to the preparation method. It should not show loose mill scale, blistering, visible corrosion products, embedded abrasive, weld spatter, burrs, sharp fins or remnants of an old coating. Dark patches, tide marks, powdery deposits or localised discolouration can indicate uneven treatment, trapped residues or differences in the underlying metal.
The surface profile should be consistent rather than irregular. A prepared surface with isolated deep scratches, polished areas or excessive roughness may produce variable powder coverage and adhesion. Profile checks should be taken from representative areas, including locations affected by welds, bends and fabrication marks. The selected profile must suit the substrate and the powder system; an aggressive profile is not automatically a better one.
Chemical pre-treatment should appear continuous and free from deposits. Where a conversion coating or other chemical stage is specified, there should be no visible streaking, patchiness, powdery residue or crystalline build-up after the final rinse and drying stages. Process controls such as bath condition, rinse quality and, where appropriate, conductivity or pH checks provide stronger evidence than appearance alone. The correct assessment depends on the metal, the pre-treatment chemistry and the powder coating specification.
Water behaviour can reveal localised surface problems. On a suitably prepared area, a water film should spread evenly rather than retracting into isolated beads or breaking into separate patches. A water-break test is only one indication and should be used with the appropriate precautions for the substrate and process. It does not replace inspection for salts, chemical residues or surface damage that may not be visible during the test.
There should be no contamination in difficult-to-reach areas. Fabricated components can retain cutting fluid, polishing compound, blasting dust or treatment chemicals in seams, folded sections, blind holes and threaded features. Evidence of adequate preparation includes clean internal surfaces where coating is required, clear drainage paths and no residue emerging from cavities during handling or heating. Components with enclosed sections also need suitable venting and drainage to prevent retained chemicals or air from affecting the coating process.
Welded and fabricated areas require particular scrutiny. Weld spatter, slag, sharp weld edges and porous or contaminated welds can interrupt the coating film. Welds should be suitably finished, and any fabrication defects that could lead to outgassing or pinholing should be addressed before coating. Sharp edges may also receive less powder coverage than adjacent faces, so edge condition is part of the preparation assessment, not merely a cosmetic concern.
Masking and contact points should be correctly defined. Threaded holes, bearing seats, machined faces, earth points and dimensional datum surfaces may need masking or plugging before treatment and coating. Masking should be secure, compatible with the process and positioned consistently. At the same time, the areas used to hang and electrically ground the component must provide reliable metal-to-metal contact. Paint, powder, heavy residue or unsuitable masking at these points can interfere with electrostatic application.
Handling should not undo the preparation. Prepared parts should be protected from contact with bare hands, dirty gloves, oily benches, unsuitable packaging and airborne dust. Fresh marks, fingerprints or handling deposits after inspection are signs that the preparation condition may no longer represent the condition at the point of coating. Clean racks, appropriate handling equipment and controlled transfer between stages help preserve the result.
For critical or repeat work, recorded checks are preferable to visual judgement alone. Useful records may include the preparation method, abrasive or chemical process used, inspection results, treatment-bath readings, profile measurements, masking details and any deviations found. A test panel or sample component can also help confirm that the preparation and powder system are compatible before a production batch is processed.
In practice, a substrate is ready when inspection confirms an even and suitable surface condition throughout, fabricated areas have been dealt with, cavities and contact points are controlled, the specified pre-treatment has been verified, and the component can be handled and electrically connected without compromising the preparation. If any of these checks gives an inconsistent result, the cause should be corrected before powder application rather than concealed by the coating.
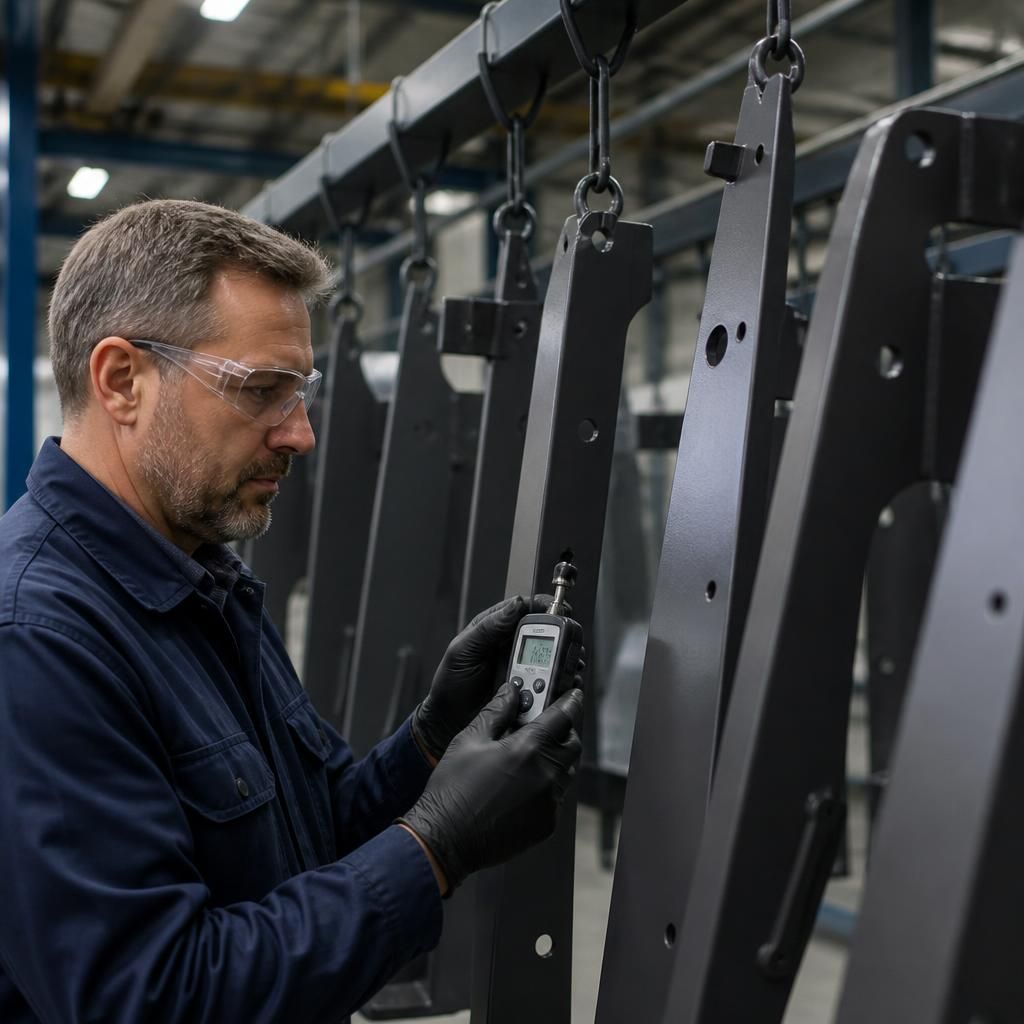
A further indicator of adequate preparation is verified dryness immediately before powder application. A surface can appear clean while still carrying a thin moisture film or condensation, particularly after rinsing, storage in a humid area or movement between different temperatures. The component temperature should be assessed against the surrounding dew point, with coating postponed or drying continued if condensation could form.
Drying checks should include recesses, seams, hollow sections and porous cast surfaces, where water may remain after the main faces look dry. Drainage and orientation should allow retained moisture to escape, while clean, dry air can help remove surface water where appropriate. For repeat work, recording the drying method and relevant environmental or surface-temperature checks provides stronger evidence than appearance alone.