

What are the key considerations for resurfacing or repainting projects where epoxy and polyester powder coatings are involved?
Resurfacing or repainting with epoxy or polyester powder coating depends on thorough substrate preparation, compatibility with the existing finish, the component’s service environment and the required appearance and durability. The coating system, surface profile, application method and curing requirements should be assessed together so the new finish bonds correctly and performs as intended.
Resurfacing or repainting a powder-coated component is primarily a decision about whether the existing finish can be retained, partially removed or taken back to bare metal before a new epoxy or polyester system is applied. The correct approach depends on the condition of the old coating, the metal beneath it, dimensional tolerances, the intended service conditions and the inspection standard required after recoating.
Assess the existing finish before choosing the treatment. A sound, firmly attached coating may sometimes be overcoated after suitable preparation, whereas blistering, peeling, widespread corrosion, contamination or loss of adhesion usually indicates that the old finish should be removed. Coating that is already separating from the substrate can undermine the new layer, even if the new powder appears sound immediately after application. Isolated damage may be treated differently from a component with general coating failure, but the decision should be based on the extent and cause of the defect rather than appearance alone.
Inspect the substrate once the condition is understood. Look for rust, pitting, weld contamination, sharp edges, dents, distortion and damage around fixing holes or joints. Corrosion beneath the original coating may be more extensive than it first appears. Aluminium, galvanised steel and other substrates can also require different preparation methods. Any repairs, weld dressing or metalwork should be completed before coating, because powder coating will reproduce significant surface irregularities rather than conceal them.
Decide how much of the old coating should be removed. Options can include mechanical preparation, controlled blasting, chemical stripping or complete removal by a specialist process. The method must suit the substrate and the component’s geometry. Excessive abrasion can alter dimensions or soften edges, while aggressive treatment can damage thin sections, threaded areas or heat-sensitive components. Where a coating is removed completely, the newly prepared metal should be protected from contamination and handled in a way that does not compromise the subsequent finish.
Consider areas that must remain uncoated. Masking may be needed for threads, bearing seats, electrical contact points, earth points, hinge faces, drainage paths and close-tolerance interfaces. Powder thickness can affect assembly, fastener engagement and moving parts. The masking specification should therefore be agreed before processing, particularly where the component forms part of a larger manufactured assembly.
Check the design for coating access and drainage. Enclosed sections, overlapping joints, narrow recesses and internal corners can retain preparation residues or create areas that are difficult to coat consistently. Drainage and vent holes may be needed on hollow fabrications to reduce the risk associated with trapped moisture or gases during processing. Components should also be presented so that powder can reach the relevant faces and so that contact points used for electrical grounding do not leave unacceptable bare areas.
Set a clear finish specification. “Repainted” does not by itself define the required result. The specification should identify the colour reference, gloss level, texture, acceptable variation, edge coverage and any areas where a different finish is required. A repair or respray may not match an aged surrounding finish exactly, particularly where the original coating has faded, become contaminated or changed gloss during service. For visible assemblies, it is sensible to establish how adjacent parts will be judged together rather than assessing each component in isolation.
Choose epoxy or polyester according to the component’s exposure. Epoxy powder coatings are commonly selected where adhesion and resistance to chemicals or corrosion are important but prolonged direct ultraviolet exposure is limited. Polyester powder coatings are generally more appropriate where colour and gloss retention in exterior or light-exposed service are important. Hybrid systems may be considered for some indoor applications. The choice should reflect the actual exposure, cleaning regime and functional requirements, not simply the resin name on the previous coating.
Account for heat-sensitive or assembled parts. Powder application involves a controlled heating stage, so the suitability of seals, plastics, adhesives, electronics, lubricants and dissimilar materials must be checked. Parts that cannot tolerate the required process may need to be removed, masked or treated by another method. Heating can also reveal trapped moisture, oils or gases in porous castings and fabricated sections, creating surface defects in the new finish.
Plan the work around the component’s dimensions and handling points. Racks, hooks and contact marks are unavoidable considerations in powder coating. Their position should be chosen where small marks will be hidden, subsequently machined or kept away from functional surfaces. Large or awkward components may need additional support to prevent movement, sagging or contact during processing. The component’s dimensions should be checked before and after coating where close fits or assembly alignment matter.
Define inspection and acceptance criteria in advance. A practical inspection may include checks for coverage, colour, gloss, texture, runs, pinholes, craters, inclusions, edge defects and visible contamination. Adhesion or thickness checks may be appropriate where the specification requires evidence of performance. Any test method should take account of the substrate and whether testing could damage a finished face. Photographs, coating details, preparation records and non-conformance decisions can help maintain consistency across repeat batches.
Consider whether a repair or full refurbishment is more appropriate. Local touch-up can be suitable for minor handling damage or a limited defect, but it may not provide the same appearance or properties as a fully applied powder coating. A complete strip and recoat is more disruptive, yet may be preferable where defects are widespread, the original coating is failing or the component has accumulated several previous layers. The decision should include preparation, masking, transport, reassembly and any required machining rather than focusing only on the coating operation.
For a planned project, provide the coater with the substrate type, component drawings or critical dimensions, previous coating information where known, service exposure, colour and gloss requirements, masking points, acceptable repair limits and the required inspection standard. For businesses across the Midlands and surrounding areas, a coating specialist can also advise on collection and delivery arrangements when components need to be processed as batches or as part of a wider refurbishment programme.
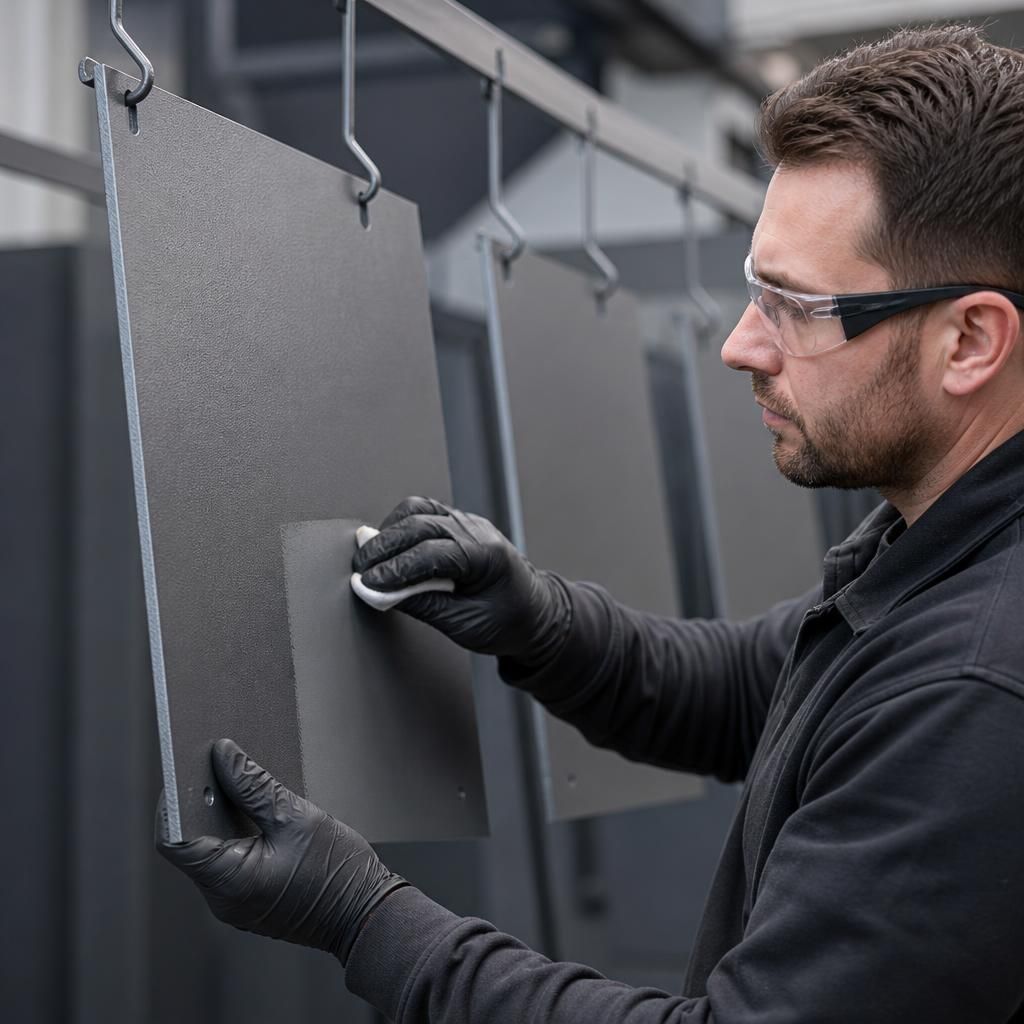
Where the existing powder coating is being retained, a small trial area can help verify that the proposed preparation and new coating are compatible before the whole component is processed. The trial should be assessed for wetting, visible defects, adhesion and the appearance of the cured finish. This is particularly useful when the original resin type, cleaning history or service exposure is unknown.
A successful trial does not remove the need to prepare the full component consistently. Its value is in identifying problems such as poor bonding, lifting, surface contamination or an unacceptable change in gloss before they affect a complete batch. The trial result, preparation method and coating specification should be recorded as part of the project documentation.