

What safety standards and certifications should be considered when selecting protective powder coating services?
When selecting protective powder coating services, consider documented quality controls, suitable surface-preparation procedures, traceability of materials and batches, and compliance with relevant health, safety and environmental requirements. Any certifications should be current, independently verifiable and relevant to the coating process, substrate, service environment and performance specification required for the project.
The most relevant standards and certifications when selecting protective powder coating services are those that verify the applicator’s management systems, the coating system’s technical performance and the controls used to protect people and the environment. The correct evidence depends on the substrate, operating conditions, required service life and any regulatory requirements applying to the finished component.
Start by separating three types of evidence:
- Applicator certification: demonstrates that the coating company operates an assessed management or specialist application system.
- Product approval: relates to the powder coating material, its intended substrate and its tested performance.
- Project performance evidence: confirms that the proposed coating build-up is suitable for the actual environment, preparation method and component design.
An organisation certified to ISO 9001 has a quality management system assessed against an internationally recognised standard. This can be useful when repeatability, controlled inspection and formal handling of non-conforming work are important. Check the certificate’s scope rather than accepting the logo alone: it should cover relevant coating or metal-finishing activities, not an unrelated part of the organisation.
ISO 14001 may be relevant where environmental management is a procurement requirement. It addresses the way an organisation identifies and manages environmental aspects such as energy use, emissions, waste and resource consumption. ISO 45001 concerns occupational health and safety management. Neither standard proves that a particular component will resist corrosion, but both can provide useful evidence that wider operational risks are managed systematically.
For architectural aluminium and other specialist applications, sector schemes such as Qualicoat or GSB approval may be relevant where the project specification requires them. These schemes can include requirements for approved materials, application controls, testing and ongoing assessment. They should not be treated as universally necessary: their suitability depends on the substrate, sector and specification. A scheme certificate should identify the certified site and the scope of work, rather than merely naming an organisation that may have several locations or activities.
For steelwork and galvanised steel, BS EN 13438 can be relevant to powder coatings used on components intended for architectural, industrial or similar applications. For aluminium, BS EN 12206-1 may be relevant to the coating of aluminium and aluminium alloys used in construction. The applicable standard should be confirmed against the component and end use, because a coating designed for one substrate is not automatically suitable for another.
Corrosion protection is often specified using BS EN ISO 12944. This standard helps classify the corrosivity of the service environment, such as indoor, rural, industrial, coastal or marine exposure, and supports selection of an appropriate paint or powder coating system. It is not, by itself, a certificate for an applicator. The specification should identify the corrosion category, expected durability range, substrate preparation, coating type and dry-film requirements. For duplex systems involving galvanising and powder coating, the interface between the two layers also needs to be specified and controlled.
Test reports can add useful evidence, but the test method and interpretation matter. Depending on the application, relevant testing may include:
- neutral salt spray testing to BS EN ISO 9227;
- resistance to humidity or condensation exposure to BS EN ISO 6270;
- adhesion testing using cross-cut methods under BS EN ISO 2409 or pull-off methods where appropriate;
- flexibility or bending tests to assess whether the coating withstands forming or handling;
- gloss measurement to BS EN ISO 2813 where appearance is part of the acceptance criteria; and
- impact, abrasion, chemical-resistance or heat-resistance testing where the component’s working environment demands it.
A laboratory result should be read as evidence for the tested formulation, substrate, film thickness, preparation and exposure conditions. Salt-spray hours, for example, should not be treated as a direct prediction of outdoor service life. Ask whether the report relates to the proposed powder, substrate and coating build-up, and whether it was produced by a competent independent laboratory or under a recognised internal procedure.
Building, transport and electrical applications can introduce additional requirements. Where coated products form part of a construction assembly, fire classification under BS EN 13501-1 may need consideration, although the required classification applies to the relevant finished product or system rather than automatically to every powder coating. Components used for electrical insulation may require electrical withstand, insulation resistance or tracking tests to the relevant product standard. Automotive and safety-critical manufacturers may also impose their own supplier approval, process-audit and material documentation requirements.
Regulatory compliance is separate from voluntary certification. A responsible coating process should account for requirements such as UK REACH, safety data sheet controls, COSHH duties, waste management and the risks associated with combustible dust. Powder application equipment and extraction systems may also need to be assessed against explosive-atmosphere risks under the Dangerous Substances and Explosive Atmospheres Regulations. Ask how these obligations are addressed, but do not assume that an ISO certificate replaces the legal duties applying to the workplace or supplied product.
Before appointing a provider, request the certificate number, issuing or accreditation body, validity dates and certified scope. For the proposed coating, request the technical data sheet, safety data sheet, recommended film thickness, curing conditions, substrate limitations and relevant test evidence. For a project with demanding corrosion or safety requirements, the coating specification should also state the acceptance tests, inspection points, repair method and the documents that will accompany each batch or delivery.
The strongest selection is therefore not the company displaying the greatest number of logos. It is the provider that can connect an appropriate, current certification or approval with the actual coating system, substrate, environmental classification and acceptance criteria for the work. For Midlands manufacturers, fabricators and construction or automotive businesses, a specialist powder coater should be able to discuss those links clearly and identify where the design authority, material manufacturer or end-product standard retains responsibility.
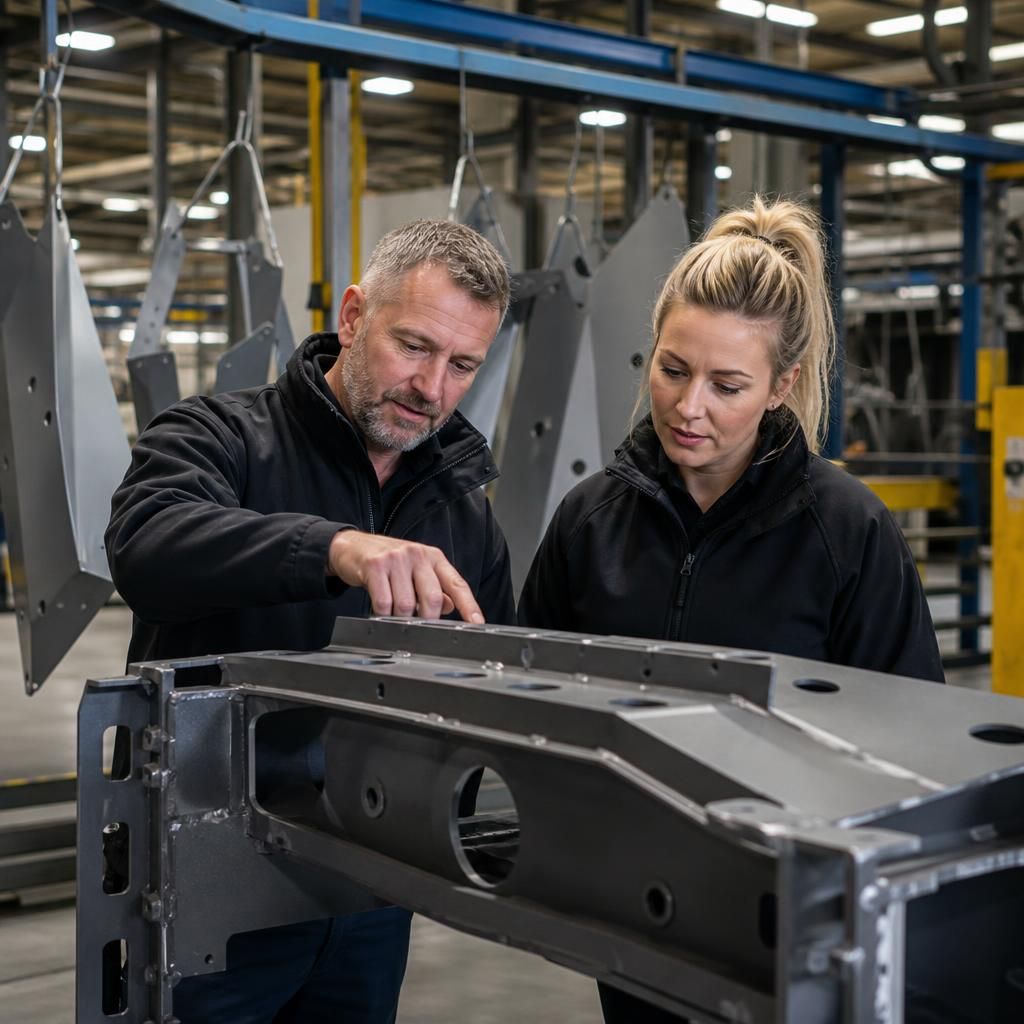
Safety standards are only useful when they are translated into clear, component-specific acceptance criteria. During technical review, assess whether the part’s design allows the specified coating system to be applied consistently and inspected properly.
- Identify edges, recesses, joints, welds and enclosed sections that may receive uneven coverage or retain contaminants.
- Confirm masking requirements for threads, bearing surfaces, electrical contact points and other areas where coating could affect assembly or function.
- Check that drainage and venting provisions are suitable for the preparation and curing process, particularly on hollow or fabricated components.
- Agree permissible film-thickness variation, appearance limits, exposed-metal tolerances and the treatment of small defects before production begins.
- Define how damage caused during handling, transport or installation will be assessed and repaired without undermining the specified protection.
This design-stage review helps distinguish a certificate that demonstrates general process control from evidence that the proposed coating can meet the component’s actual safety, performance and inspection requirements.
Discuss Your Protective Powder Coating Standards and Certification Requirements
Discuss your component, service environment and required acceptance criteria with Powder-coatings.co.uk to identify the relevant certification and test documentation for your project. This helps establish a clear coating specification before production begins.