

What impact does substrate geometry have on the effectiveness of electrostatic coating preparation?
Substrate geometry directly affects electrostatic coating preparation because recesses, internal corners, narrow gaps and complex profiles can restrict access for cleaning, rinsing and drying, while edges and projections alter the electric field. These features can create Faraday-cage areas that receive less powder, so preparation and coating specifications must account for the part’s shape, access points and required coverage.
Substrate geometry affects preparation effectiveness by determining how completely every surface can be contacted, treated, drained and inspected. A coating system may be correctly specified, yet still perform inconsistently if the component’s shape creates unprocessed areas, retains treatment residues or produces local differences in surface condition. Geometry therefore needs to be considered when selecting the preparation sequence, racking method and inspection plan, not only when setting the powder application parameters.
Surface accessibility and process contact
Flat, open surfaces are generally straightforward to expose to the stages of a preparation line. Three-dimensional parts are more demanding because the treatment medium must reach faces that are angled away from the spray pattern or partly shielded by adjacent features. Brackets, folded sections, channels, frames and assemblies with overlapping members can contain partially enclosed zones where the cleaning or conditioning action is weaker than on the outer face.
This can result in a variable starting condition across one component. An exposed face may be fully degreased and chemically conditioned while a sheltered face retains oil, oxides or residues from fabrication. The risk is higher where surfaces meet at tight internal angles or where one part is close to another. A preparation specification should therefore identify all coated faces and confirm that the chosen equipment can make effective contact with them.
Holes, cavities and hollow sections
Holes and enclosed sections require particular attention because liquids can enter without leaving readily. If a component is immersed or subjected to wet spray treatment, a cavity may collect cleaner, rinse water or conversion-coating solution. Unless the part is oriented to allow drainage, residues can remain after the visible outer surface appears dry. These residues may interfere with adhesion, contribute to staining or create defects during heating.
Drainage holes, access openings and suitable orientation can make a substantial difference. Hollow fabrications should be reviewed to establish whether internal surfaces are intended to be coated, whether they can be adequately treated and whether trapped liquid can escape. Where a cavity cannot be reliably prepared, the coating requirement may need to be limited to accessible external surfaces or the design may need modification before production.
Racking and part orientation
Geometry also determines how a component can be supported during preparation. Contact points are necessary for handling and electrical continuity, but they occupy small areas that may receive less treatment or remain uncoated. The contact position should be chosen on a non-critical area where possible, while still providing secure support and a suitable route for the coating process.
Orientation should allow liquid to run away rather than pool in corners, seams or upturned channels. Large panels, deep trays and fabricated boxes may need different orientations at different stages, or a fixture designed to hold them at an angle. The selected method should be assessed across the full process rather than only at the cleaning stage, since a position that drains well may not provide the best access for subsequent coating.
Edges, corners and transitions
Edges and corners are geometrically significant because they are the points where two surfaces meet and where material thickness or curvature can change abruptly. Sharp edges can be difficult to prepare uniformly and may be more susceptible to a thinner final film than broad faces. Burrs, rolled edges, weld spatter and rough cut-outs can also interrupt the continuity of the prepared surface.
Mechanical finishing before chemical preparation is often important for these features. Removing burrs and loose weld deposits gives the treatment stage a more consistent surface to work on. Where the design permits, a small radius or smoother transition is easier to prepare and coat than a sharp, irregular intersection. This is a design-for-coating consideration as much as a line-process consideration.
Geometry and retained contamination
Fabricated components often contain joints, laps, seams and threaded features. These can retain cutting fluids, grinding dust, weld residues or moisture even after the main surfaces have been cleaned. A seam that is partly closed may behave differently from an open joint, while a threaded hole can hold contamination in its flanks and alter the usable depth of the coating.
Such features should be identified before preparation so that they can be cleaned, protected or excluded from the coating requirement as appropriate. Masking may be needed for threads, precision bores, mating faces and drainage paths. Masking must itself be compatible with the preparation process; an unsuitable mask can prevent treatment from reaching an area that requires protection or leave residue on an adjacent surface.
Effect on chemical treatment
Complex geometry can alter the renewal of solution at the surface. Recesses and narrow passages may receive less fresh treatment medium, while enclosed areas may have a different exposure time from open faces. In a multi-stage process, this can produce variations in cleaning, rinsing and conversion treatment if the component moves through the line without allowing adequate drainage between stages.
Process selection should take account of the component’s size, orientation, openings and surface area. Spray systems need suitable nozzle access and coverage; immersion systems need controlled movement, drainage and, where relevant, agitation. The objective is not simply to expose the component to each stage, but to ensure that the process conditions are effective over the surfaces that must be coated.
Influence on drying and inspection
Geometry affects drying because water and preparation residues collect in low points, blind holes, folded returns and internal corners. A part can appear dry externally while retaining moisture in a recess. These areas should be examined before powder application, with particular attention to holes, seams, underside features and areas hidden by fixtures.
Inspection should follow the component’s geometry rather than rely only on viewing the most accessible face. Suitable checks include looking for visible oil or residue, confirming that critical areas are dry, and examining difficult features under appropriate lighting. Where the geometry is repeatable, inspection points and orientation instructions can be built into the work specification to reduce variation between batches.
Design and preparation recommendations
- Provide access openings or drainage routes where hollow sections or enclosed features are unavoidable.
- Avoid unnecessary narrow gaps, unsealed overlaps and pockets that can retain treatment liquids or contaminants.
- Remove burrs, sharp fabrication defects, weld spatter and loose residues before the chemical preparation stage.
- Define which faces, bores, threads and internal areas require coating and which must be masked or protected.
- Agree fixture contact points and component orientation before production, considering cleaning, rinsing, drying and coating together.
- Use a representative trial component when a design contains deep recesses, unusual profiles or partly enclosed sections.
In practice, the most reliable preparation plan is geometry-specific. The component drawing or sample should be reviewed for access, drainage, contact points, contamination traps and inspection limitations before the treatment route is finalised. This approach helps ensure that preparation is consistent across the whole coated area, rather than optimised only for the surfaces that are easiest to reach.
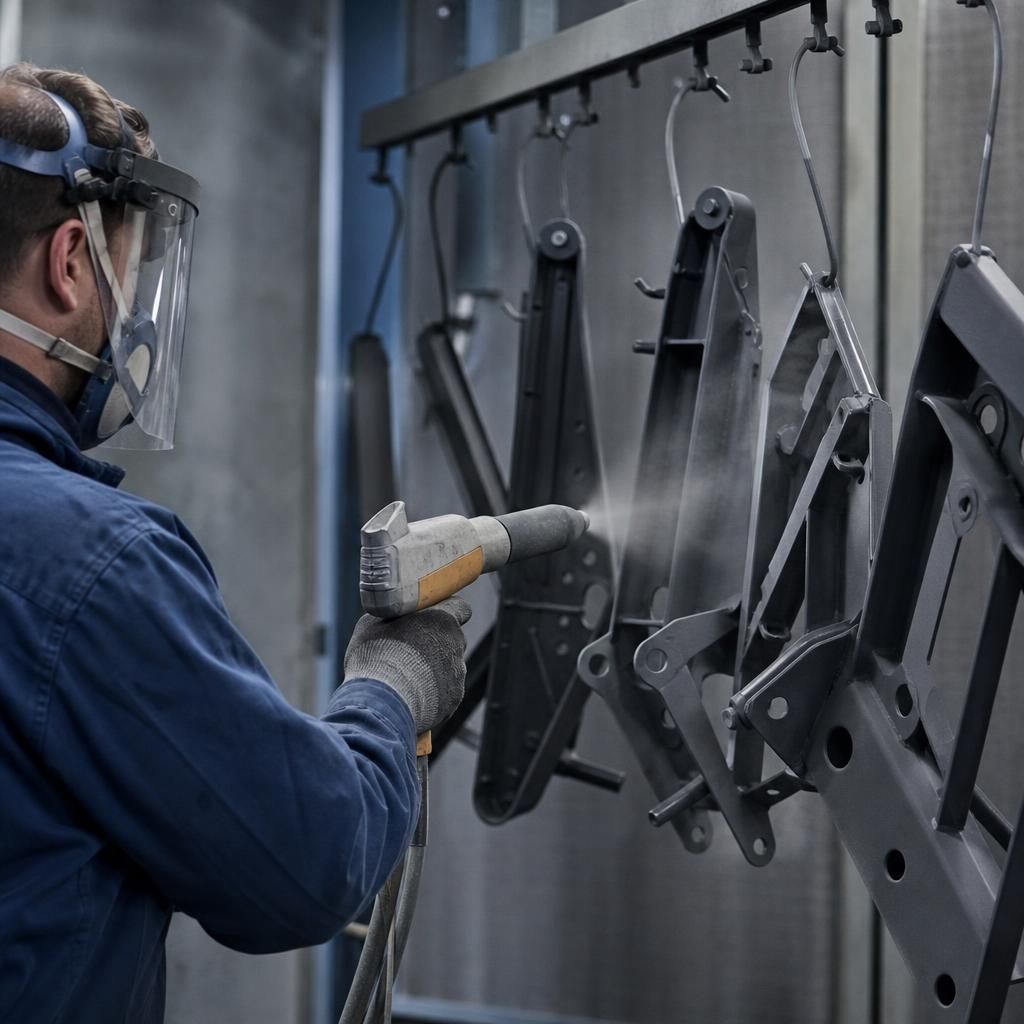
Complex geometry cannot usually be corrected by increasing electrostatic application voltage alone. Higher voltage may intensify powder attraction to exposed projections while doing little to improve penetration into shielded recesses, and excessive charge can contribute to back-ionisation or an uneven film. The preparation specification should therefore be assessed alongside the intended application settings, rather than treating electrical adjustment as a substitute for suitable access.
For critical components, separate the coating requirement into exposed faces, recessed areas and edges, then define the acceptable finish for each zone. This helps determine whether the geometry is suitable for a standard electrostatic process or whether certain surfaces require a different application approach, additional process development or exclusion from the coating requirement. A cross-sectional review of the part drawing is often useful because it reveals hidden surfaces that may not be apparent from an external view.