

What preparatory steps are essential for ensuring optimal adhesion and effectiveness of anti-corrosion coatings on steel surfaces?
Optimal adhesion and corrosion protection depend on removing contaminants, rust and mill scale from the steel before coating. The surface should then be thoroughly dried, given an appropriate profile for mechanical keying, and checked for cleanliness and defects so the anti-corrosion coating can form a continuous, well-bonded film.
Effective preparation for an anti-corrosion coating is a controlled process that covers the steel’s condition, fabrication quality, surface chemistry, environmental conditions and coating specification. The objective is not simply to make the metal look clean; it is to provide a stable, compatible substrate on which the complete coating system can perform as intended.
Start with a condition and specification review. Identify the steel grade, previous service exposure, intended environment and required durability before selecting the preparation method. Consider whether the component will face outdoor weathering, condensation, immersion, road salts, chemicals or abrasion. The preparation standard, coating type, film thickness and any primer or topcoat should be agreed as one system, because a preparation method suitable for one product may not be suitable for another.
- Check drawings and coating specifications for required areas, thicknesses, masking zones and inspection requirements.
- Confirm whether the steel has previously been painted, galvanised, oiled or chemically treated, as existing finishes may require specialist assessment or complete removal.
- Establish whether concealed faces, joints, contact points and internal sections can be prepared and coated adequately.
Resolve fabrication defects before preparation. Coating cannot compensate for poor steelwork design or inaccessible corrosion traps. Weld spatter, sharp projections, burrs and poorly finished welds can create thin spots or discontinuities in the coating. Welds should be continuous and suitably dressed where the specification requires it. Sharp external edges generally need rounding or edge treatment so that the coating can cover them consistently rather than pulling away from the apex.
Crevices, unsealed overlaps and narrow gaps deserve particular attention. They can retain moisture and preparation residues, allowing corrosion to begin beneath an otherwise sound-looking finish. Where the design permits, improve drainage, seal suitable joints and provide access for preparation and inspection. Components should also be arranged so that hooks, racks or lifting points do not leave uncoated areas in critical positions.
Control residues that are difficult to see. Soluble salts, abrasive dust, detergent traces and handling marks can remain after visible preparation and interfere with coating adhesion or accelerate under-film corrosion. Where service conditions justify it, use appropriate testing to verify that the substrate is within the coating specification’s limits. Do not handle prepared steel with contaminated gloves, slings or work surfaces, and keep prepared parts protected from rain, condensation and airborne process residues.
Use suitable preparation equipment and materials. Abrasives must be clean, dry and appropriate for the steel and the selected coating system. Recycled or contaminated abrasive can transfer unwanted material back onto the surface. Equipment should be maintained so that pressure, nozzle condition and media flow remain consistent across the component. Large parts may need a planned sequence to prevent prepared areas being marked or recontaminated while other sections are being worked on.
Where chemical cleaning or conversion treatments are specified, residues must be removed in accordance with the product instructions. Inadequately controlled chemical treatment can leave a film that affects bonding just as readily as oil or dust. The preparation method should therefore be documented, including the equipment, materials, sequence and any acceptance checks relevant to the coating system.
Manage the surrounding conditions. Steel temperature, air temperature, relative humidity and the condition of the workshop or preparation area all influence the time available between preparation and coating. The steel must remain sufficiently above its dew point to prevent invisible condensation forming. If the prepared surface begins to show discoloration, corrosion staining or other change before coating, stop and reassess it rather than coating over the change.
Parts should be supported and handled in a way that avoids contact damage. Clean lifting equipment and suitable gloves reduce the risk of recontamination. Preparation should be coordinated with masking and racking requirements, especially where threads, machined faces, bores, electrical contact points or dimensional interfaces must remain free of coating.
Inspect before the coating is applied. A useful pre-coating inspection checks more than general appearance. It should confirm that:
- the required preparation method has been completed consistently;
- welds, edges, corners and difficult-to-reach areas are acceptable;
- the surface is free from visible dust, oil, moisture and preparation residue;
- masking and hanging arrangements will not compromise critical surfaces;
- environmental readings are suitable for the specified product; and
- any flash corrosion, handling damage or recontamination has been corrected.
For demanding applications, record the preparation and inspection results as part of the job documentation. Test pieces or trial panels can help confirm that the chosen preparation, coating chemistry and curing process are compatible before a full production batch is processed. This is particularly useful where the component geometry is complex, the exposure is severe or more than one coating layer is required.
Finally, apply the coating within the specified recoat or preparation window and follow the product requirements for mixing, application and curing. The most reliable results come from treating preparation as part of the complete corrosion-control system: sound fabrication, controlled surface treatment, suitable environmental conditions, verified cleanliness and a coating specification that matches the steel’s service conditions.
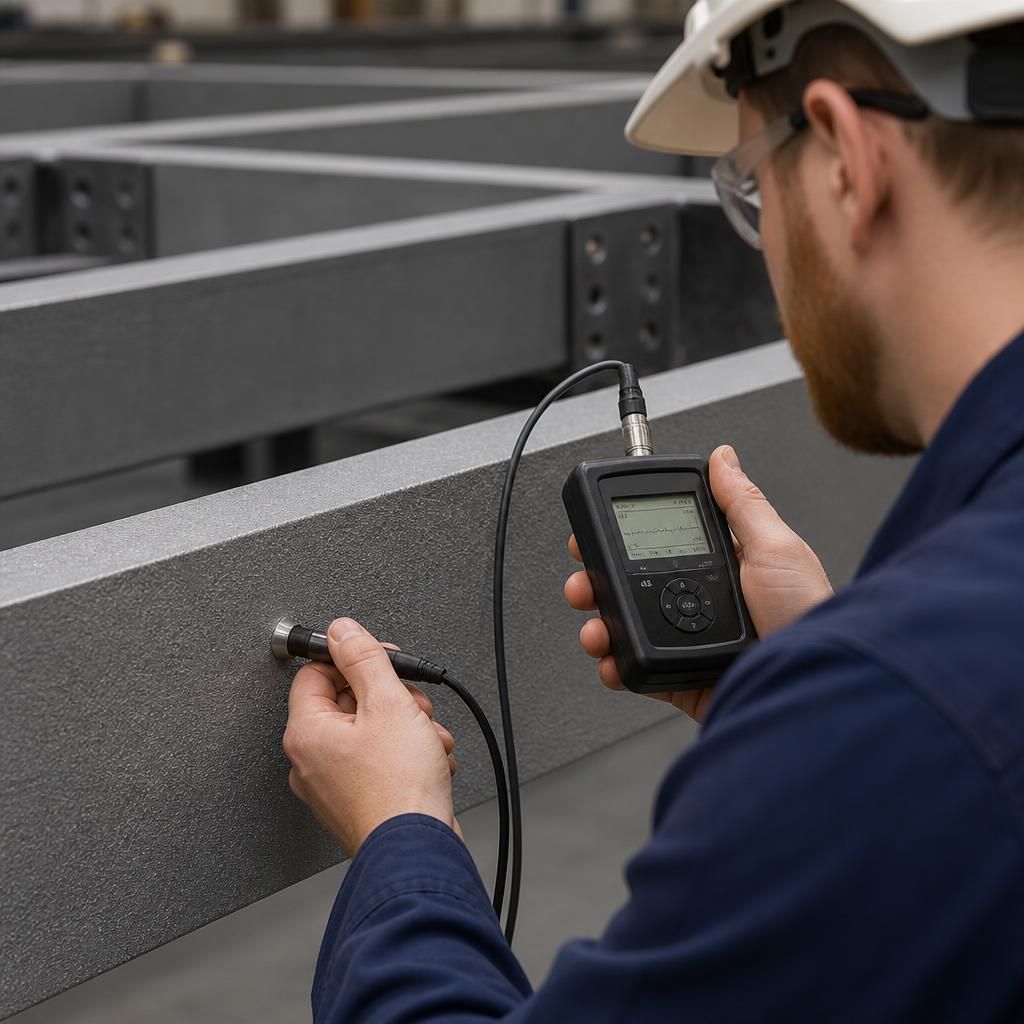
Surface profile should be verified as well as created. The texture left by blasting or mechanical preparation must suit the specified anti-corrosion coating: an insufficient profile may limit mechanical adhesion, while an excessively coarse profile can leave coating peaks under-protected if the applied film does not cover them adequately. Check representative areas using an appropriate profile comparator or measuring instrument, particularly on large or complex steelwork, and confirm that the recorded result falls within the coating specification before application.
Discuss your steel surface preparation requirements
Discuss your steel surface preparation requirements with our team to review the component condition, coating specification and inspection needs before processing. We can help identify the preparation approach suitable for your anti-corrosion coating system.