

What safety and regulatory standards should be considered when selecting a zinc primer powder coating for industrial use?
When selecting a zinc primer powder coating for industrial use, check the product’s safety data sheet and technical data against UK REACH, COSHH, workplace exposure controls and applicable waste requirements. The coating system should also meet the relevant project specification—such as corrosion-protection standards for the intended environment—while the application process should address combustible powder risks under DSEAR and any applicable ATEX controls.
A zinc primer powder coating should be selected against the complete coating system, the exposure environment, the metal substrate and the obligations applying to the finished component. The key evidence is not simply that the product contains zinc, but that the specified primer has been tested for its intended use, is compatible with the subsequent topcoat and can be applied and verified consistently.
Relevant standards for corrosion protection
For steelwork, BS EN ISO 12944 is a central reference. It provides a framework for classifying corrosivity, selecting protective paint systems and assessing laboratory performance. The correct system depends on factors such as moisture, salt exposure, pollution, immersion, condensation and the expected maintenance conditions. A zinc primer suitable for a dry internal component should not automatically be specified for an exposed structural part or a coastal installation.
BS EN ISO 12944-5 can help compare coating-system types and expected durability categories, while BS EN ISO 12944-6 covers laboratory performance testing. These standards should support, rather than replace, a project-specific specification. Where the component will face particularly severe or specialist conditions, the relevant parts of the ISO 12944 series and the purchaser’s engineering requirements should be reviewed together.
It is also important to distinguish a zinc primer powder coating from hot-dip galvanising, sherardising or zinc electroplating. Those processes have different standards, thickness controls and service assumptions. A powder primer should therefore be specified as one layer within an organic coating system unless the project documentation explicitly requires another form of zinc protection.
Performance information to request
- Recommended substrate preparation and any limitations relating to steel grade, surface condition or existing contamination.
- Nominal and permitted dry-film thickness for the primer, together with the method used to measure it.
- Recoat or overcoat requirements, including the compatible topcoat chemistry and any maximum or minimum interval where relevant.
- Results from appropriate adhesion, corrosion, humidity and accelerated-exposure tests.
- Application and curing conditions, including the specified metal temperature and cure schedule.
- Batch identification, storage requirements and product shelf-life information.
Common test references include BS EN ISO 2808 for coating-thickness measurement, BS EN ISO 2409 for cross-cut adhesion and BS EN ISO 4624 for pull-off adhesion. Humidity resistance may be assessed using BS EN ISO 6270, while neutral salt-spray testing is covered by BS EN ISO 9227. These tests can provide useful comparative evidence, but a salt-spray result alone does not establish how a coating will perform in a particular outdoor or industrial environment. The test method, duration, preparation, film thickness and failure criteria should all be recorded.
System compatibility and design controls
Zinc-rich primers can affect the appearance, adhesion or curing of a subsequent powder layer if the complete system has not been validated. Selection should therefore consider the primer and topcoat together. The system specification should identify whether the topcoat is intended to be applied over a cured primer, whether the primer needs preparation before recoating and how edges, welds, recesses and areas of different thickness are to be treated.
Design details can be as important as the coating product. Crevices, sharp edges, unsealed joints and areas that retain water can create local corrosion conditions that a compliant coating cannot fully overcome. Drainage, access for preparation, avoidance of trapped contaminants and suitable edge treatment should be addressed before coating. Masking requirements for threads, electrical contact points, bearing faces and machined tolerances should also be defined.
Regulatory status of the finished component
The coating itself is not automatically subject to one universal approval for every industrial application. Additional requirements may apply because of the finished product, its location or its function. Construction products, structural components, equipment used in regulated installations and parts supplied into a controlled process may each have separate documentation or conformity obligations. The purchaser should confirm whether a declaration of performance, UKCA or CE-related evidence, or a project-specific approval is required for the complete component rather than assuming that a coating certificate meets that obligation.
Where the component is used in contact with drinking water, food, medical equipment, animal environments or other controlled applications, sector-specific restrictions may apply to the coating formulation and finished surface. The relevant end-use requirements should be identified before product selection, since general industrial suitability does not establish suitability for those applications.
Quality assurance and traceability
A robust specification should define how the coating will be accepted after application. Typical controls include visual inspection, dry-film thickness readings, adhesion checks where required, cure verification and inspection for pinholes, runs, inclusions or uncovered areas. Acceptance limits should be agreed in advance and should distinguish between isolated repairable defects and conditions requiring rework.
Traceability should link the coated component to the primer and topcoat batch numbers, preparation method, application records, cure data and inspection results. This is particularly important for batch-produced parts or components that will be incorporated into safety-critical, structural or difficult-to-access assemblies. Records should be retained in the format required by the purchaser’s quality system or project documentation.
Practical selection checklist
- Classify the service environment and identify the required durability level.
- Confirm the substrate, preparation standard and design features that could retain moisture or interfere with coating.
- Specify the complete primer-and-topcoat system rather than selecting the zinc primer in isolation.
- Check product technical evidence against the required test methods and acceptance criteria.
- Confirm any sector-specific conformity, contact or declaration requirements for the finished component.
- Agree thickness, curing, inspection, repair and traceability requirements with the applicator and end client.
For Midlands manufacturers and fabricators, these details can be incorporated into the coating brief before components are collected for processing. A clear brief gives the coating applicator the information needed to assess the intended system, identify compatibility issues and provide records that support the finished component’s technical file.
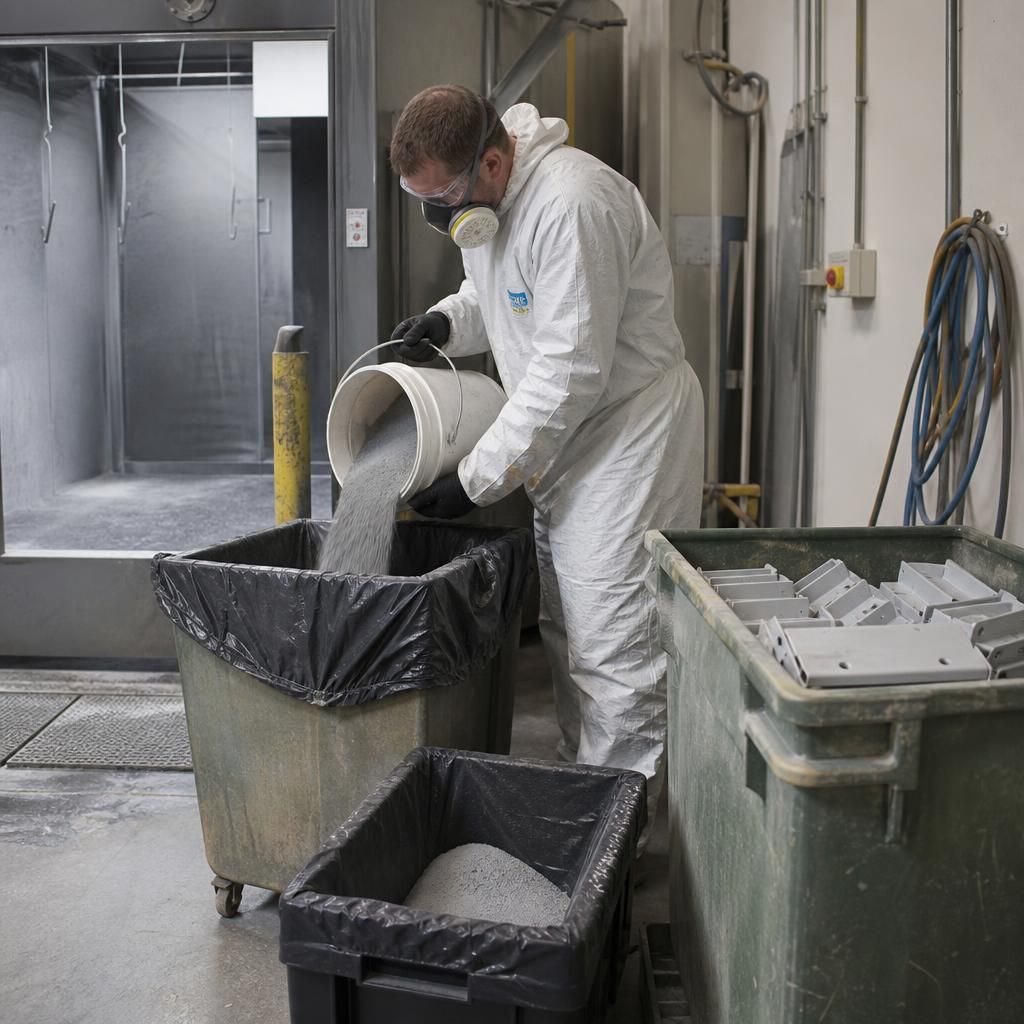
Waste controls are part of selecting a compliant zinc primer powder coating because unused powder, contaminated extraction media, spill residues and coating-removal debris must be managed according to their composition. The product safety data sheet should be used with the application process to determine whether waste is hazardous, rather than assuming that all zinc-containing powder has the same classification.
- Identify likely waste streams before production begins, including overspray, cleaning materials and defective coated parts.
- Keep different waste types separate where mixing could affect classification, recovery or disposal.
- Use suitable labelled containers and prevent powder residues from entering drains or unprotected ground.
- Provide the required waste information to the authorised waste contractor and retain the relevant transfer or consignment records.
This assessment should form part of the coating specification and site risk assessment. It helps ensure that the selected primer is practical to handle throughout storage, application, rework and disposal, not merely compliant as a product in its unopened packaging.
Discuss Your Zinc Primer Compliance Requirements
Share your component specification, service environment and intended end use with the powder-coating.co.uk team to identify the relevant zinc primer compliance requirements. This can help establish what technical evidence, system compatibility checks and documentation should be included before coating begins.