

What are the most effective methods for ensuring uniform thickness and coverage during the nylon coating process?
Uniform nylon coating depends on thorough, consistent surface preparation, controlled powder application and correct positioning of each component. Calibrated equipment, stable process conditions and measured film-thickness checks help identify uneven coverage and maintain a consistent finish across batches.
Uniform nylon coating is achieved by matching the application method to the component’s geometry, controlling the part’s thermal profile, maintaining consistent powder condition and validating coverage on representative areas. No single technique suits every component: simple shapes, deep recesses, thin sections and large fabrications each require different controls to prevent thin spots, heavy edges or missed surfaces.
Select the process according to component geometry. Fluidised-bed coating is well suited to parts that can be heated evenly and immersed without trapping powder. It can produce substantial, continuous coverage on relatively straightforward shapes. Electrostatic spray application offers more control for larger components, selective coating and shapes that cannot be immersed. Preheated-powder or hot-flock methods may also be appropriate for particular nylon systems. The selected process should reflect the required film build, access to all surfaces, component mass and the way heat will move through the metal.
Control the thermal profile of the part. Nylon powder must soften and flow sufficiently to form a continuous film, but excessive heat can cause over-thick areas, surface defects or unnecessary degradation. Thin sections and exposed edges heat differently from heavy welds and dense sections, so the heating cycle should be assessed across the actual component rather than judged from the oven or heater setting alone. Representative trial pieces, particularly those containing both light and heavy sections, help establish whether the complete part is reaching the condition needed for even flow.
Account for difficult geometry. Corners, holes, internal faces, sharp edges and recessed areas do not receive powder in the same way as broad, accessible surfaces. A suitable spray path should expose these areas without repeatedly directing powder at the nearest edge. Where practical, the design can include suitable radii and avoid abrupt transitions that encourage local build-up. Deep cavities may need a dedicated access sequence, while narrow openings may require a different nozzle position or application method to prevent a thin internal coating.
Manage powder condition and fluidisation. Nylon powder can be affected by moisture and contamination, which may alter flow, charging behaviour and melt consistency. Powder should be kept in clean, controlled storage and handled in a way that prevents foreign material entering the process. For fluidised-bed work, the air distribution must keep the powder moving evenly without creating dead zones or excessive turbulence. In spray work, consistent feed and atomisation are important so that the deposited layer does not vary as the operator moves around the component.
Use a repeatable application sequence. A defined sequence reduces the risk of relying on operator judgement from one part to the next. It should identify the surfaces to be coated, the order in which they are approached, the number and direction of passes where spraying is used, and the areas that need particular attention. Welds, brackets, returns and internal faces should be included in the sequence rather than treated as optional touch-up areas. Touching up an isolated thin spot can create a visible or functional transition if the surrounding film has already begun to set, so prevention is preferable to correction.
Design fixtures for access and electrical continuity. Racks and contact points should support the component without shielding important surfaces or becoming coated to the point that they interfere with repeatability. For electrostatic application, a clean, reliable electrical path is essential for predictable powder attraction. Contact points should be chosen on areas that can tolerate a small uncoated mark or can be treated as part of the finishing plan. Fixture design should also prevent parts moving or touching during heating and coating, as contact can interrupt coverage and create marks.
Use a representative control sample. A first-off component or test piece with comparable material thickness, welds, apertures and recesses provides more useful process evidence than a simple flat panel. It can show whether the chosen method is reaching the least accessible areas and whether the heating cycle produces the intended flow across different sections. When a batch contains significantly different component designs, grouping similar parts and reviewing each group separately is more reliable than assuming one setting will suit every shape.
Inspect more than the broad visible faces. A coverage review should include edges, undersides, internal faces, attachment points and areas close to fixtures. Visual inspection can identify missed regions, runs, roughness and local build-up, while a documented thickness map helps reveal repeatable patterns such as consistently thin recesses or heavy edges. If a defect follows the same location on successive parts, the cause is usually more effectively addressed through the application sequence, fixture, heating arrangement or component orientation than through additional powder.
Keep the process reproducible between batches. Record the coating system, part type, loading arrangement, application method and relevant thermal conditions so that a proven setup can be repeated. Powder reclaim, colour changes and cleaning arrangements should be managed to avoid contamination or altered feed characteristics. Any change in metal thickness, component design, powder condition or equipment should trigger a review using a representative sample rather than being assumed to have no effect.
For industrial components, the most dependable approach is therefore a documented process built around the part’s geometry: choose the appropriate nylon application method, establish even heat flow, maintain clean and consistent powder, provide access to difficult surfaces, and verify the complete component through a repeatable inspection plan. This combination addresses both coverage and film-build variation more effectively than increasing powder quantity or adding isolated corrective passes.
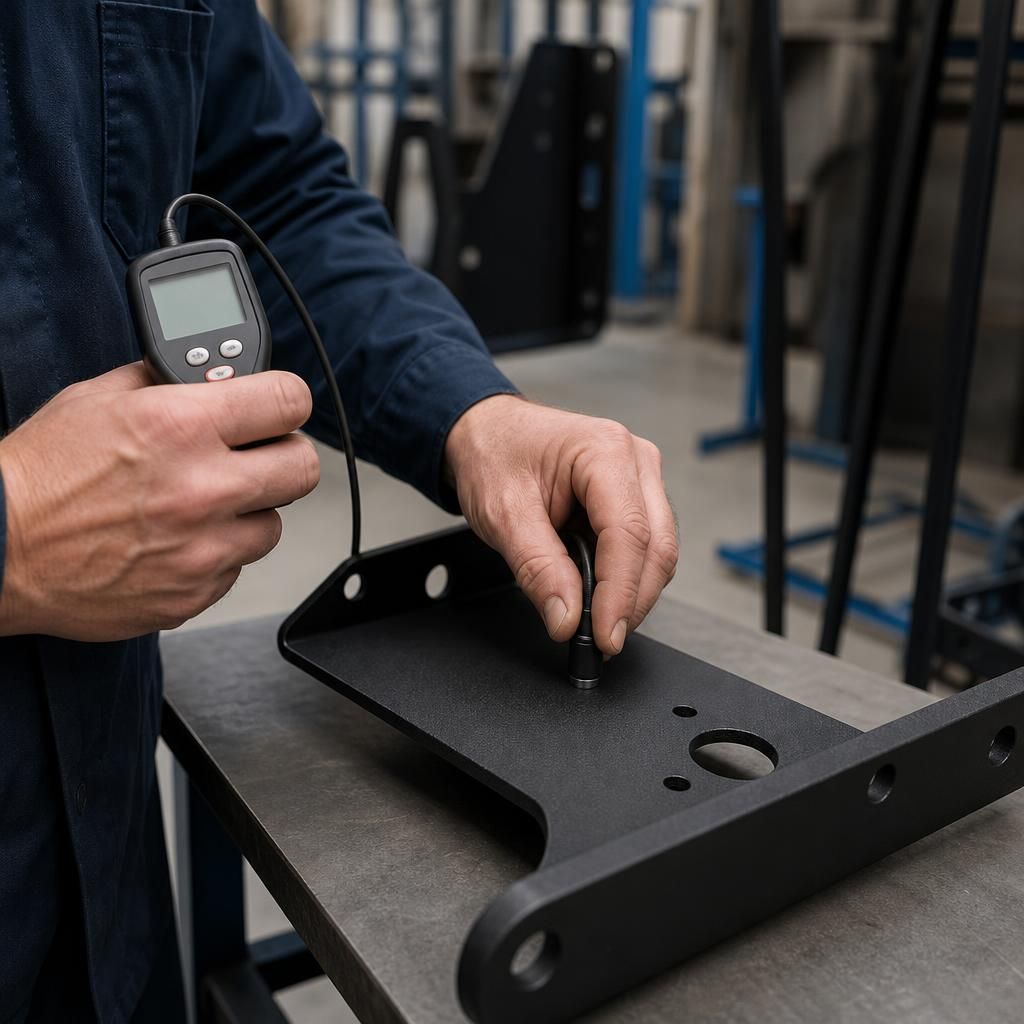
A reliable thickness check begins with agreed acceptance criteria, not simply taking an average reading. Define the required minimum and maximum film build, identify critical surfaces and record measurements at consistent locations on representative components. Use a suitable, calibrated gauge for the nylon coating and metal substrate, and take readings only when the coating has cooled and stabilised sufficiently for dependable results.
Thickness readings alone cannot confirm complete coverage. A sound inspection combines recorded measurements with a deliberate search for missed areas, pinholes, exposed edges and uncoated contact points. Where a component has surfaces with different functional requirements, assess each area against its own specification rather than applying one general reading to the whole part. This separates a genuinely uniform coating from one that merely produces an acceptable average.