

What are the typical turnaround times for industrial powder coating projects and how does this affect project scheduling?
Industrial powder coating turnaround times vary according to part size, preparation requirements, batch volume, coating specification and the production schedule. Build these stages, along with collection or delivery, into the project plan and confirm the expected programme before committing to downstream manufacturing or installation dates.
There is no single standard turnaround time for industrial powder coating: a realistic programme is established after the coater has reviewed the components, finish specification, quantities and required preparation. Straightforward repeat work may follow a simpler production sequence, while large, mixed or technically demanding batches require more planning before a completion date can be agreed.
Project scheduling is affected by the full route through the coating operation, not just the time spent applying powder. A typical sequence may include:
- reviewing drawings, component condition, coating requirements and any masking or dimensional restrictions;
- receiving and identifying the parts so that different batches, colours or specifications remain traceable;
- degreasing, blasting or otherwise preparing the metal surface;
- masking areas that must remain free from coating and arranging components for efficient handling;
- applying the specified powder and curing it under controlled conditions;
- checking the finished parts for coverage, appearance, adhesion-related defects and damage from handling; and
- packing the completed items for collection, delivery or onward use.
Preparation often has a greater effect on the programme than the coating application itself. Existing paint, corrosion, oil, weld residue, sharp edges and contamination may need attention before powder can be applied. Components with inaccessible areas, threaded holes, close tolerances or heat-sensitive attachments may also need additional assessment. Supplying clean, clearly identified parts with agreed masking instructions reduces the risk of clarification work or reprocessing.
Batch size and component configuration also influence scheduling. A uniform batch of similar parts can usually be planned differently from a mixed consignment containing several sizes, colours, coating thicknesses or preparation standards. Large components may require specialist handling, suitable loading arrangements and additional coordination. If several finishes are required, the production sequence may need to account for colour changes, cleaning and separation of batches.
The coating specification should be settled before production is scheduled. Colour, gloss level, texture, protective performance, film thickness, edge coverage and any requirement for nylon or another specialist coating can alter the preparation and application route. Changes made after parts have entered production can lead to rework, additional inspection or a revised completion date.
Downstream activities should be planned around the agreed completion point rather than an assumed industry-wide lead time. Installation teams, fabrication, assembly, transport and site access may all depend on the coated parts being available in the correct order. Where a project has phased requirements, it can be useful to discuss whether batches should be processed and returned in sequence, provided that this fits the production plan and avoids unnecessary handling.
Good scheduling information should include the number and dimensions of parts, their material and condition, the required finish, masking details, target dates, delivery arrangements and any inspection or documentation requirements. Drawings, photographs and sample parts can help clarify unusual components. The more complete this information is at the planning stage, the less likely it is that the programme will need to be adjusted because of an unresolved technical detail.
For businesses in the Midlands and surrounding areas, collection and delivery can be incorporated into the plan so that transport does not become a separate scheduling assumption. Parts should be packed and presented in a way that protects the finish during movement, particularly where coated surfaces, edges or large fabricated items may be vulnerable to contact damage.
The most reliable approach is therefore to treat powder coating as one linked stage within the wider manufacturing or construction programme. Confirm the specification before submitting the work, allow time for preparation and inspection, provide complete batch information, and obtain an agreed production and transport plan before fixing dependent installation or dispatch dates.
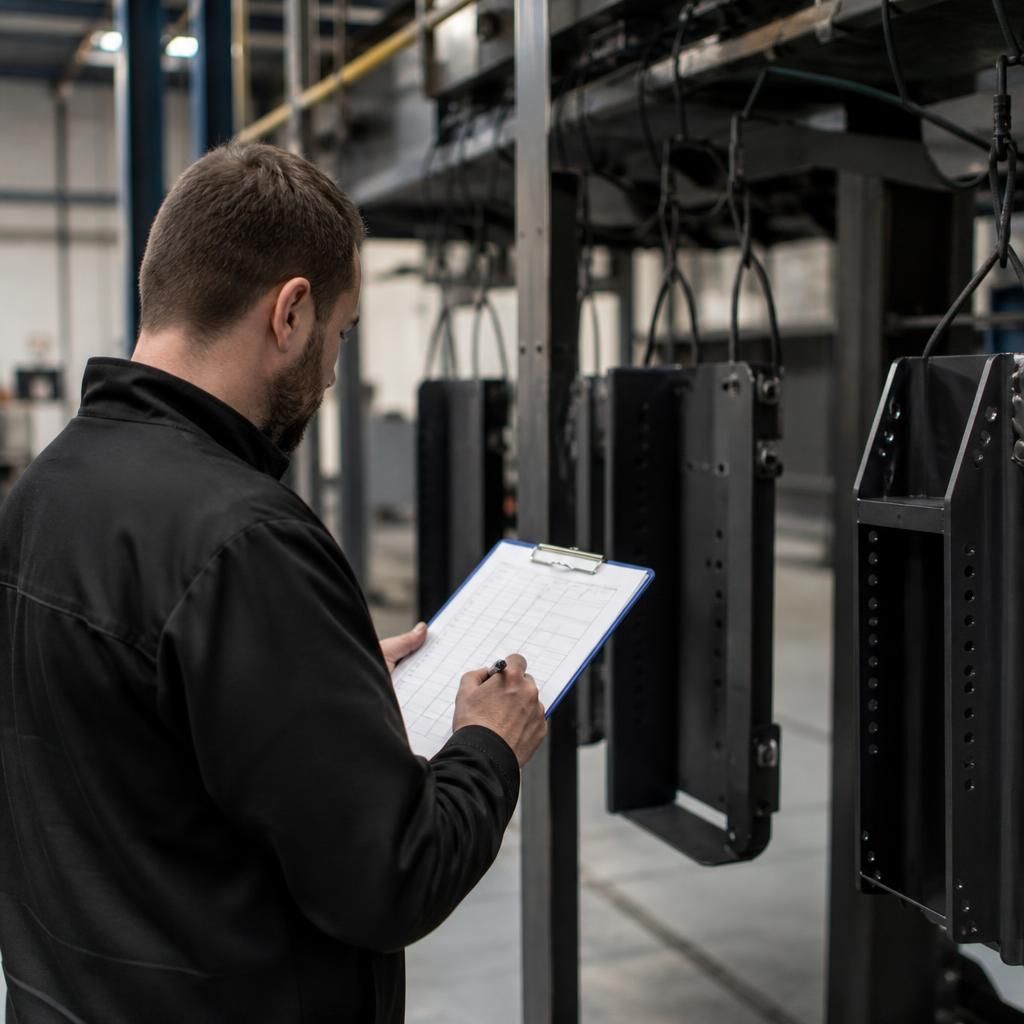
Turnaround planning is most reliable when the coating scope is treated as a controlled production release. Once the parts, finish and preparation requirements have been agreed, late changes should be assessed before being added to the batch. A colour change, revised masking instruction or additional component may require a separate setup, cleaning or inspection step rather than simply extending the existing run.
For projects with a fixed installation or assembly sequence, separate approved batches can help maintain control without allowing unconfirmed additions to disrupt the main programme. Any change should be recorded with its effect on the coating sequence, inspection point and handover arrangement, so the wider project schedule is based on a current production position rather than an earlier assumption.