

What challenges might arise from incorrect powder coating thickness on steel, and how can these be mitigated?
Incorrect powder coating thickness on steel can cause inadequate corrosion and wear protection when too thin, or cracking, poor adhesion, uneven curing and unnecessary material use when too thick. Mitigation involves defining the required film thickness, controlling application and curing, and checking the finished coating with suitable thickness measurements so deviations can be corrected.
Incorrect powder coating thickness on steel is best addressed by treating thickness as a controlled manufacturing characteristic rather than a final visual check. The specification should define the acceptable film-thickness range, the areas to be measured, the measurement method, and the action required if readings fall outside the agreed limits. This prevents disputes caused by different interpretations of what constitutes an acceptable coating.
Dimensional problems can arise when coating is applied to close-fitting components. Additional material around mating faces, slots, holes, threaded sections and locating points may affect assembly, especially where the steel part has tight tolerances. Coating build-up can also alter the fit of moving parts or prevent fasteners from seating correctly. These risks should be considered during design and communicated before production. Critical faces can be masked, plugged or kept free of coating where the design requires it, while sufficient clearance should be allowed for coated areas.
Part geometry affects thickness control. Sharp edges, corners, recesses, internal faces and welds do not accept powder in the same way as broad, flat surfaces. Electric-field effects can cause powder to accumulate at corners while recessed areas receive less coverage. Weld spatter, rough grinding, burrs and abrupt changes in section can create local high and low readings. Preparing edges, removing contaminants, blending rough welds where appropriate and using a suitable application technique reduces these variations.
Some components also contain areas that are difficult to coat consistently because of their shape or how they are suspended. The racking position, part orientation, gun angle and distance from the application equipment all influence deposition. Repositioning the component, adjusting the spray path or applying powder in more than one direction can improve access to shielded faces. Any masking must be secure and resistant to the cleaning and curing stages so that it does not move or leave unwanted residue.
Measurement can be misleading if the inspection method is unsuitable. A single reading does not represent an entire steel component, particularly when the part has edges, welds, recesses or large flat areas. Readings should be taken from agreed representative locations, with additional checks at features known to be difficult to coat. The gauge should be suitable for the coating and steel substrate, checked against appropriate reference standards, and used on clean, stable surfaces. Repeated readings help identify a pattern rather than relying on an isolated result.
Inspection results should be recorded against the component, batch or production stage. A thickness map or inspection record can show whether a deviation is confined to one feature or indicates a wider application problem. If the result is close to the specification limit, the measurement uncertainty and the condition of the surface should be considered before accepting or rejecting the part. Where required, a second inspection method or independent check can help resolve doubtful readings.
Curing must be assessed alongside thickness. Powder does not achieve its intended properties simply because it has been deposited at the right nominal thickness. The steel must reach the coating system’s specified metal temperature for the required time. Part mass, shape, loading pattern and oven airflow can cause different areas to heat at different rates. Monitoring the metal temperature at representative points, rather than relying only on the oven air display, helps identify under-cured or over-processed areas.
When thickness readings or appearance indicate a process problem, the cause should be identified before further parts are coated. Useful checks include:
- confirming that the powder has been stored and handled in accordance with its technical requirements;
- checking gun settings, powder delivery, atomising air and electrostatic conditions;
- verifying that the steel is properly grounded and correctly positioned on the rack;
- examining the pretreatment for contamination, incomplete cleaning or inadequate rinsing;
- reviewing oven loading, metal temperature and cure records; and
- comparing readings from flat, edge, recessed and welded areas.
Corrective action depends on the type and location of the deviation. A local application issue may be resolved by changing the spray angle, rack position or pass sequence. A recurring problem across a batch usually requires a process adjustment, equipment check or review of the part preparation. Simply applying another coat over an uncontrolled surface can increase build-up and create new dimensional or adhesion risks, so the proposed rework route should be agreed before it is carried out.
For components that cannot be reworked reliably, removal of the coating and preparation of the steel may be necessary before recoating. The removal process must not damage critical dimensions, edges, welds or the steel itself. After rework, the component should be inspected again for surface condition, thickness, coverage and cure rather than being accepted solely on appearance.
Prevention is strongest when the coating requirement is established at the design and quotation stage. The specification should identify the substrate condition, pretreatment expectations, coating system, target range, areas to be masked, critical dimensions, inspection locations and acceptance criteria. A representative sample or first-off component can expose access, masking and curing issues before a full batch is processed. This approach is particularly useful for fabricated steelwork with mixed sections or complex assemblies.
For manufacturers and fabricators, a clear information pack containing drawings, critical tolerances, part weights, coating requirements and any restricted areas gives the coater the information needed to plan the process. Where collection and delivery are used, components should also be protected from moisture, impact and contamination before coating; damaged or contaminated steel can create defects that are incorrectly attributed to film thickness. Careful specification, controlled application, suitable measurement and documented rework provide the most reliable way to mitigate thickness-related problems on steel.
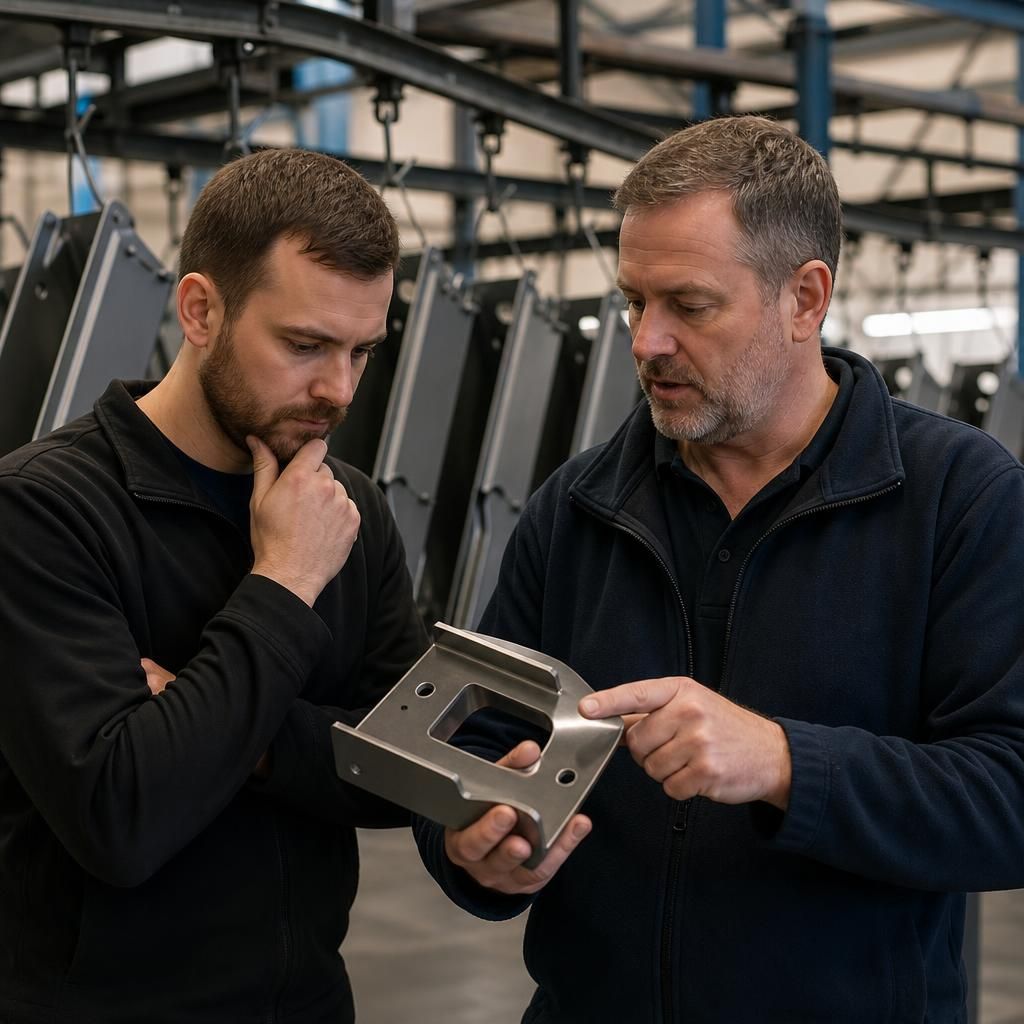
The acceptable powder coating thickness for steel should be linked to the component’s service conditions, not treated as a universal target. Outdoor steel, components exposed to corrosive substances and parts subject to repeated abrasion may require a different coating specification from sheltered items with mainly decorative or dimensional requirements. Setting the range without considering the intended environment can leave a coating under-protected or unnecessarily thick.
To mitigate this risk, confirm the exposure conditions, expected wear, appearance requirements and any dimensional constraints before production. The coating system and thickness range can then be selected to provide the required protection without creating avoidable build-up. Where a component has different functional areas, the specification should identify whether the same thickness applies throughout or whether particular surfaces need separate controls.
Discuss your steel coating thickness requirements
Discuss your steel coating thickness requirements with Powder-coatings.co.uk, including component geometry, service conditions and critical dimensions, before production begins. Providing these details helps establish a suitable coating specification and inspection approach.