

What factors should be considered when determining the thickness of an epoxy powder coating?
The required thickness of an epoxy powder coating is determined by the component’s intended use, exposure conditions, substrate, geometry and the performance required from the finished coating. The specification should also account for surface preparation, powder characteristics, curing requirements and acceptable thickness tolerances, since excessive or insufficient coverage can affect finish quality and protection.
Epoxy powder coating thickness should be set by the required performance specification and verified by measuring the cured dry film, rather than by applying the heaviest possible layer. The correct build must provide adequate coverage and protection while remaining compatible with the component’s dimensions, tolerances, appearance and curing requirements.
Required performance
The coating specification should identify what the film must withstand. A component exposed to chemicals, moisture, abrasion or repeated handling may require a different film build from an item used in a clean, dry indoor environment. Where the epoxy coating provides electrical insulation, thickness may also need to be linked to the required dielectric performance. The specification should state the required nominal thickness and the acceptable lower and upper limits, rather than relying on a general instruction such as “apply one coat”.
Substrate condition and surface profile
Surface preparation affects how the powder layer sits on the metal. Blasting can create an anchor profile that improves adhesion, but a rough surface may produce different readings at peaks and valleys. The specified thickness therefore needs to provide sufficient coverage over the profile without creating an unnecessarily heavy film. Rust, scale, oil, moisture and other contaminants can also interfere with adhesion; increasing the thickness will not correct a defective surface.
The substrate itself is relevant during application and curing. Steel, aluminium and other metals differ in thermal behaviour, conductivity and surface texture. A component with substantial mass may heat more slowly than a thin pressing, while dissimilar sections on the same part can reach curing temperature at different rates. These differences can affect flow, coverage and the final measured build, so the coating process should be assessed against the actual component rather than a flat test panel alone.
Component geometry
Edges, corners, holes, recesses, welds and enclosed sections can all produce local variations in film thickness. Electrostatic powder application may place more material on exposed faces and less inside deep recesses or narrow channels, commonly referred to as the Faraday cage effect. Sharp edges can also be more vulnerable to thin coverage, while powder may accumulate at corners or changes in profile.
Drawings should identify critical areas and any surfaces where a minimum coating build is essential. If mating faces, threaded holes, bearing seats or close-fitting assemblies are coated, the film thickness must be allowed for in the dimensional design. Masking, plugs or post-coating machining may be needed where coating is not permitted. These requirements should be agreed before production because a visually acceptable coating can still cause assembly problems if it is applied to a precision interface.
Powder and application variables
The formulation, particle distribution and intended application method influence the achievable film build. Gun settings, voltage, powder flow, spray distance, part earthing and the number of passes all affect how much powder deposits on a surface. Poor earthing can reduce transfer efficiency and create uneven coverage, while excessive deposition may lead to runs, poor flow, orange peel or other finish defects after curing.
Complex components may need a controlled application sequence rather than a uniform pass over every face. Areas that are difficult to reach may require adjustments to gun angle, spray direction or masking. A coating provider should establish settings using representative parts or trials where geometry is challenging, then monitor the result rather than assuming that the same settings suit every component.
Curing and film formation
Thickness cannot be considered separately from the curing schedule. The powder must reach its specified metal temperature for the required time so that the epoxy resin cross-links and forms a continuous film. A thick deposit may take longer to heat through than a thin one, particularly on a heavy component. If the coating is under-cured, its measured thickness may appear satisfactory but its hardness, adhesion and resistance can be compromised.
Over-application can create its own problems. An excessively thick film may trap air or contaminants, alter the surface appearance, interfere with dimensional fits and make it more difficult to achieve consistent cure through the coating. The target should therefore be a controlled, uniform build within the agreed tolerance, not the maximum thickness that can be deposited.
Measurement and acceptance criteria
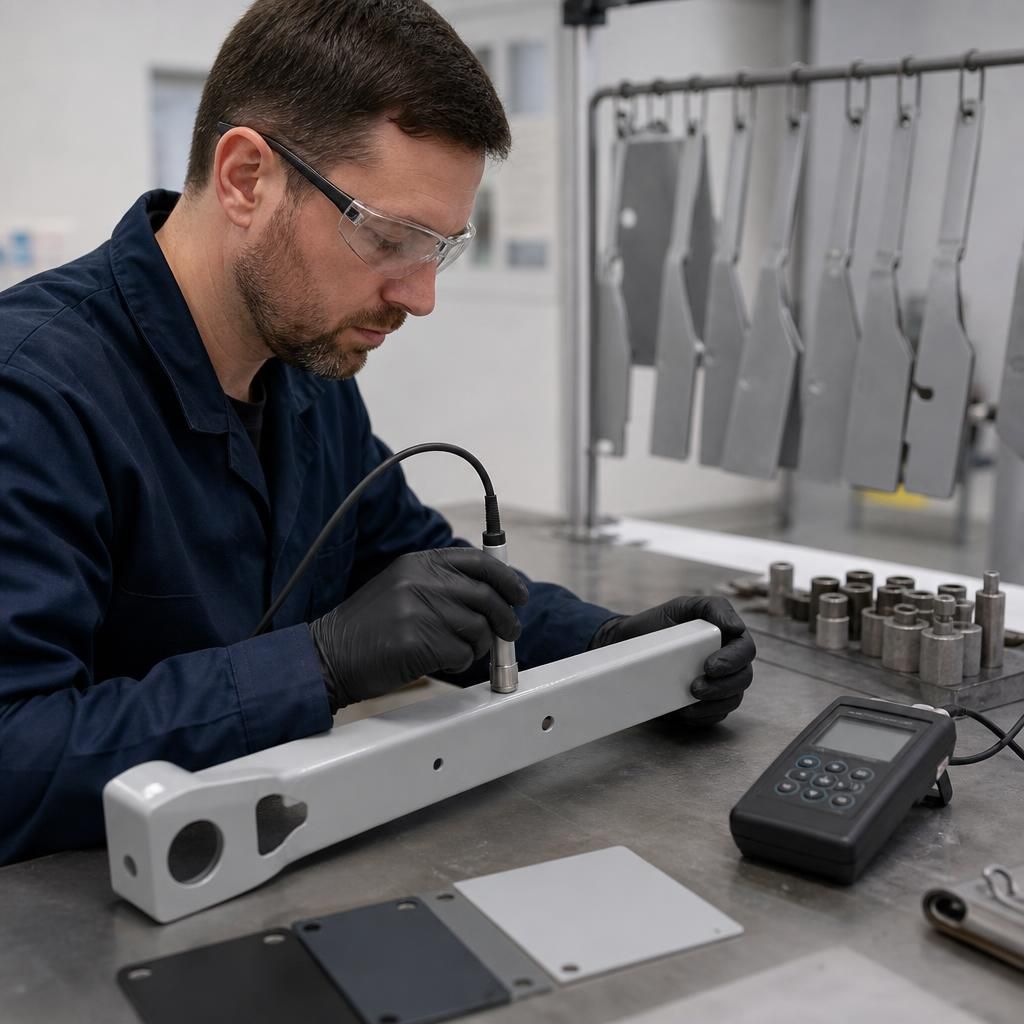
Dry-film thickness is normally checked after curing using a suitable calibrated gauge. The measurement method must match the substrate and coating system, and readings should be taken at defined locations rather than only where the finish looks most uniform. For larger or complex parts, a sampling plan can specify the number and distribution of readings, including critical edges, faces and recessed areas.
International coating inspection methods such as ISO 2808 and, where applicable, ISO 19840 provide recognised approaches to measuring and assessing film thickness. The purchase specification should make clear which method applies, how local readings are interpreted and what action is required if results fall outside the permitted range. This prevents disagreements caused by different measurement locations or by treating one isolated reading as representative of the entire component.
Practical specification information
A useful coating drawing or purchase order should include the substrate, preparation standard, powder type, target dry-film thickness, permitted tolerance, areas to be coated, areas to be masked and the required finish. It should also identify performance tests or inspection records where these are necessary. Providing component drawings, assembly clearances and details of the service environment allows the thickness requirement to be judged in relation to the finished part rather than selected in isolation.
For a new component, representative trial pieces can help confirm coverage, appearance, cure and dimensional impact before batch production. The final specification should be based on the measured result from the actual geometry and on the coating’s required function. This approach gives a more reliable thickness than using a generic value for every epoxy-coated metal component.
The epoxy powder manufacturer’s technical data sheet should be used to confirm the coating’s recommended film-build range before a thickness is specified. Different epoxy formulations can have different flow, cure and performance characteristics, so a thickness suitable for one product should not automatically be applied to another.
Where the coating must meet a particular resistance or insulation requirement, the selected build should be validated using the relevant test method on a representative coated sample. This confirms that the proposed thickness provides the required performance without introducing defects associated with excessive application.