

How can I ensure that my chosen powder coating preparation service meets industry standards for quality and safety?
Choose a powder coating preparation service that can demonstrate documented procedures for substrate cleaning, pre-treatment, inspection and batch traceability, alongside suitable risk assessments and controls for chemicals, equipment and waste. Ask for clear evidence of process checks and quality records so you can verify that preparation is consistent, safe and appropriate for your metal components.
A powder coating preparation service meets industry standards when it can show that each metal component is assessed against defined acceptance criteria, prepared using a controlled process, inspected before coating and handled under appropriate health and safety controls. The evidence should relate to your substrate, component geometry, existing finish and end use rather than relying on general claims of quality.
Check how the service defines preparation quality. A competent provider should be able to explain what a suitable surface looks like before powder is applied. This may include requirements for cleanliness, freedom from oil and grease, removal of corrosion or loose material, suitable surface profile and the absence of residues that could affect adhesion. Ask how these requirements change for steel, aluminium, galvanised metal or previously coated parts. Parts with weld spatter, sharp edges, pits, casting defects or trapped contamination may need additional attention because preparation alone cannot correct every underlying defect.
Ask for substrate-specific process information. Pre-treatment must be compatible with the metal and the powder system. For example, an aluminium component may require a different cleaning and conversion approach from a mild-steel component, while galvanised surfaces can require controls to manage their existing protective layer and outgassing risk. The provider should be able to explain why a particular cleaning, abrasive, chemical or rinsing method has been selected, including any limitations for thin sections, threaded features, close-fitting parts or components with internal cavities.
Look for measurable inspection rather than visual judgement alone. Visual inspection is useful for identifying rust, oil, mill scale, residues and obvious damage, but it should form part of a wider checking process. Depending on the agreed specification, relevant checks may include:
- surface cleanliness and the removal of visible contamination;
- the condition and profile of an abrasive-prepared surface;
- residual chemical contamination or inadequate rinsing;
- the presence of moisture before coating;
- masking and protection of areas that must remain uncoated; and
- the condition of edges, welds, recesses, holes and joints where coating defects are more likely.
Ask what happens when a part fails an inspection. A controlled service should have a defined method for recording the issue, deciding whether rework is possible and obtaining approval where the component differs from the supplied specification. This prevents unsuitable parts from moving into coating without a clear decision.
Verify the checks used to confirm the finished result. Preparation quality ultimately affects coating performance, so it is reasonable to ask how the completed coating is assessed where the project requires it. Depending on the agreed specification, this can include dry film thickness measurement, adhesion testing, visual assessment, cure verification and checks for runs, pinholes, inclusions, bare areas or uneven coverage. Testing should be appropriate to the coating system and component rather than applied automatically in the same way to every job.
For safety-critical, exposed or technically specified components, provide the service with the relevant drawing, coating specification, operating conditions and performance requirements before work begins. These details help establish suitable preparation and inspection criteria. They also clarify whether the coating must withstand abrasion, chemicals, weathering, heat, impact or repeated cleaning. A provider should identify any requirement that cannot be verified through preparation or coating checks alone.
Examine safety controls for preparation activities. Preparation can involve chemicals, abrasive equipment, compressed air, extraction systems, lifting equipment and contaminated waste. Ask how the service controls exposure to chemical products, dust, noise, flying particles and manual-handling risks. Suitable arrangements normally include documented risk assessments, safety data sheets for relevant substances, controlled chemical storage, appropriate personal protective equipment, guarding and maintenance for machinery, ventilation or extraction where needed, and safe arrangements for collecting and disposing of waste.
In the UK, the provider should operate in line with applicable workplace health and safety duties, including suitable controls for hazardous substances and work equipment. You do not need to assume that a certificate proves every control is effective: ask how employees are trained, how equipment is maintained and how incidents, spills or process deviations are dealt with. Safe working should cover the whole preparation route, including unloading, handling, masking, cleaning, drying and movement between stages.
Assess competence and consistency. Ask who is responsible for approving the preparation standard, how operators are trained and how process changes are authorised. Consistency matters particularly for repeat batches, where variation in cleaning, pre-treatment or drying can produce different coating performance. Useful evidence may include sample inspection records, agreed job specifications, non-conformance records and a clear method for confirming any changes to the component or required finish.
It is also important to agree responsibilities before work starts. Confirm what condition the parts must be supplied in, whether existing coatings or contamination will affect preparation, which areas must be masked, what tolerances apply and how defects or rework will be managed. For components with tight dimensions or assembled features, establish whether preparation and coating thickness may affect fit, threads, contact points or electrical continuity.
A practical selection check is therefore to request four things: the proposed preparation route for your particular metal, the inspection and acceptance criteria, the safety controls relevant to the work and representative quality records or test evidence. Compare the detail and relevance of the answers rather than choosing a service solely on price. For Midlands manufacturers, fabricators, construction firms and automotive businesses, a specialist powder coating provider can then assess whether its preparation approach is suitable for the component and arrange collection or delivery where required.
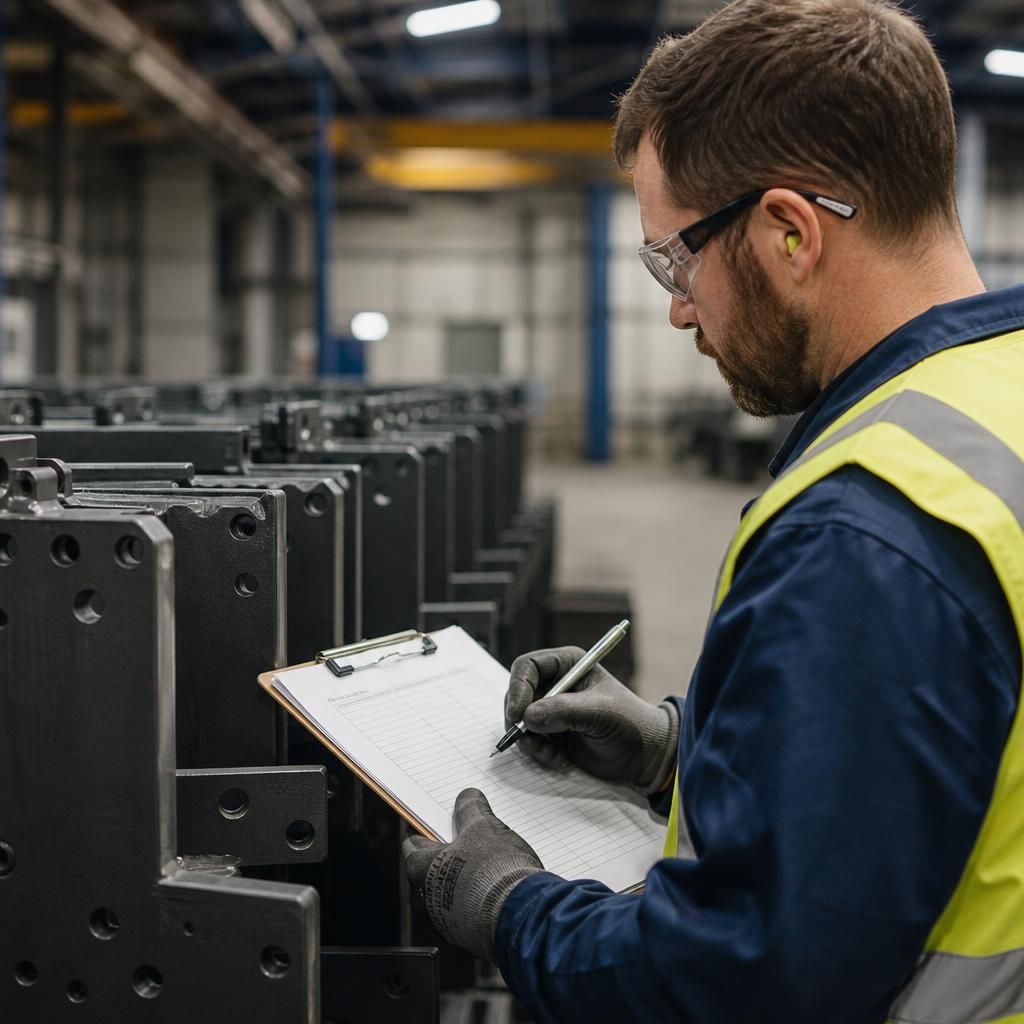
Batch traceability is a practical indicator of controlled powder coating preparation. Each component or batch should remain identifiable as it moves through cleaning, pre-treatment, drying, inspection and coating, reducing the risk of parts being mixed up or processed against the wrong specification.
Ask how the service records the job reference, substrate, agreed preparation route, inspection status and any rework. Parts awaiting inspection should be distinguishable from those approved for the next stage, while rejected or held items should be segregated. This identification system is particularly important for repeat production runs, mixed metal types and components with different masking or finish requirements.