

What are the recommended steps to ensure the correct powder coating thickness for steel, and how can they impact the performance of the coated component?
To achieve the correct powder coating thickness on steel, define the required specification, prepare the surface properly, apply the powder under controlled conditions, measure the cured film thickness, and verify the finish and cure before release. Consistent thickness supports adhesion, corrosion and wear resistance, while excessive, insufficient or uneven coating can impair protection, appearance, curing and the component’s dimensional fit.
Correct powder coating thickness on steel is a controlled film-build requirement, not simply the application of as much powder as possible. The suitable thickness must provide the specified level of protection while remaining compatible with the component’s dimensions, geometry, service conditions and finishing specification. A reliable approach combines design review, coating-system selection, controlled production checks and documented acceptance criteria.
1. Establish the required film-build range
Begin with the technical specification for the component and identify whether it gives a target thickness, an acceptable range or a performance class. The requirement may depend on the steel’s exposure to moisture, chemicals, abrasion, impact, heat or outdoor conditions. It may also be influenced by whether the part is decorative, structural, concealed or subject to frequent handling.
Thickness should be treated as a tolerance rather than a single ideal reading. The specification should state how readings are to be taken, which areas are critical and how local variations will be judged. This is particularly important where the coated part must fit against another component, pass through an opening or retain accurate clearance around holes, threads, hinges and mating faces.
2. Review the component before production
Examine the steel component’s shape, dimensions and intended use before deciding how the process will be controlled. Broad flat faces are generally easier to coat evenly than deep recesses, internal corners, narrow returns and closely spaced features. Edges can behave differently from adjacent surfaces, while recessed areas may receive less powder or be difficult to measure accurately.
Identify surfaces that must remain free from coating, such as contact points, earthing locations, threads, bearing seats and precision-fit areas. Masking, racking and hanging arrangements should be agreed before coating begins, since these affect access to the steel and can leave contact marks or uncoated points. Parts with complex geometry may require a measurement plan that gives greater attention to vulnerable or functionally important areas.
3. Confirm the powder and substrate are suitable
The powder manufacturer’s technical information should be checked for the recommended application range, curing conditions and compatibility with the intended steel substrate and service environment. The chosen system should be suitable for the required level of corrosion protection and any additional chemical, mechanical or thermal demands.
Consider the steel grade, surface condition and any previous treatment. Welds, sharp edges, weld spatter, porosity, oil, scale and embedded contamination can affect the local film even when the average thickness appears acceptable. Where a conversion coating, primer or specialist protective layer is part of the system, the thickness of each layer and the combined build should be included in the specification.
4. Plan the application around the part geometry
Application settings should be selected to produce a stable and even deposit rather than to correct defects after coating. Gun position, movement, powder delivery, electrostatic settings, earthing and the arrangement of the part should be reviewed for the component being processed. Recesses and Faraday areas may need a different application approach from exposed faces.
Parts should be presented consistently from one batch to the next. Consistent racking and orientation make it easier to compare results and identify whether a recurring thin or heavy area is caused by the component, the application method or the equipment. Where several parts are coated together, the inspection plan should include locations from different positions on the rack or conveyor.
5. Control curing as well as film build
Powder coating thickness cannot be judged reliably until the film has been cured under the specified conditions. The relevant condition is the temperature reached by the steel, not simply the temperature displayed by the oven. Part size, mass, loading pattern and the position of the component in the oven can all affect heat penetration.
Use suitable temperature-monitoring methods to confirm that representative parts reach the required cure profile. If the film is outside the intended thickness range, curing behaviour may also change. A heavy deposit can require more heat input to cure fully, while a thin or uneven deposit may leave weakly protected areas even when the surface appears acceptable.
6. Measure using a defined inspection method
Use an appropriate calibrated dry-film thickness gauge for the steel substrate and check the instrument in accordance with the relevant inspection procedure. Calibration or verification should account for the type and condition of the substrate, the probe being used and the expected coating range.
Measurements should be taken at planned points rather than only on the most accessible face. Include representative flat areas, edges where measurement is practical, corners, recesses and surfaces with a functional requirement. Avoid treating one reading as proof of uniformity. A series of readings gives a more useful picture of the coating distribution and helps distinguish an isolated reading from a process-wide issue.
Where a reading is unexpectedly high or low, check the surface again and confirm that the probe is correctly positioned. Rough steel, curved surfaces, narrow sections and awkward access can influence measurement reliability. The inspection record should identify the part, locations checked, readings obtained, equipment used and the acceptance decision.
7. Assess the result against function, not appearance alone
A smooth, attractive finish does not prove that the coating has the required thickness or cure. Review the measured film build alongside visual inspection, adhesion requirements, edge coverage, masking quality and the dimensional needs of the component. Pay particular attention to areas where coating could interfere with assembly or where inadequate coverage could expose the steel during service.
If the specification calls for additional tests, carry them out using the agreed method and on representative parts. Tests might assess adhesion, cure or resistance to the conditions expected in service, but the selected tests should reflect the coating system and the component’s actual risk rather than being used as substitutes for basic thickness control.
8. Correct variation and retain process records
When readings fall outside the agreed range, quarantine or identify the affected parts and determine the cause before releasing them. Possible causes include inconsistent earthing, unsuitable gun settings, poor racking, excessive powder delivery, inadequate access to recesses, contamination or an incorrect cure profile. Rework should only be undertaken where the coating system and component specification allow it; adding another layer can create excessive build or obscure the source of the problem.
Records of thickness readings, cure checks, equipment verification, batch details and corrective actions provide evidence that the process was controlled. They also make it possible to compare recurring problem areas and refine the application method for future batches.
The performance benefit of this approach is balanced protection. A coating that is too thin may leave vulnerable steel areas, while excessive build can affect curing, appearance, assembly clearances and resistance to impact or cracking. Even distribution within the agreed specification therefore supports more predictable corrosion protection, wear behaviour, dimensional fit and service performance than a high average thickness achieved with substantial local variation.
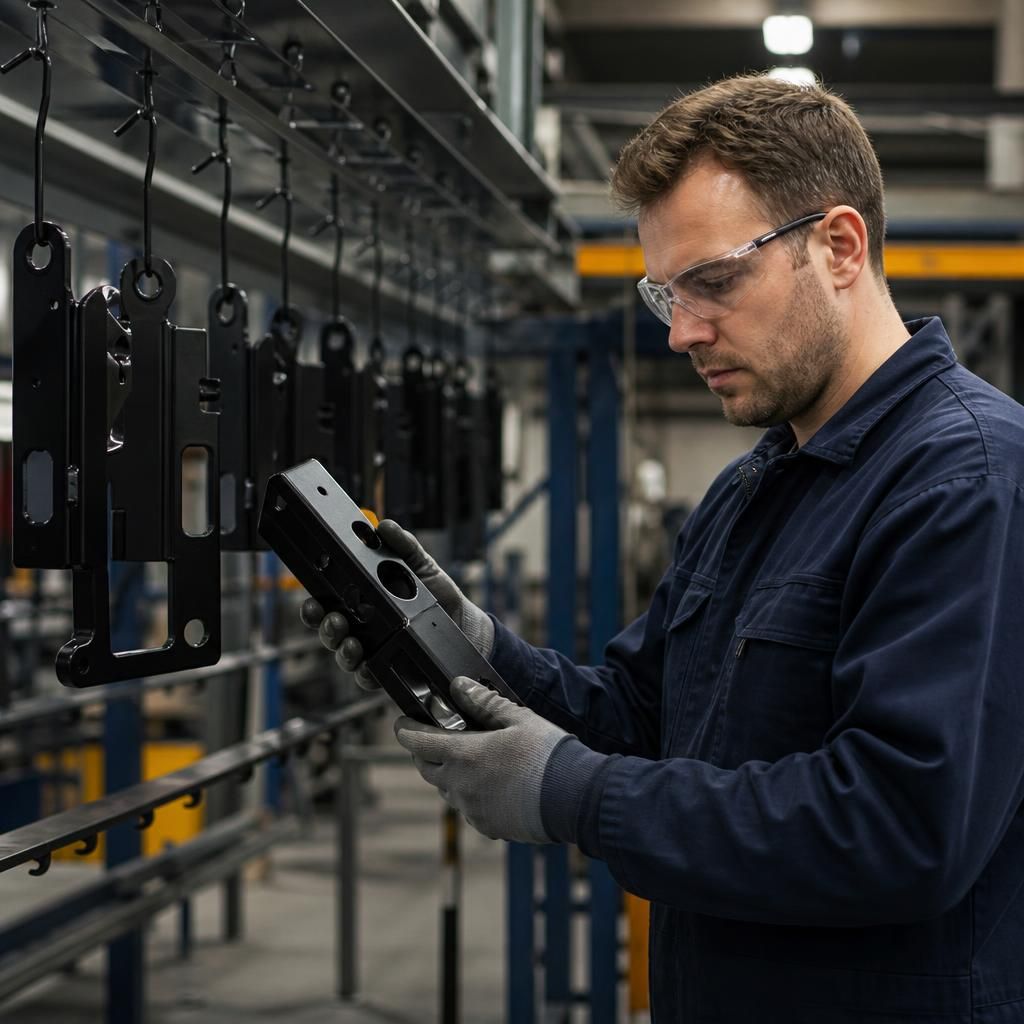
For complex steel components, a first-off or representative sample should be used to validate the coating process before the full batch is released for production. This allows the applicator to confirm that the selected powder, racking arrangement and application settings work with the component’s geometry, rather than relying on results from a simpler test piece.
Any adjustments identified during this validation can then be applied consistently across the batch. This reduces the risk of discovering widespread non-conformance after coating, when correction may affect dimensions, appearance or the suitability of the finished component for assembly and service.
Discuss your steel coating thickness requirements
Discuss your steel component’s geometry, service environment and coating specification with the powder-coating team to establish a suitable thickness-control plan. Providing drawings, target film-build requirements and any critical dimensional areas will help define the appropriate inspection approach.