

What are the critical application techniques for maximising the effectiveness of zinc epoxy primer?
Maximising zinc epoxy primer effectiveness depends on thorough surface preparation, accurate mixing, controlled film application and complete curing under the coating manufacturer’s specified conditions. Removing contamination and corrosion, maintaining suitable environmental conditions, and achieving an even, continuous film are essential for reliable adhesion and corrosion protection.
The most effective zinc epoxy primer applications use the application method, equipment and inspection process appropriate to the component’s geometry and service conditions. In practice, this means selecting suitable spray equipment for production work, using controlled brush application for localised areas, treating edges and welds deliberately, maintaining the zinc pigment in suspension and verifying the finished coating before subsequent coats are applied.
Select the application method to suit the component
- Airless spray: Often the preferred method for larger fabricated parts and production work because it can deposit a consistent, adequately built film without excessive solvent dilution. Equipment settings should be matched to the primer’s technical data sheet rather than selected solely for convenience.
- Conventional spray: May be suitable where finer atomisation or detailed control is required, although it can introduce more overspray and may require greater operator control.
- Brush or roller: Useful for small components, edges, difficult-to-reach areas and local repairs. These methods should be used carefully because excessive working can disturb the zinc-rich film and create an uneven surface.
Application equipment must be clean and compatible with the primer. Residues from previous coatings, unsuitable hoses or contaminated spray components can affect adhesion, appearance and the protective performance of the primer.
Control zinc pigment settlement during application
Zinc particles are dense and can settle in the container or application equipment. The material therefore needs to remain properly agitated throughout use, following the coating manufacturer’s instructions. If the zinc-rich solids are not kept evenly distributed, one section may receive too much binder and another too little zinc, reducing consistency across the component.
Operators should also avoid adding thinner simply to make application easier. Any thinning must be expressly permitted by the product data sheet and carried out within its stated limits. Excessive thinning can reduce build, alter the drying behaviour and leave insufficient zinc-rich material in the protective film.
Give special attention to edges, welds and complex profiles
Sharp edges, corners, weld toes, bolt heads, cut-outs and recessed sections are more difficult to coat uniformly than broad flat faces. They can suffer from reduced coverage, runs, sags or premature breakdown if they are not handled deliberately. A controlled stripe coat or carefully directed pass may be appropriate on vulnerable details, provided it is compatible with the specified coating system.
Spraying should follow a logical sequence that keeps awkward areas visible and accessible rather than allowing them to become hidden behind later work. Components should be positioned so that recesses, undersides and internal faces can be reached without excessive spray shadow. Where a design creates narrow gaps or enclosed sections, the coating specification should confirm whether the primer is suitable and how those areas are to be treated.
Use disciplined spray technique
The spray gun should be held at a consistent distance and kept square to the surface wherever access allows. Arcing the gun, moving too quickly or lingering at the end of a pass can produce dry spray, thin zones, runs or localised over-application. A planned sequence with controlled overlap helps maintain uniformity without relying on repeated corrective passes.
Spray pressure, tip selection and material delivery should be adjusted to produce proper atomisation while avoiding unnecessary misting. Dry spray can create a rough, weakly bonded surface, while excessive wetness can trap solvent or cause sagging. The correct balance depends on the product, equipment, component temperature and surrounding conditions, so the manufacturer’s application instructions should take precedence.
Respect recoat compatibility and sequence
Zinc epoxy primer is usually one part of a wider coating system rather than the final protective layer. The next coat must be compatible with the primer and applied within the specified recoat conditions. Applying a subsequent coat too soon can interfere with the primer’s development, while waiting beyond the permitted interval may require additional treatment before recoating.
The planned system should also account for the intended topcoat, exposure conditions and appearance requirements. A primer selected for one overcoat combination should not automatically be assumed suitable beneath another. Technical documentation should be checked for intercoat adhesion, maximum and minimum recoat intervals, abrasion requirements and any restrictions on overcoating.
Inspect the coating rather than relying on appearance
Visual inspection is useful for identifying runs, pinholes, missed areas, dry spray, embedded debris and obvious texture defects, but it cannot confirm film thickness on its own. Suitable thickness measurement should be carried out using a calibrated gauge and a documented inspection plan. Readings should cover representative flat areas as well as edges, welds, corners and other locations where coating build is likely to vary.
For components requiring a high level of corrosion protection, inspection may also include checks for discontinuities or pinholes, particularly where the primer forms part of a specified protective system. Defects should be repaired using an approved method, and repaired areas should be rechecked before the component proceeds to the next coating stage.
Record the process for repeatable results
For batch work, consistency improves when the coating process is recorded. Useful information includes the primer specification, batch identification, application method, equipment settings, environmental readings, inspection results and any repairs undertaken. This record helps identify variation between batches and provides evidence that the specified coating system was followed.
These techniques are particularly important for fabricated metal components with mixed geometries or demanding service conditions. A specialist powder-coating or industrial finishing provider can review the component design, coating specification and production requirements before confirming whether zinc epoxy primer is suitable as part of the wider protection system.
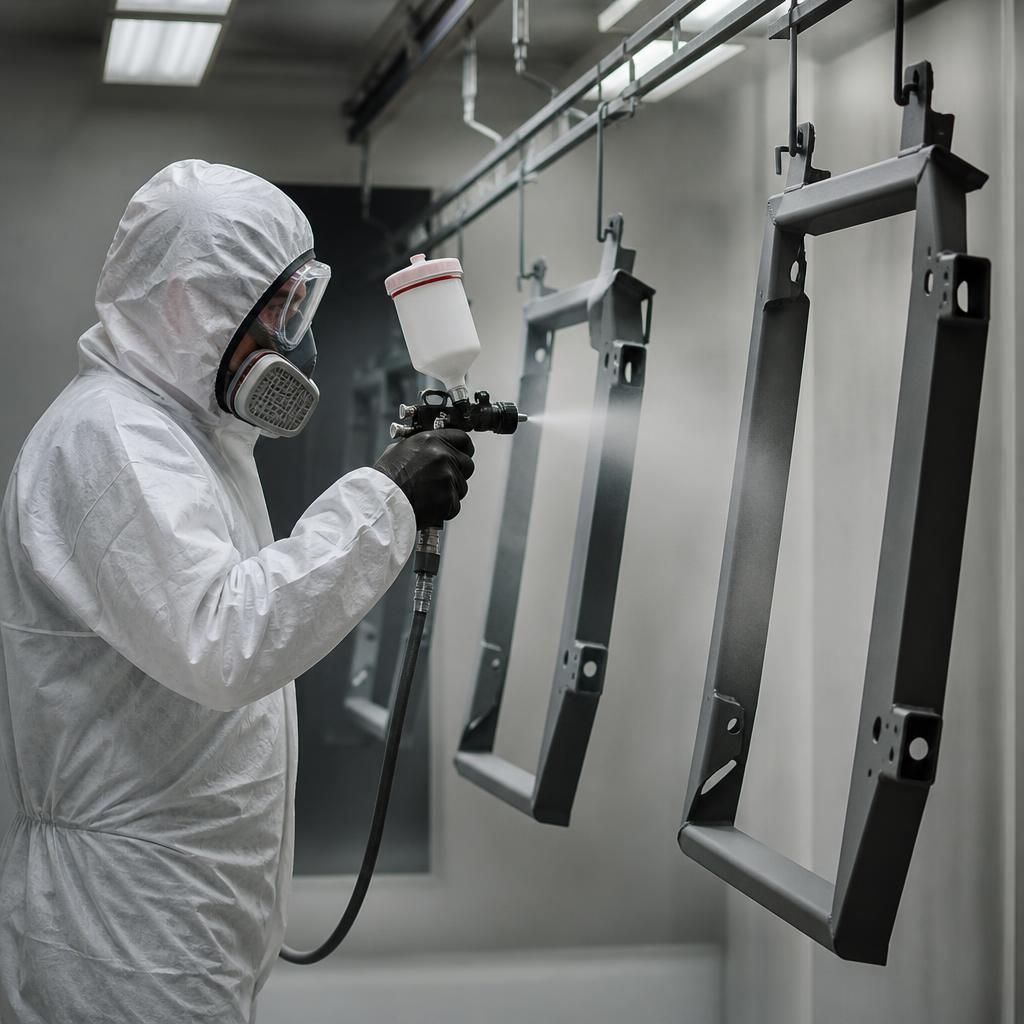
Environmental control is a critical zinc epoxy primer application technique because condensation, excessive humidity and unsuitable temperatures can compromise adhesion and curing. Before coating, confirm that the metal is clean, dry and sufficiently above the dew point to prevent invisible moisture forming on the surface during application.
Record the substrate and surrounding air conditions, and avoid applying primer when temperature or humidity falls outside the product manufacturer’s specified range. Maintain suitable ventilation so solvents can evaporate without causing excessive airflow across the wet film. The coated component should remain protected from moisture, contamination and temperature changes throughout the stated curing period.
Discuss your zinc epoxy primer application requirements
Discuss your component geometry, service conditions and proposed coating system with a specialist before specifying zinc epoxy primer. This helps establish whether the application method and inspection requirements are suitable for your metal parts.