

What factors determine the optimal powder coating thickness for steel components?
The optimal powder coating thickness for steel components is determined by the required corrosion and wear resistance, the component’s service environment, its geometry and the coating specification. The powder type, application method and curing requirements must also be considered, as excessive thickness can affect finish quality while insufficient coverage may reduce protection.
The optimal powder coating thickness is the cured film-build range that provides the required protection and appearance without creating defects, dimensional problems or curing difficulties. It is established by considering the component’s specification, the condition and design of the steel, the coating system being applied and the way thickness will be checked before the parts are released.
The required performance level comes first. A specification may prioritise resistance to moisture, chemicals, abrasion, impact, heat or handling damage. These requirements can lead to different film-build targets and, in some cases, a multi-layer system rather than one unusually thick coat. The coating manufacturer’s technical data should be used alongside the end user’s requirements, because a product’s recommended application range is part of its performance design.
The steel substrate affects the practical result. Surface roughness, mill scale, weld spatter, sharp imperfections and remnants of previous coatings can all influence the measured and effective film build. Powder follows the prepared surface rather than creating a perfectly flat layer. A rough profile can therefore require sufficient coating to cover the peaks while retaining protection in the valleys. Preparation should remove contaminants and unstable material before thickness targets are considered; increasing the powder load is not a substitute for sound preparation.
Part design creates areas that need particular attention. External faces, internal corners, holes, returns, recesses and boxed sections may not receive powder evenly. Edges can become thinner or heavier depending on the electrostatic field and the way the powder is deposited. Tight tolerances around mating faces, threads, slots and moving interfaces may also limit the permissible build. These areas should be identified at quotation and production-planning stages so that masking, racking, gun positioning or a different application sequence can be selected where necessary.
Dimensional requirements can be decisive. The coating adds material to the steel, which may affect assemblies, press fits, sliding surfaces, fastener engagement and the alignment of adjoining parts. The required build should therefore be assessed against drawings and tolerances, not just the visible finish. Critical surfaces may need masking or a controlled coating boundary, while non-critical faces may allow a wider working range.
Appearance also places limits on thickness. Excess powder can produce runs, sags, orange peel, cratering, pinholes or an uneven texture. Heavy build may be particularly noticeable on broad flat panels and on edges where powder accumulates. Conversely, low build can leave the substrate texture visible, reduce opacity or create inconsistent gloss and colour. A visually acceptable result depends on the powder’s finish characteristics, the steel’s preparation and consistent deposition, rather than thickness alone.
Application conditions influence how the target is reached. Gun settings, part temperature, earthing, distance from the component, movement speed and the number of passes all affect deposition. Complex assemblies may need more than one angle of application to reach recessed areas, whereas excessive passes on accessible faces can create overbuild. Racking should expose the required surfaces without creating contact points that remain uncoated.
Measurement must represent the whole component. One reading from an accessible flat face cannot confirm uniformity. Checks should cover representative high-build and low-build locations, including edges, corners and areas with different orientations. A calibrated dry-film thickness gauge is normally used after curing, with readings assessed against the agreed specification and any permitted range. Where a part is safety-critical, dimensionally sensitive or subject to formal inspection, the inspection plan should define measurement locations, frequency and acceptance criteria before production begins.
Coating build should be reviewed alongside cure and handling. The measured thickness is meaningful only when the film has been properly cured and the component has been handled without damaging the surface. A thick deposit can require careful control of the curing cycle, while an under-cured film may not deliver the properties expected from its nominal build. The coating system’s technical instructions should therefore govern both the target thickness and the conditions used to confirm the finished result.
For a production component, the most reliable approach is to agree the target range from the performance and dimensional requirements, inspect the steel and its preparation, identify difficult features, apply a controlled test piece or first-off component where appropriate, and record thickness readings from representative locations. This turns thickness from a visual estimate into a defined process requirement that can be repeated across batches.
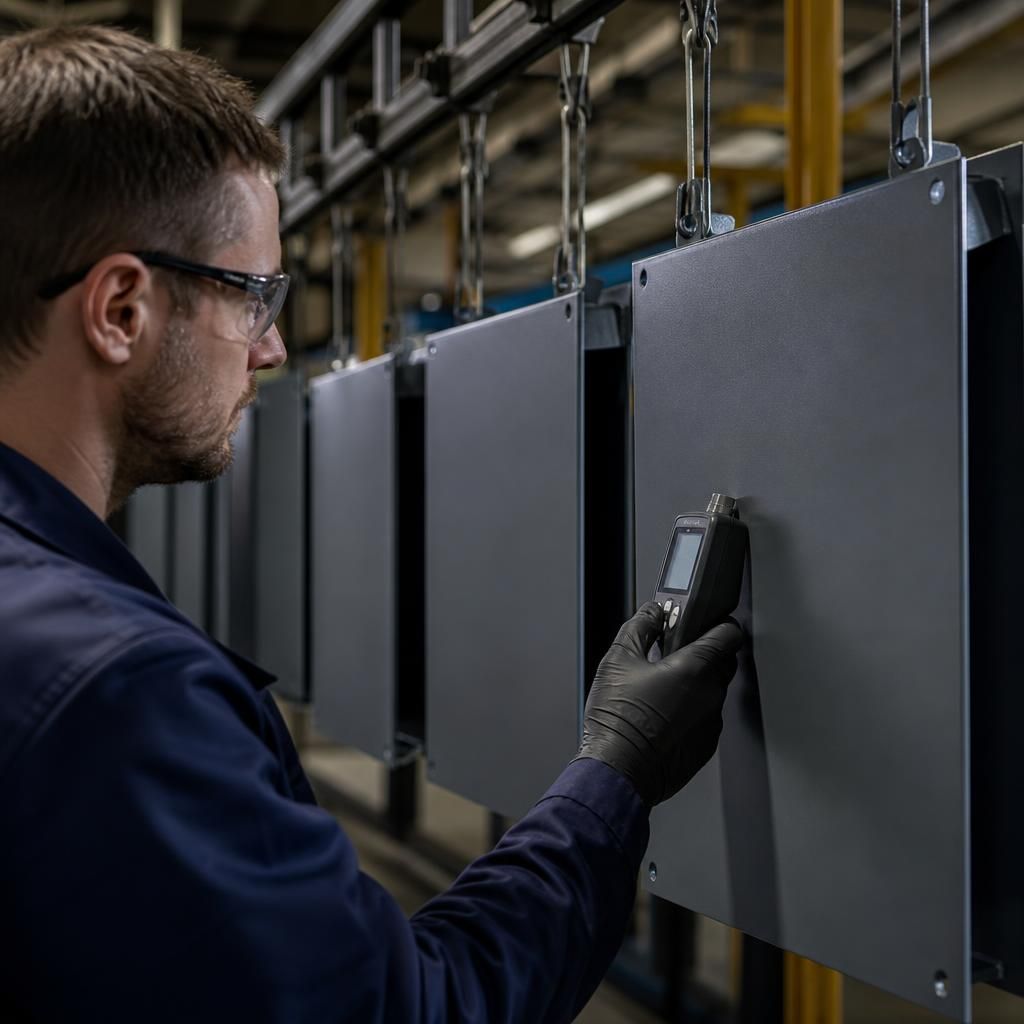
Optimal powder coating thickness must be assessed on the cured film, not solely on the amount of powder applied. Component mass, section thickness and geometry affect how quickly the steel reaches the required metal temperature, so two areas receiving a similar powder deposit may not develop identical final performance if their cure conditions differ.
This is particularly important for assemblies combining thin sheet, heavy plate, brackets or boxed sections. The production process should account for the slowest-heating areas and confirm that the specified cure schedule is achieved without compromising thinner sections or sensitive components. Thickness readings should therefore be interpreted alongside cure records and the coating manufacturer’s technical requirements, rather than treated as evidence of performance in isolation.