

What role do alkaline and acidic pretreatment chemicals play in preparing surfaces for powder coating?
Alkaline pretreatment chemicals typically degrease metal by removing oils, grease and workshop residues, while acidic chemicals remove oxides, scale and other inorganic contamination and may lightly etch the surface. Used in a controlled sequence suited to the substrate, they create a cleaner, more chemically receptive surface for powder coating, supporting adhesion and corrosion protection.
Alkaline and acidic pretreatment chemicals control the condition and chemistry of a metal surface before powder is applied. Their role is not simply to make components look clean: they help establish a consistent surface that allows subsequent coating stages to perform as intended, while reducing the risk of defects caused by contamination, oxidation or incompatible residues.
Alkaline chemicals provide the initial conditioning stage. They are commonly formulated with builders, wetting agents and detergents so that contamination can be loosened and carried away from the component. This is particularly important where parts have been handled during fabrication or have been exposed to cutting fluids, forming lubricants, polishing compounds, drawing oils or general workshop dirt. If these materials remain in place, they can interfere with later chemical stages and contribute to poor wetting, cratering, pinholing or localised coating failure.
The strength and formulation of an alkaline cleaner must match the substrate and the contamination being treated. Excessive alkalinity, prolonged contact or unsuitable operating conditions can attack sensitive metals or alter the appearance of the surface. Aluminium, galvanised steel and mixed-metal assemblies often need more carefully controlled chemistry than untreated carbon steel. Temperature, concentration and contact time therefore need to be controlled rather than assuming that a stronger or longer treatment will produce a better result.
Acidic chemicals perform a different conditioning function. Once organic contamination has been dealt with, an acid stage can address inorganic residues and surface films that are not effectively treated by alkaline products. It may also produce a controlled degree of micro-roughening or activation, giving the surface a more suitable chemical state for the next stage. The purpose is controlled preparation, not aggressive metal removal.
Acid selection depends on the metal. A treatment suitable for mild steel may be inappropriate for aluminium, zinc-coated material or an assembly containing more than one metal. Compatibility affects both the appearance of the component and the quality of the resulting surface. Acidic formulations may also include inhibitors or additives designed to limit unnecessary attack on the base metal, but these do not remove the need for correct process control.
The sequence between the two stages is critical. A typical process may involve an initial inspection, alkaline cleaning, one or more rinses, an acidic activation or conditioning stage, further rinsing, and then a conversion treatment where specified by the coating system. Each rinse separates one chemical stage from the next. Without effective rinsing, residues can dilute or neutralise the following bath, leave deposits on the component or continue reacting during drying.
Rinse quality matters as much as the active treatment. Water containing excessive dissolved salts can leave marks or deposits as it evaporates, while carry-over from a previous tank can change the chemistry of the next stage. Drainage, component orientation and the design of racks or baskets all affect whether liquids are trapped in joints, folds, hollow sections or recesses. Parts must be able to drain properly so that residual chemicals do not remain beneath the powder film.
Process control determines whether the chemistry is repeatable. Operators normally monitor relevant factors such as bath concentration, pH, temperature, contact time and contamination build-up. The condition of the bath can change as oils, metal salts and other residues accumulate. A process that was suitable when a tank was freshly prepared may produce a different result if its working chemistry is no longer within the specified range. Records, checks and corrective actions help identify whether a problem originates in cleaning, rinsing, surface conditioning, drying or powder application.
After chemical treatment, the component must be dried thoroughly before powder coating. Moisture trapped in seams, threaded holes or enclosed sections can cause defects during curing and may undermine the consistency of the finish. Drying conditions must also suit the substrate and the preceding chemistry; excessive heat or poor drainage can concentrate residues on the surface rather than remove them.
The condition of the prepared metal can be assessed through practical checks. A visual inspection can identify staining, remaining scale, water marks or uneven treatment. A water-break assessment can help reveal areas that are still contaminated, because a properly prepared surface allows water to form a continuous film rather than separating into beads. Where a coating specification requires it, additional adhesion or corrosion-resistance testing can provide evidence that the complete pretreatment and coating system is performing correctly.
Alkaline and acidic stages should therefore be selected as part of one compatible process, not as unrelated products. The correct approach considers the metal grade, existing surface condition, fabrication residues, component geometry, required finish and the powder-coating system that follows. Chemicals should be used in accordance with their technical instructions and safety data, with suitable controls for storage, handling, ventilation, personal protective equipment and treatment of spent solutions. Properly managed, the two chemical stages create predictable conditions for coating; poorly matched or uncontrolled chemistry can introduce defects before the powder reaches the surface.
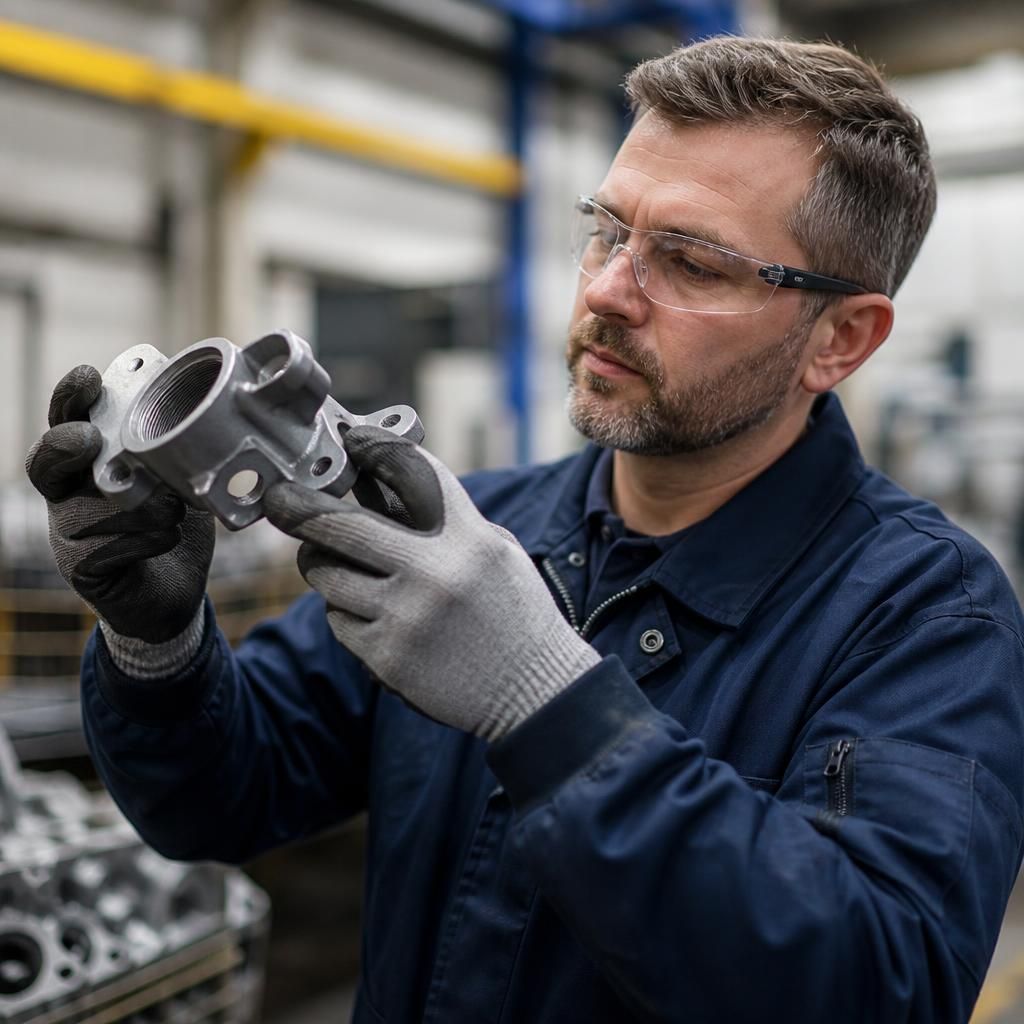
Acidic pretreatment must also be considered where components have close dimensional tolerances. Excessive etching can affect threads, sharp edges, mating faces or finely machined areas, while trapped chemistry in recesses can create localised staining or coating defects. For these parts, the treatment should be qualified against the required surface condition and any areas that must retain precise dimensions should be protected or assessed separately.
This is especially relevant to fabricated assemblies containing different metals, where one chemical stage may affect each substrate at a different rate. Evaluating the complete component rather than treating the metals in isolation helps determine whether the selected alkaline and acidic stages will prepare the surface without causing avoidable dimensional or appearance changes.