

What preparation steps are necessary before commencing a large-scale powder coating project?
Before a large-scale powder coating project begins, confirm the finish specification, inspect the components, and ensure each part is clean, dry and free from oil, rust, scale and other contaminants. Agree masking and hanging requirements, identify drainage and venting points, check that parts can tolerate the curing process, and plan batching, packing and collection or delivery around the production sequence.
Preparation for a large-scale powder coating project means turning the design, component and production requirements into a controlled coating plan before parts enter the process. The key tasks are agreeing technical requirements, confirming production data, validating the substrate and process route, organising quality checks, and removing avoidable handling or sequencing problems.
Define the project requirements
Begin with a complete project brief covering the component description, drawing or part number, material, quantities, required finish, acceptance criteria and intended service environment. The finish specification should identify the colour reference, gloss level, texture and coating type where these affect performance. It should also state which faces are cosmetic, which areas must remain uncoated and whether there are critical dimensions or mating surfaces.
For repeat production, establish which requirements apply to the whole programme and which vary by batch. A controlled revision system is important: the coating team should be able to distinguish current drawings, approved samples and superseded instructions. Any design changes should be assessed before production so that an earlier batch is not compared against a later specification.
Confirm component and material compatibility
Powder coating is applied to electrically conductive components that can withstand the preparation and curing process. Confirm the substrate, alloy, existing treatment, welded areas, cast features and any dissimilar metals. These details can affect pretreatment, adhesion, outgassing and the appearance of the finished film.
Review components for features that may retain moisture, release gases during heating or create difficulty during application. Weld porosity, casting defects, deep recesses and enclosed sections should be identified in advance. Where a design is still being developed, the coating process should be considered alongside fabrication, since small changes to access, joints or drainage can make production more consistent.
Agree a representative approval method
For a large production run, agree how the first acceptable result will be established and how later batches will be compared with it. A representative sample or first-off component can be used to confirm colour, texture, gloss, coverage, edge appearance and the treatment of masked areas before the full quantity is processed.
The approval record should identify the component, finish specification, revision status and any agreed visual limitations. This is particularly useful where the parts have visible welds, sharp transitions, perforations or mixed surface textures. It separates genuine process variation from an appearance that was present in the component before coating.
Plan the production sequence
Large-scale work should be divided into identifiable production lots rather than treated as one undifferentiated quantity. Decide how parts will be grouped by colour, finish, size, material and priority, then establish the order in which they will be processed. The sequence should minimise unnecessary changes while ensuring that urgent or installation-critical parts are clearly identified.
Provide a production schedule that accounts for component availability, drawing approvals, powder and consumable requirements, agreed inspection stages and the planned movement of finished parts. Where several component types form one assembly, retain their relationship through part numbers or batch references so that compatible parts are processed and supplied together.
Prepare technical and quality documentation
A practical project pack may include approved drawings, finish schedules, masking diagrams, hanging or orientation instructions, inspection criteria, batch identification and non-conformance procedures. It should also record any special requirements for coating thickness, visual zones, coverage of edges and treatment of threads or contact points.
Agree how results will be recorded and who can approve a deviation. Quality checks may include visual examination and appropriate coating tests, depending on the specification and the component’s service requirements. The important point is to decide the evidence required before production starts, rather than trying to reconstruct the process history afterwards.
Check powder, colour and consumable control
Confirm that the selected powder is suitable for the substrate, environment and required appearance, and that the material reference matches the approved specification. For a high-volume project, powder should be controlled by product reference, colour, finish and batch where relevant. Mixing similar-looking materials without approval can create visible differences between production lots.
Also identify the ancillary items needed for the run, including masking materials, hooks, contact points, protective separators and labels. These items can influence throughput and finish quality, so they should be available in the correct form before components arrive for processing.
Resolve design and handling risks before production
Review how components will be loaded, moved, inspected and stored at each stage. Large or awkward parts may require a defined orientation or dedicated support to prevent contact damage. Small components may need controlled segregation to avoid mixing part numbers, while finished surfaces may need protection from abrasion during internal handling.
Consider tolerances at assembly interfaces, threaded areas, press fits and sliding surfaces. Powder coating adds a measurable film to the component, so areas with close fits may require an agreed exclusion, allowance or post-coating check. These decisions should be made from the engineering requirement, not improvised after coating has begun.
Use a pre-production review
Before releasing the full run, hold a final review of the current drawings, approved finish, component readiness, process route, quality records, production sequence and handling instructions. Include any lessons from sample or first-off parts and close outstanding technical queries before authorising volume production.
This review gives the coating provider and customer a common reference for the project. It also makes it easier to identify whether a problem originates in the component, the agreed specification, the application process or subsequent handling. For complex programmes, that clarity is as important as the coating material itself.
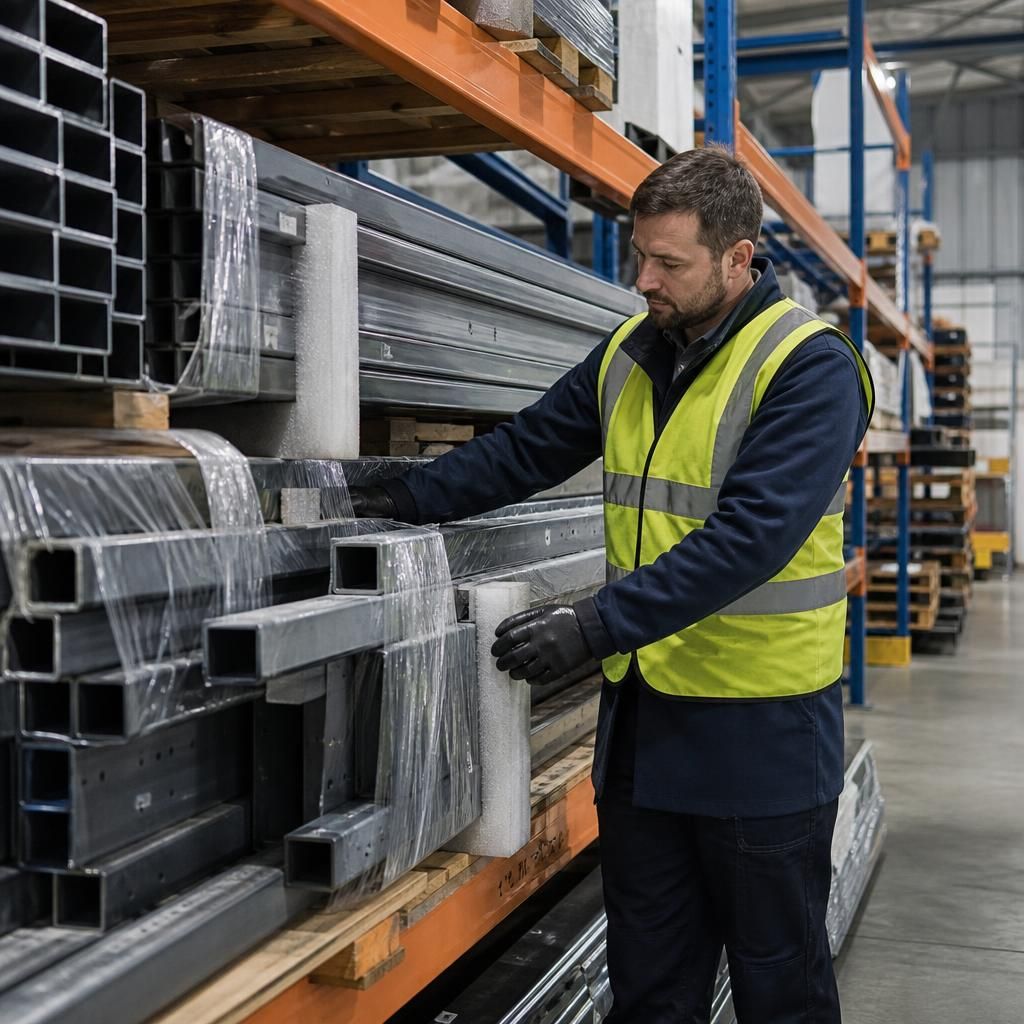
Control the condition of components between fabrication and coating. Parts should be protected from condensation, workshop dust, silicone products, marking residues, cutting fluids and temporary corrosion inhibitors that could interfere with pretreatment or adhesion. Any oil, chemical residue or previous protective treatment should be identified before the coating route is agreed, rather than discovered after processing has started.
Storage and transport arrangements should also prevent new contamination. Use clean supports and suitable separators, avoid placing prepared surfaces directly on dirty pallets or workshop floors, and keep components protected from moisture until they are ready for processing. This preserves the condition established during fabrication and reduces the risk of rework caused by contamination introduced before coating.