

What are the benefits of using zinc phosphate treatment in the powder coating pretreatment process?
Zinc phosphate treatment creates a conversion layer on prepared metal that provides a more receptive surface for powder coating. It improves coating adhesion, helps inhibit corrosion beneath the finish and supports a more durable, consistent coating system.
Zinc phosphate treatment is a chemical conversion pretreatment that modifies the surface of steel before powder is applied. Its main benefits are a controlled, micro-textured substrate, improved resistance to coating breakdown at the metal interface and more predictable performance from the complete coating system. It is particularly useful where components will face moisture, handling, outdoor exposure or demanding industrial service.
Unlike a simple cleaning stage, zinc phosphating creates an insoluble crystalline layer through a controlled chemical reaction with the metal. The resulting surface is not intended to act as a standalone finish. Instead, it forms an intermediate layer between the substrate and the powder coating, helping the pretreatment and coating work as a coordinated system.
- More consistent surface preparation: A correctly controlled phosphate stage gives the powder coating a more uniform base than a surface that has only been degreased and rinsed. This can reduce variation between batches where components have been exposed to different levels of handling, storage contamination or fabrication residue.
- Additional protection at the metal interface: The conversion layer adds a further line of defence beneath the powder film. If the coating is damaged or moisture reaches the substrate, the treated interface can slow the progression of localised coating failure compared with inadequately prepared metal.
- Improved resistance to blistering and under-film deterioration: Moisture, salts and contaminants trapped at the metal/coating boundary can contribute to blistering and loss of finish. Zinc phosphate helps create a more stable interface when the preceding cleaning, rinsing and drying stages have been properly controlled.
- Better suitability for demanding service conditions: The additional pretreatment stage is valuable for components used outdoors, in humid locations or in industrial environments where untreated steel would be more vulnerable to premature breakdown. The required level of treatment should be selected according to the component’s use rather than applied automatically to every job.
- Greater process control: Zinc phosphating can be monitored through bath condition, temperature, contact time, concentration and the appearance or weight of the conversion coating. These controls provide practical checks before powder application and make it easier to identify whether a problem originates in cleaning, phosphating, rinsing, drying or curing.
The treatment is most effective as part of a complete pretreatment sequence. Fabrication oils, grease, mill scale, rust, welding residues and other contamination must first be removed. The component is then rinsed before entering the zinc phosphate stage, followed by suitable rinsing and thorough drying. Any residue left on the surface can interfere with the subsequent coating process, so phosphate treatment cannot compensate for inadequate degreasing or poor rinsing.
Compared with iron phosphate, zinc phosphate generally produces a more substantial crystalline conversion layer and is therefore often selected where the coating system requires a higher level of pretreatment performance. The choice still depends on the substrate, component geometry, exposure conditions, powder specification and production process. Galvanised steel, for example, may require a different treatment approach from mild steel because its surface chemistry differs.
There are also practical limitations. Excessive coating weight, incomplete rinsing, poor bath control or insufficient drying can create residues and surface defects rather than improve the finished result. Complex fabrications need particular attention because joints, recesses and enclosed areas can retain process chemicals or water. The powder must also be applied and cured in accordance with its technical requirements; zinc phosphate is not a substitute for correct powder application or oven control.
In summary, zinc phosphate is beneficial because it provides a controlled conversion layer that strengthens the overall pretreatment system, reduces interface-related failure risks and supports more repeatable powder coating results. Its value depends on matching the chemistry to the metal, maintaining the treatment stages within specification and confirming that the prepared components are clean and dry before coating.
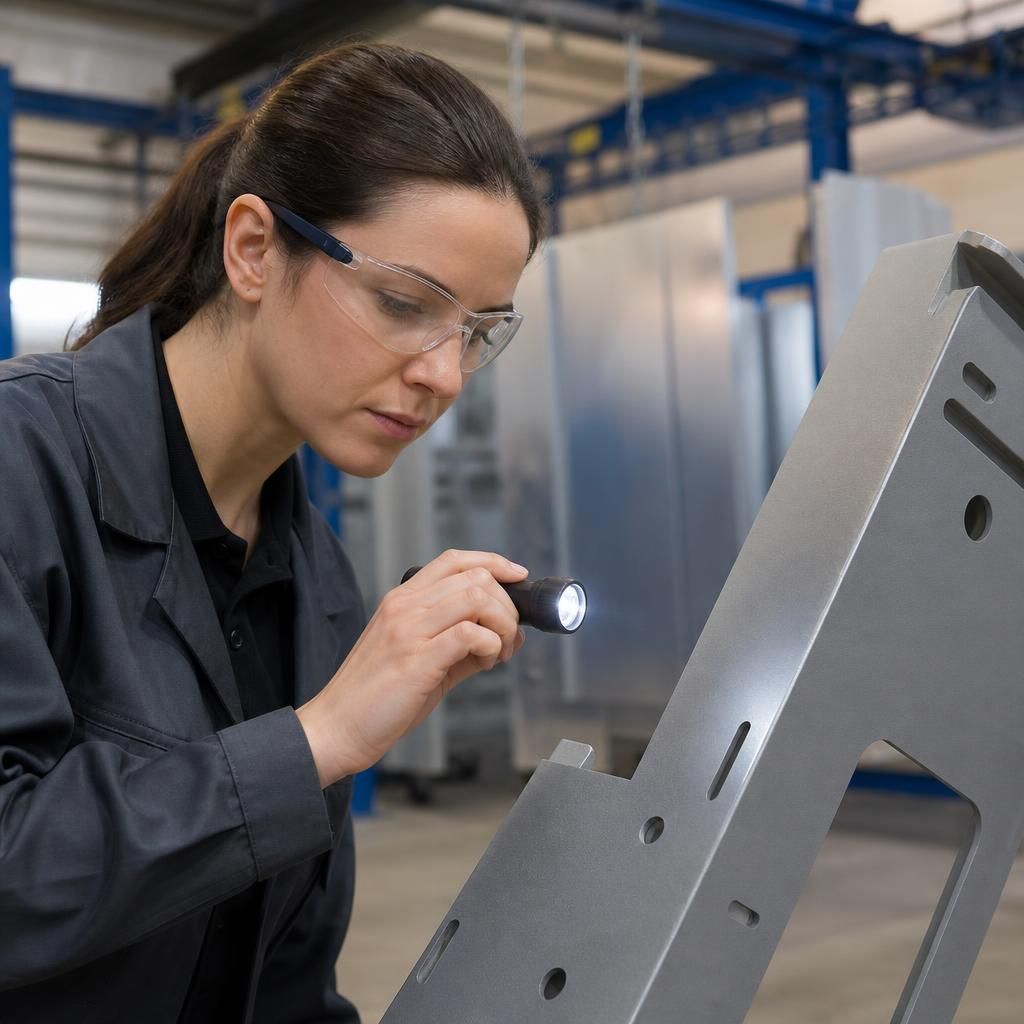
A further benefit of zinc phosphate treatment is that it creates a defined quality checkpoint before powder is applied. The prepared metal can be inspected while the surface remains accessible, rather than relying on the finished coating to reveal whether pretreatment was successful.
Checks at this stage can identify:
- bare or unevenly treated areas;
- powdery or loosely attached phosphate residue;
- water marks caused by ineffective rinsing or drying; and
- contamination left from fabrication or handling.
Correcting these issues before coating helps prevent a pretreatment fault from becoming concealed beneath the powder film. This makes zinc phosphate useful not only as part of the corrosion and adhesion system, but also as a practical inspection stage within industrial coating quality control.
Discuss zinc phosphate pretreatment for your components
Discuss your component material, service environment and coating requirements with a powder coating specialist to establish whether zinc phosphate is the appropriate pretreatment. This helps ensure the preparation sequence is matched to the metal and intended application.