

What key factors ensure the effectiveness of nylon coating in protective applications?
Effective nylon coating depends on thorough surface preparation, correct control of coating thickness and application conditions, and complete curing suited to the metal substrate and nylon system. The coating must also be selected for the intended environment, with adhesion, coverage and finish inspected to confirm consistent protection against wear, moisture and chemicals.
The effectiveness of nylon coating in a protective application is determined by how well the coating system matches the component’s service conditions and how consistently it is applied across the part. In addition to the coating material itself, the design of the component, the required mechanical performance, dimensional tolerances, production controls and inspection criteria all influence the result.
Application conditions should be defined before coating begins. The specification should identify the expected exposure to abrasion, impact, vibration, water, oils, cleaning agents, salts and other chemicals. It should also record operating temperatures and whether the component will be used indoors, outdoors or in a setting where it is subject to repeated thermal or mechanical cycling. Nylon is not a universal solution; a formulation that performs well against physical wear may not be the most suitable choice for continuous chemical exposure or elevated temperatures.
The substrate and component design also affect protective performance. Steel, aluminium and other metals can have different requirements for preparing and coating their surfaces. Welds, sharp corners, recesses, slots and enclosed sections may be more difficult to coat evenly than broad, accessible faces. Radiused edges generally support more uniform coverage than sharp edges, while deep recesses can create areas that need particular attention during application. Drainage and venting provisions may be relevant for hollow fabrications, both to support processing and to prevent trapped residues or moisture affecting the finished part.
Coating thickness must be appropriate to the component’s function. Too little material may leave high-wear areas insufficiently protected, whereas excessive build can interfere with assembly, moving clearances, threaded connections or the operation of closely fitted parts. The required thickness should therefore be specified alongside dimensional tolerances, masking requirements and any areas that must remain free of coating. This is especially important for shafts, bores, mating faces, holes and components assembled with press fits.
The nylon grade should be selected for the dominant form of service stress. Important considerations can include:
- resistance to sliding or repeated abrasion;
- resistance to impact and chipping;
- flexibility where the part may bend or experience vibration;
- resistance to the chemicals, oils or cleaning products encountered in use;
- surface friction and the effect of the finish on movement or handling; and
- colour, texture and appearance where the coating is also used for identification or presentation.
Where several of these demands apply at once, the selection should be based on the most severe credible condition rather than on normal use alone. Occasional exposure to a contaminant, cleaning process or impact event can determine whether a coating remains serviceable.
Component handling and the coating process must preserve coating continuity. Contact points used to support a part can create uncoated areas or marks if they are not planned in advance. Parts should be presented so that all specified surfaces are accessible, while masking protects threads, precision faces, electrical contact points and other areas that must remain clear. Complex batches benefit from an agreed orientation and handling method so that similar components receive comparable treatment.
Inspection should assess more than visual appearance. A sound quality plan can include checks for consistent coverage, visible defects, pinholes, runs, inclusions, damage and correct masking. Depending on the application, it may also be appropriate to verify coating thickness, dimensional clearance and the condition of critical edges or recesses. Inspection criteria should be agreed before production, particularly where the coating forms part of a functional fit or provides protection in a demanding environment.
Small defects should be considered in relation to the part’s role and the coating specification. A minor cosmetic variation may have a different significance from a discontinuity on a sealing face, a bearing surface or an area exposed to concentrated wear. Clear acceptance criteria help distinguish appearance issues from defects that could affect protective performance.
Finally, effectiveness depends on controlling the whole supply chain around the coated part. Clean storage, suitable packaging and careful transport prevent damage after coating. Components should not be stacked or tied in a way that abrades the finish, and contact with incompatible materials or contaminants should be avoided before installation. For repeat production, retaining the coating specification, inspection records and any agreed masking or handling details helps maintain consistency between batches.
For industrial metal components, the most reliable approach is therefore to define the service environment, select nylon for the actual combination of stresses, design the process around the component’s geometry and tolerances, and verify the finished coating against functional requirements. A specialist powder coater can help translate those requirements into a practical specification for individual parts or repeat batches.
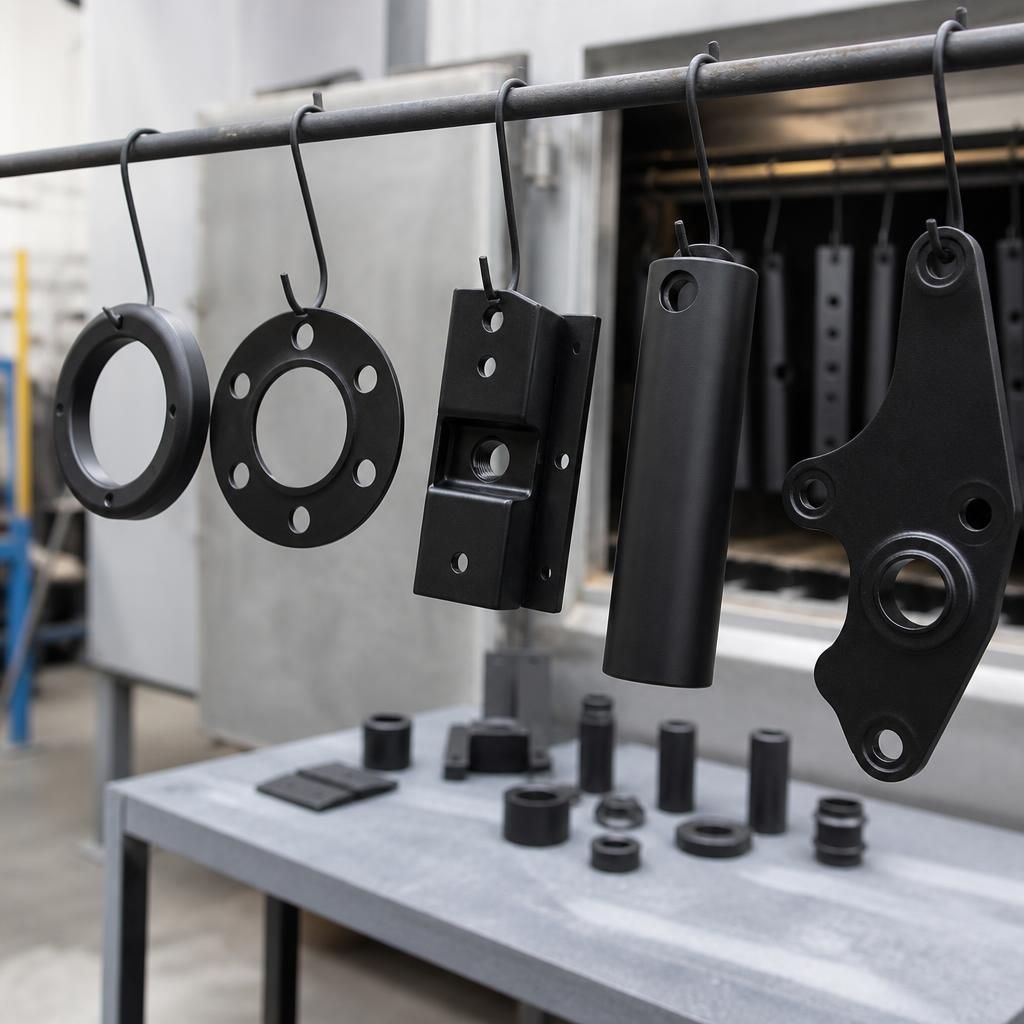
Representative trial pieces can confirm whether a nylon coating system is suitable before a full production batch is processed. The trial should use the same metal, surface condition, component geometry and application method as the finished parts, because results from a simple test panel may not reflect coverage around corners, recesses or contact areas.
Evaluation can include adhesion, coating continuity, thickness, appearance and any functional checks relevant to the component, such as movement through a mating part or resistance to a specified cleaning medium. Reviewing these results against the agreed requirements allows the coating specification, masking arrangement and process settings to be adjusted before production. This validation step is particularly useful where the component is safety-critical, dimensionally sensitive or exposed to a combination of wear and chemical contact.