

What is the best powder coating thickness for galvanised steel?
The best powder coating thickness for galvanised steel is the thickness specified for the chosen coating system and service conditions, rather than a universal figure. It should provide continuous, even coverage while allowing correct curing and adhesion, with the required thickness confirmed through the coating specification and checked during application.
The appropriate powder coating thickness on galvanised steel is determined by the complete coating system, the intended environment and the required corrosion protection. A thicker film is not automatically better: excessive build can impair curing, increase the risk of cracking or poor edge coverage, and create dimensional problems on components that must fit together.
Galvanised steel is already protected by its zinc coating, so powder coating normally forms a supplementary barrier rather than acting as the sole protection against corrosion. The required dry-film thickness should therefore be selected alongside the galvanising condition, the powder chemistry, the specification for the finished component and the severity of exposure. A part used indoors may have different requirements from one exposed to moisture, road contaminants, condensation or industrial pollution.
Several factors should be considered when establishing the specification:
- Service environment: exposure to water, salt, chemicals, abrasion and ultraviolet light affects the level of protection required.
- Powder type: different coating chemistries and product formulations have their own application ranges and curing requirements. The powder manufacturer’s technical data should take precedence over a generic thickness recommendation.
- Component geometry: corners, recesses, holes, welds and folded edges do not receive powder uniformly. The nominal thickness must allow for complete coverage without causing excessive build in areas where powder accumulates.
- Dimensional tolerances: coating build can affect threads, mating faces, hinges, slots and other close-fitting features. These areas may need masking, a controlled coating allowance or a defined exclusion zone.
- Galvanised surface condition: the zinc surface may contain oxides, storage staining, passivation residues or other contaminants. Thickness cannot compensate for inadequate preparation or poor adhesion.
Thickness should be treated as part of a controlled process, not as an isolated target. The galvanised surface needs suitable cleaning and preparation, followed by application and curing in accordance with the powder system’s technical requirements. Particular care is needed where the zinc coating is rough, uneven or visibly affected by previous handling, because local high spots can produce a greater build while recesses remain undercoated.
Measurement is normally based on dry-film thickness after curing. Readings should be taken at representative points across the component rather than relying on a single measurement. Large or complex parts may require checks on broad faces, edges, corners and recessed areas. The results should be assessed against the agreed specification, including any permitted variation, rather than judged solely by appearance.
Undercoating can leave the steel or zinc insufficiently protected and may expose weak areas at edges or defects. Overcoating can be equally problematic: it may obscure detail, interfere with assembly, alter the appearance, or contribute to solvent release, pinholing and other finish defects if the system is not applied correctly. Applying additional powder to hide surface irregularities is therefore not a substitute for proper preparation and process control.
For demanding applications, the specification should identify the required coating system, preparation standard, nominal dry-film thickness, acceptable tolerance, curing conditions and inspection method. It should also state whether different requirements apply to edges, masked areas, contact points or repaired sections. Agreeing these details before production avoids disputes over whether a finish is acceptable after coating.
Where galvanised steel is being coated in batches, sample parts or test panels can help confirm that the selected system is compatible with the substrate and that the proposed thickness cures and adheres correctly. This is particularly useful when the galvanising finish varies between suppliers or when components combine heavy sections with thin sheet and intricate features.
In practice, the best result comes from balancing protection, adhesion, appearance, curing and dimensional control. A coating specialist can review the component design, galvanised finish, exposure conditions and powder manufacturer’s data before confirming the production specification and inspection method.
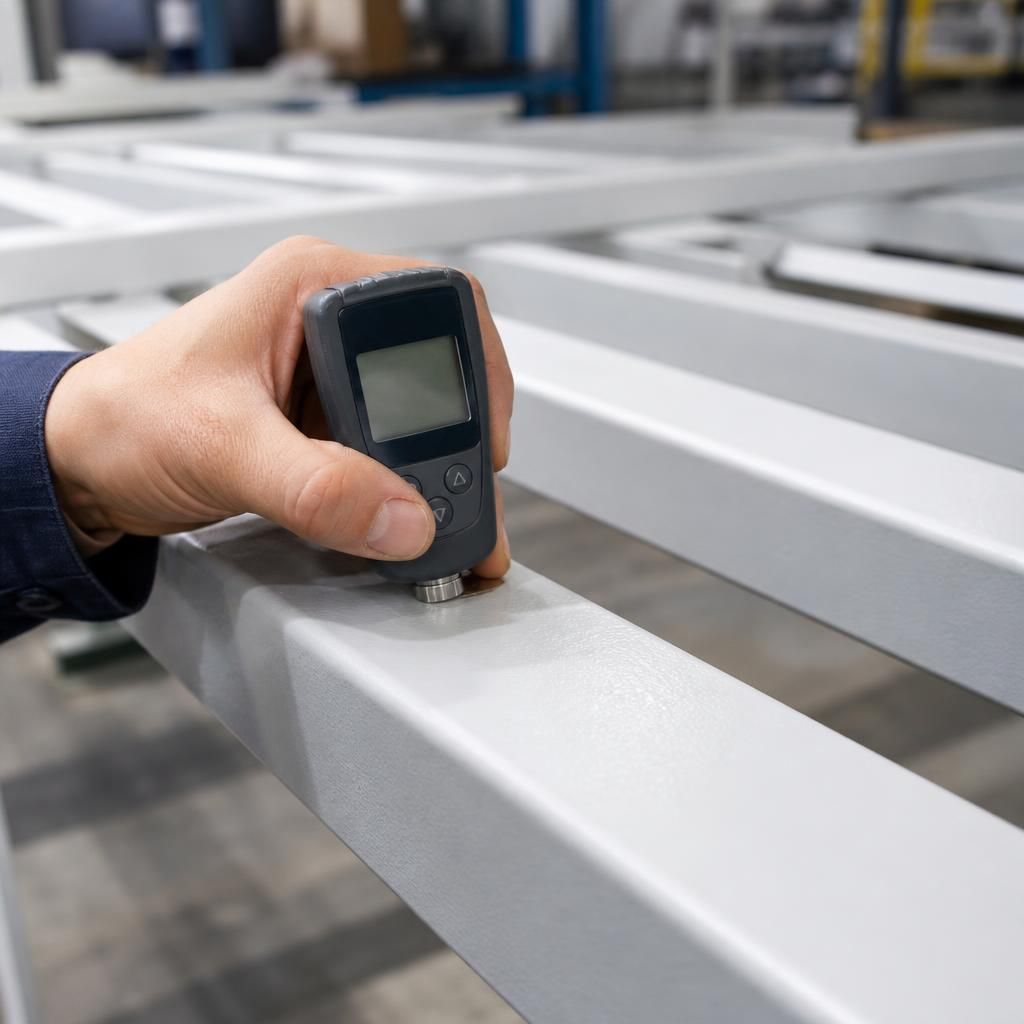
When checking powder coating thickness on galvanised steel, it is important to distinguish the powder layer from the combined thickness of the zinc and powder coatings. A conventional magnetic coating gauge may detect the full non-magnetic coating stack, so its reading may include the galvanising as well as the cured powder.
The inspection specification should therefore state which layer is being assessed and confirm that the chosen measurement method is suitable for a galvanised substrate. Where the powder thickness must be verified separately, pre-coating readings, reference panels or a suitable cross-sectional examination may be needed. This prevents a combined reading from being mistaken for the powder film thickness and gives a more reliable basis for assessing whether the specified coating system has been applied correctly.