

What factors should be considered when comparing the efficacy and longevity of different powder coating resins for specific industrial sectors?
Comparing powder coating resins requires assessing how each chemistry performs under the sector’s actual conditions, including UV exposure, moisture, chemicals, abrasion, temperature and mechanical impact. Longevity also depends on substrate preparation, coating thickness, curing control, service environment and the required finish, so polyester, epoxy, hybrid, polyurethane or nylon systems should be selected against the component’s use rather than judged in isolation.
The most reliable comparison is based on the resin’s performance against the component’s specification, not on resin type alone. Efficacy means how well the coating delivers the required properties at the point of use, while longevity means how long those properties and the appearance remain acceptable. A sound assessment therefore combines resin chemistry with the substrate, component design, exposure classification, production method, maintenance expectations and any relevant sector requirements.
Start by defining what “performance” means for the component. A coating may be judged primarily on corrosion resistance, but other requirements can be equally important. These may include:
- adhesion to the prepared substrate and resistance to delamination;
- flexibility where parts are formed, assembled or subject to movement;
- resistance to scratching, chipping and repeated handling;
- retention of colour, gloss and surface uniformity where appearance is specified;
- resistance to oils, cleaning agents, fuels, solvents or process chemicals;
- electrical insulation or controlled conductivity where the finished part forms part of an electrical assembly;
- low-friction or wear-resistant behaviour for moving or contacting components; and
- compatibility with subsequent assembly, sealing, bonding, machining or installation.
This prevents a coating from being selected because it performs well in one test while failing an important requirement in service. For example, a finish with good hardness may still be unsuitable if the component needs to flex during installation, and a visually durable finish may not withstand repeated contact with a particular cleaning chemical.
Compare the resin families by their typical operating strengths and limitations. Epoxy-based systems commonly provide strong adhesion and useful resistance to corrosion and many chemicals, making them relevant to interior components, fabricated assemblies and parts where weathering is limited. Their suitability should be questioned where prolonged direct sunlight is expected, because exterior appearance and surface performance may deteriorate even if the underlying film remains attached.
Polyester systems are often considered for external metalwork because exterior-grade formulations can provide better resistance to weathering and colour change than many interior-focused alternatives. However, polyester is not one uniform category: the formulation, stated exposure class, colour, gloss level and film build all affect the result. Hybrid epoxy-polyester systems can offer a practical balance for many indoor applications, but should not automatically be treated as equivalent to an exterior-grade polyester.
Polyurethane systems may be selected where a particular combination of appearance, smoothness, hardness and weathering performance is required. Nylon coatings are relevant where a thicker, tough and wear-resistant layer is needed, including components exposed to repeated contact or abrasion. Their application requirements and dimensional effect need careful consideration, particularly on small parts, close tolerances, threaded areas and assemblies containing moving interfaces.
Assess the service environment in more detail than simply labelling it “indoor” or “outdoor”. Two parts used outside can experience very different conditions. A sheltered architectural component, a roadside fitting and an agricultural machine may all be exposed outdoors, but differ in sunlight, standing water, salt contamination, dirt accumulation, condensation and cleaning frequency. Indoor conditions also vary: a dry factory, a washdown area, a chemical-processing space and a heated building should not be treated as the same environment.
Consider the complete exposure cycle rather than one isolated hazard. Repeated wetting and drying, condensation beneath deposits, contact between dissimilar metals, trapped moisture in joints and contamination around edges can influence service life. The resin should be reviewed alongside the component’s drainage, joint design, weld quality and access for cleaning. Powder coating can protect an appropriate substrate effectively, but it cannot correct poor component design or eliminate an exposure route that allows corrosion to begin beneath or behind the coating.
Use the substrate and part geometry as selection criteria. Steel, galvanised steel, aluminium and previously coated components present different adhesion and pretreatment challenges. Sharp corners, recesses, holes, folded returns and welded areas can produce local differences in coverage and curing. Complex geometry may also affect how consistently the powder deposits, particularly where electrostatic shielding occurs.
Edges deserve particular attention because the coating can be thinner there than on broad faces. A resin that performs well on a flat test panel may not provide the same protection on a fabricated assembly with exposed edges, crevices or weld spatter. The comparison should therefore include representative components or test panels that reproduce the actual substrate, geometry and preparation method, rather than relying only on a supplier’s generic data sheet.
Separate laboratory durability from predicted field life. Salt-spray, humidity, chemical-immersion, abrasion, impact, adhesion, gloss-retention and accelerated-weathering tests can help compare products, but each measures a defined property under controlled conditions. A longer result in one test does not automatically establish a longer service life in every industrial environment. Test duration, panel preparation, film condition, scribe method, failure definition and pass criteria must be comparable before results are used to rank resins.
For a meaningful comparison, specify the acceptance criteria in advance. These might cover maximum loss of adhesion, allowable corrosion creep from a scribe, acceptable gloss or colour change, resistance to a named cleaning chemical, or the number of handling cycles a component must tolerate. If no measurable criterion is set, terms such as “heavy duty” or “high performance” are difficult to use consistently.
Review curing behaviour and production tolerances. A resin’s stated performance assumes that it has reached the required cure throughout the film. The relevant condition is the metal temperature and time at that temperature, not simply the oven’s displayed air temperature or the time a component spends inside the oven. Part mass, thickness, loading pattern and oven airflow can cause different areas of one batch to receive different thermal exposure.
Some resin systems are more tolerant of variation than others, but none should be assessed independently of the production process. Under-cure can reduce mechanical and chemical performance, while excessive heat can affect colour, gloss or the substrate. A proper comparison should consider the available application equipment, part size, line control, rework procedure and the practical curing window for the chosen formulation.
Take whole-life requirements into account. A resin with a lower initial material cost may be less suitable if it requires frequent recoating, specialist cleaning or early replacement. Conversely, selecting the most demanding specification for every part may add cost and process complexity without improving useful life. Consider inspection access, likely damage, repairability, colour availability, spare-part matching and whether the component can be removed for future recoating.
For manufacturers and fabricators, the best comparison normally results in a written coating specification. It should identify the substrate, preparation standard, resin family or approved formulation, colour and finish, target film requirement, curing schedule, testing method, acceptance criteria and conditions of use. Where the application is unusual, sample panels or representative trial parts can expose problems with adhesion, appearance, masking, assembly clearance or cure before full production begins.
Industrial powder coating work is most effectively assessed on this evidence-led basis. A specialist coating provider can help interpret the component’s use, check whether the selected system is compatible with the part and advise on practical application constraints, while the end user remains responsible for defining the service conditions and required performance. This approach gives efficacy and longevity a measurable meaning and reduces the risk of choosing a resin solely by reputation or headline test result.
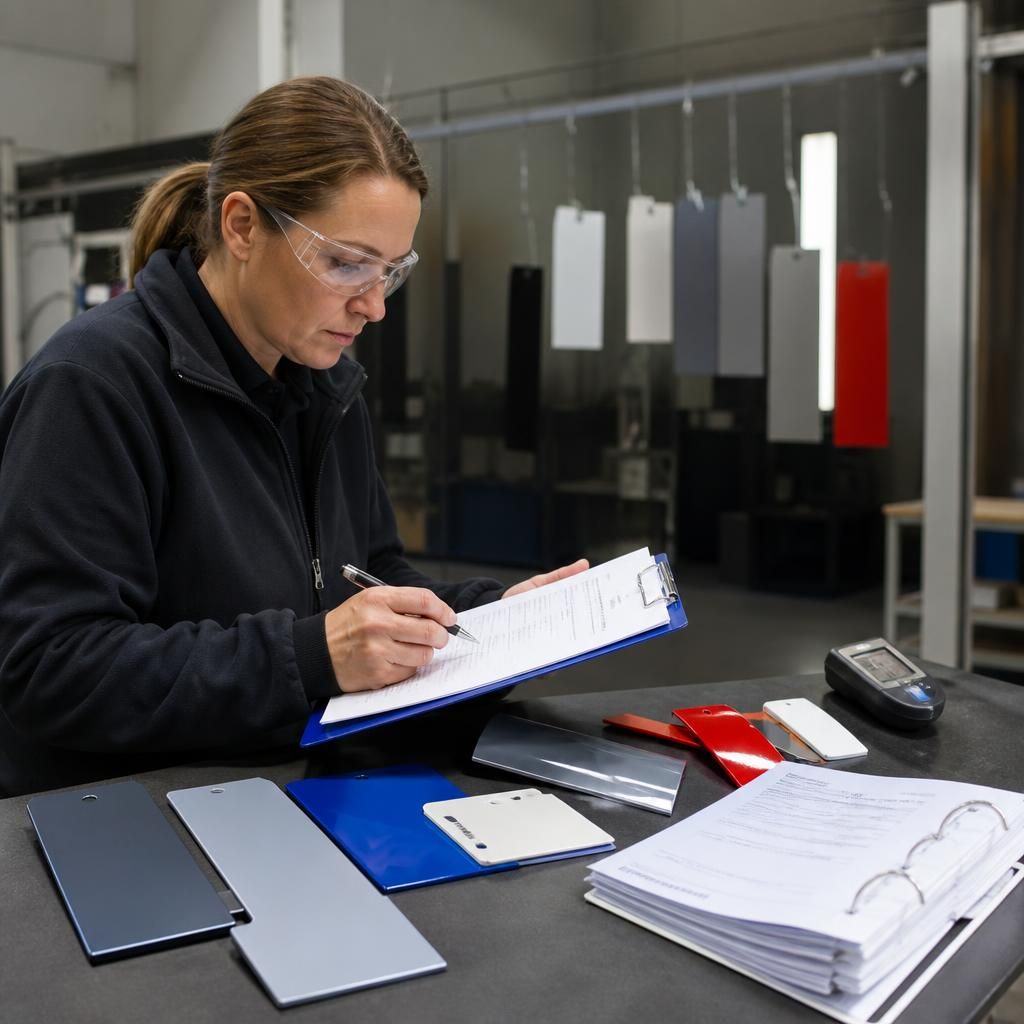
Comparing powder coating resins for a specific industrial sector also requires checking the quality and relevance of the supporting documentation. A resin should not be selected solely because a technical data sheet describes it as durable; the evidence should relate to the component’s intended use and the specification that the finished product must meet.
- Check whether the formulation has the required sector, project or customer approval, where one applies.
- Confirm that technical data covers the properties important to the application, such as weathering, chemical resistance, abrasion or appearance retention.
- Review restrictions on substances, cleaning methods and contact with adjoining materials before approval.
- Require clear identification of the approved formulation, colour, finish and application conditions so that later batches can be compared consistently.
- Consider whether the supplier provides suitable safety, handling and repair information for the people who will apply, assemble or maintain the coated part.
This evidence is particularly important when components enter a controlled supply chain. Manufacturers and fabricators may need to demonstrate that the selected resin remains consistent between production batches and that any change in formulation is identified before it affects fit, appearance or service performance. Documentation therefore forms part of the efficacy and longevity assessment: it helps establish what has been specified, what has been tested and whether the coating remains appropriate for the sector throughout the product’s life.